Lasersec Technologies

Anti-counterfeit packaging for refillable FMCG products

Sustainability is becoming a major priority for FMCG brands worldwide.

Many companies are redesigning packaging systems to reduce plastic waste, minimize environmental impact, and encourage circular consumption models.

One of the most widely adopted approaches is refillable packaging.

Consumers purchase a durable container once and then refill it with product pouches, sachets, or refill packs. This model significantly reduces packaging waste and supports long-term sustainability goals.

However, while refillable packaging improves environmental performance, it also introduces new security challenges.

Refill packs and reusable containers can become targets for counterfeit products if authentication mechanisms are not integrated into the packaging system.

For FMCG brands focused on sustainability innovation, ensuring both environmental responsibility and product authenticity is becoming increasingly important.

The Rise of Refillable Packaging in the FMCG Industry

Refillable packaging systems are becoming increasingly common across FMCG categories such as:

  • Personal care products
  • Household cleaning products
  • Liquid detergents
  • Beauty and skincare products
  • Food and beverage concentrates

In these systems, consumers typically purchase a primary container that is designed for repeated use.

Refill packs allow the consumer to replenish the product without discarding the main container.

This model offers several sustainability benefits:

  • Reduced plastic consumption
  • Lower packaging waste
  • Reduced transportation impact due to lighter refill packs
  • Improved lifecycle efficiency for packaging materials
While these advantages are significant, refillable systems also create new vulnerabilities for product authenticity.

The Counterfeit Risk in Refillable FMCG Products

In refill-based systems, the original container often remains in use for a long period of time.

Consumers rely on refill packs to maintain product quality and performance.

However, counterfeiters may attempt to exploit this system by introducing fake refill packs or unauthorized refilling practices.

Some common risks include:

  • Counterfeit refill pouches imitating branded refill packs
  • Unauthorized refill stations offering diluted or fake products
  • Reused containers filled with non-genuine formulations
  • Repackaged counterfeit products sold as genuine refills

Because consumers already possess the original container, they may assume that any refill product associated with that brand is authentic.

Without authentication features, distinguishing genuine refills from counterfeit ones becomes extremely difficult.

Why Traditional Packaging Security May Not Work for Refill Systems

Traditional anti-counterfeit strategies often focus on protecting the primary product packaging.

However, refill systems change the structure of product distribution.

Instead of purchasing a completely new packaged product each time, consumers rely on secondary refill formats.

These refill packs are often:

  • Smaller
  • Flexible pouches or sachets
  • Lightweight packaging formats

Because refill packs are designed to reduce material usage, they may contain fewer physical security elements.

This creates opportunities for counterfeiters to replicate packaging designs more easily.

For FMCG brands investing in sustainability-driven packaging systems, security must evolve alongside sustainability initiatives.

The Authentication Challenges of Reusable Containers

Reusable containers present another layer of complexity for product authentication.

Since the primary container may remain in use for months or even years, the container itself does not necessarily verify the authenticity of the product inside.

A consumer may refill the container multiple times, but there is no guarantee that the refill used is genuine.

Without proper authentication mechanisms, several issues can arise:

  • Consumers unknowingly using counterfeit refills
  • Diluted or substandard products affecting performance
  • Negative brand experiences caused by fake formulations
  • Difficulty tracing product origin
In such scenarios, the brand may still be blamed even though the counterfeit refill was not produced by the manufacturer.

Integrating Authentication into Refill Packaging

To address these risks, FMCG brands are increasingly integrating authentication technologies directly into refill packaging systems.

These technologies help verify product authenticity while maintaining the sustainability advantages of refill models.

Common authentication solutions include:

These features allow consumers, retailers, and manufacturers to confirm that the refill product originates from an authorized source.

How QR-Based Authentication Supports Refillable Packaging

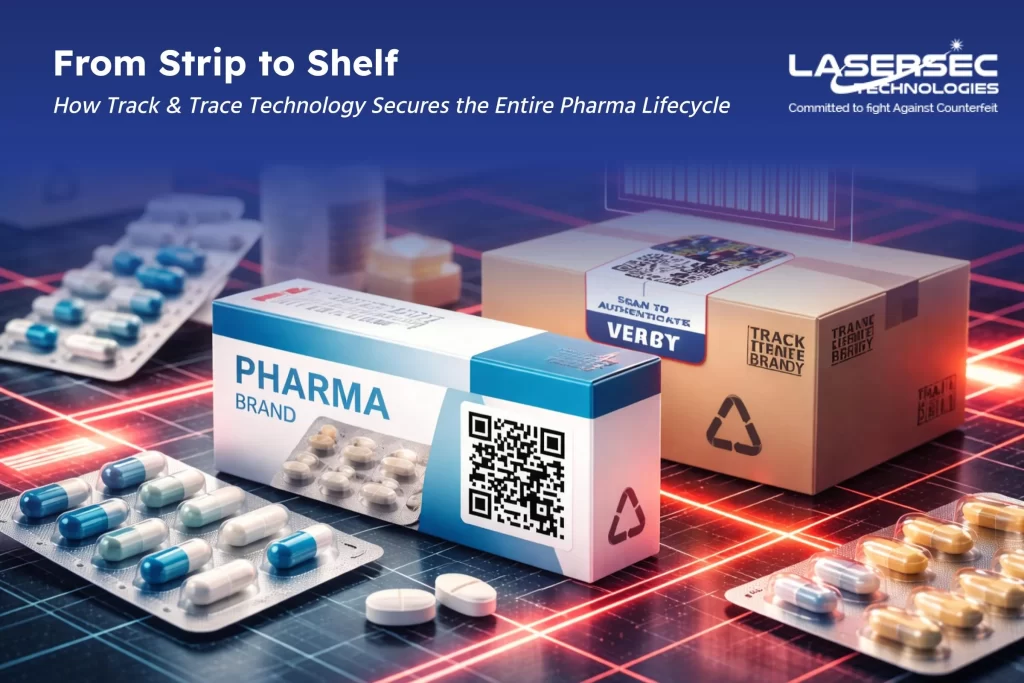
QR code authentication is particularly well suited for refill packaging because it requires minimal packaging material while enabling powerful verification capabilities.

Each refill pack can carry a unique scannable QR code linked to a secure authentication system.
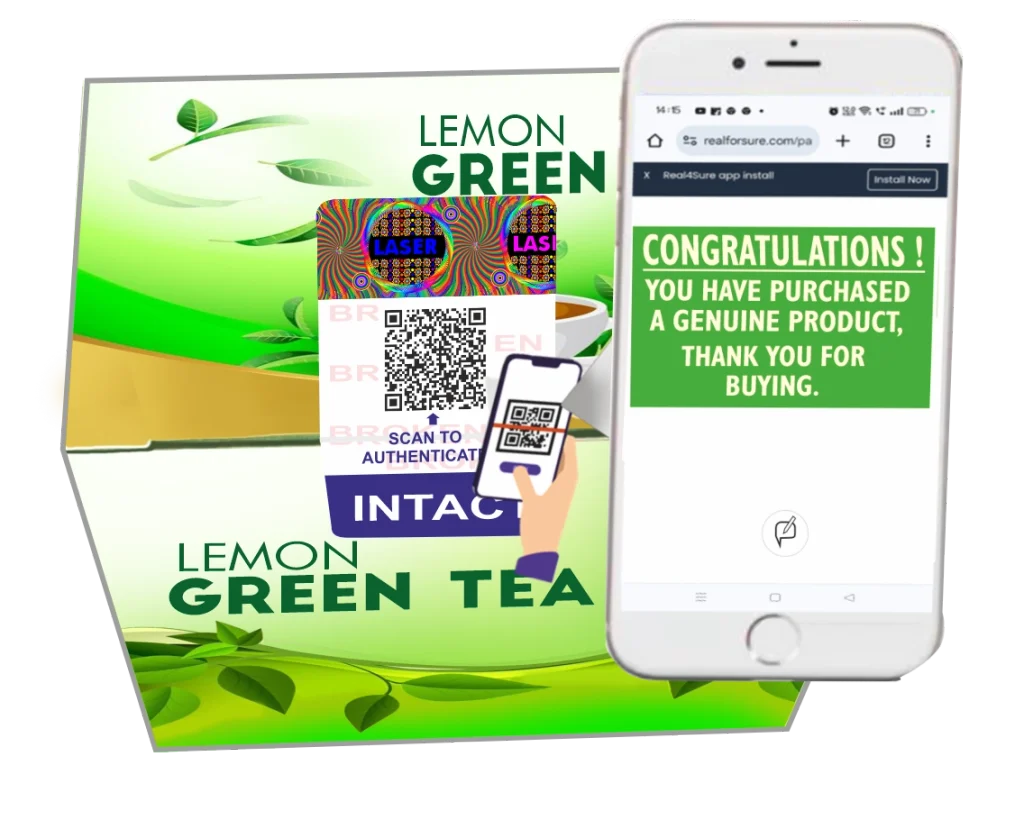
When scanned, the system can verify:

  • Whether the refill product is genuine
  • Manufacturing origin and batch details
  • Product authenticity status
  • Brand verification information

This creates a simple verification process that consumers can perform using their smartphones.

If duplicate scans or suspicious activity occurs, the system can flag potential counterfeit distribution.

Supporting Transparency in Sustainable FMCG Supply Chains

Consumers who choose refillable products are often highly conscious about sustainability and brand ethics.

These consumers value transparency regarding product origin, formulation quality, and environmental impact.

Authentication technologies allow brands to provide this transparency through digital engagement.

When consumers scan refill packaging, brands can share information such as:

  • Product authenticity confirmation
  • Sustainability commitments
  • Responsible sourcing practices
  • Product usage guidance
This interaction strengthens consumer trust while reinforcing the brand’s sustainability messaging.

Why Sustainability and Security Must Work Together

Sustainability innovations should not compromise product security.

If refill systems are vulnerable to counterfeit infiltration, the consequences can include:

  • Consumer safety concerns
  • Product performance failures
  • Damage to brand credibility
  • Loss of consumer trust in refill systems

Therefore, packaging innovators and sustainability leaders must design refillable packaging systems that balance environmental responsibility with authentication security.

Integrating anti-counterfeit technologies ensures that refillable models remain safe, reliable, and trustworthy.

How Lasersec Technologies Supports Secure Refillable Packaging

At Lasersec Technologies, we help FMCG brands integrate authentication and anti-counterfeit protection into modern packaging systems.

Our solutions combine secure holographic labels, QR-based authentication, tamper-evident packaging features, and Track & Trace systems to protect products across evolving packaging formats.

These technologies help FMCG brands:

  • Prevent counterfeit refill products
  • Protect reusable container ecosystems
  • Enable consumer-level product authentication
  • Strengthen supply chain visibility
  • Support sustainable packaging strategies without compromising security

By integrating smart authentication technologies into refill packaging, brands can maintain both environmental responsibility and product integrity.
Share :

Frequently Asked Questions

Refillable packaging systems can be vulnerable to fake refill packs, unauthorized refilling, and reused containers filled with counterfeit products. Anti-counterfeit technologies help brands verify product authenticity, protect consumers, and maintain trust in sustainable packaging initiatives. Learn how tamper-proof seals in FMCG build consumer trust and prevent refilling or product substitution and explore our full range of FMCG Industry Anti-Counterfeit Solutions for refill packaging security.

Unique QR codes allow consumers, retailers, and manufacturers to verify whether a refill pack is genuine using a smartphone. The technology can also provide access to product information, batch details, and authentication records while helping brands detect suspicious or duplicate scans. Explore how QR-based authentication strengthens brand protection and discover our Anti-Counterfeit Labels with QR Code designed specifically to strengthen refill pack verification across FMCG supply chains.

Yes. Sustainability and security are complementary when designed together. Refillable packaging can incorporate authentication technologies such as tamper-evident seals, security holograms, serialized identifiers, and Track & Trace systems without undermining environmental goals. See how tamper-evident packaging and Track & Trace work together to deliver layered protection, and learn how building instant consumer trust with QR codes helps FMCG brands reduce waste while protecting against counterfeit products.

For FMCG brands, anti-counterfeit measures can protect brand reputation, improve consumer confidence, reduce the circulation of fake refill products, and support long-term sustainability initiatives. Discover how anti-counterfeiting solutions are critical for emerging FMCG markets and explore how our Tamper-Proof Hologram Stickers combined with QR Code Authentication and Track & Trace Technology create a layered approach to safeguarding refill ecosystems.

An effective refill packaging solution should combine authentication, tamper evidence, and supply chain visibility while remaining compatible with sustainability objectives. Features such as unique QR codes, holographic security elements, serialized identifiers, and Track & Trace capabilities help ensure refill products remain genuine from production to purchase. Explore our FMCG Industry Anti-Counterfeit Solutions and Anti-Counterfeit Labels with QR Code, and learn how combating food adulteration with anti-counterfeit solutions helps build a secure and sustainable packaging strategy.

Related Blogs

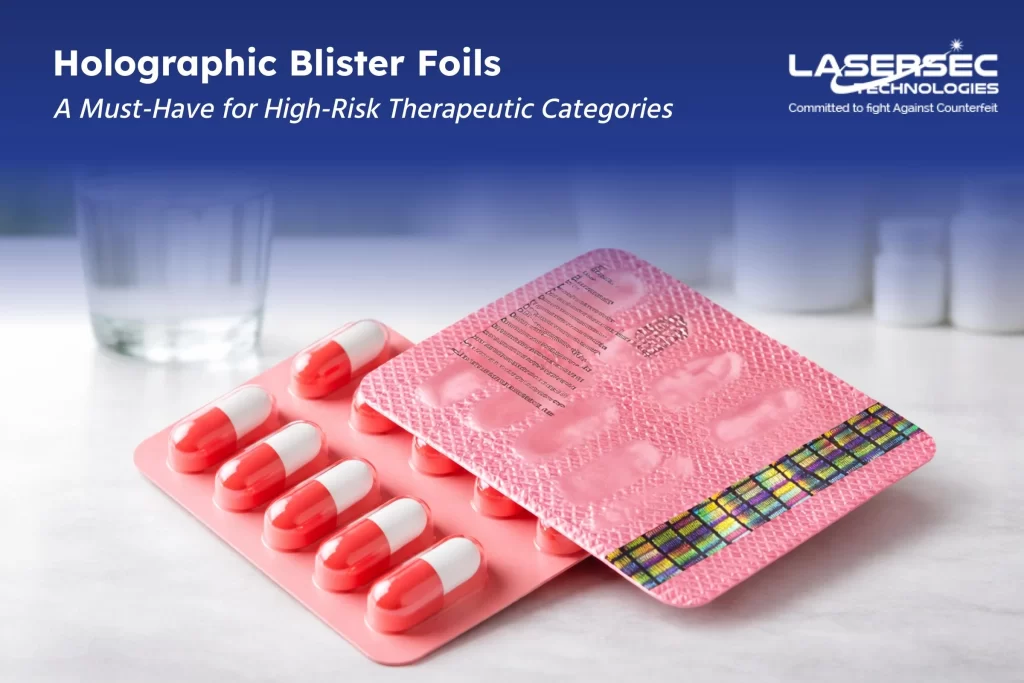
Holographic blister foil for high-risk pharmaceutical drugs

A pharmaceutical product moves through years of research, regulatory approvals, clinical validation, and strict manufacturing protocols before it reaches patients.

For critical therapeutic categories such as oncology medicines, anti-infectives, and psychotropic drugs, the stakes are even higher. These medicines are often life-saving, tightly regulated, and distributed through controlled supply chains.

Yet despite these safeguards, counterfeit drugs continue to infiltrate global pharmaceutical markets.

In many cases, counterfeit products replicate packaging so closely that visual inspection alone cannot identify the difference. A blister pack may appear genuine while the tablets inside are ineffective, contaminated, or entirely fake.

For manufacturers of high-risk medicines, this creates a serious challenge. Traditional packaging is no longer sufficient to protect products against sophisticated counterfeiting operations.

This is why holographic blister foils have emerged as a critical pharmaceutical packaging security solution. By integrating advanced holographic security directly into blister packaging, manufacturers can significantly strengthen product authentication, supply chain integrity, and patient safety.

Why High-Risk Therapeutic Categories Are Prime Targets for Counterfeit Drugs

Counterfeit pharmaceutical products do not affect all drug categories equally. Certain therapeutic segments are more vulnerable due to their high value, global demand, and critical medical importance.

These include:

  • Oncology drugs
  • Anti-infective medications such as antibiotics and antivirals
  • Psychotropic and controlled substances
  • Specialty and high-value prescription medicines

Counterfeiters often target these medicines because they command higher prices and move through complex international supply chains.

In some cases, counterfeiters attempt to replicate genuine packaging using advanced printing techniques. Without strong security features integrated into packaging, distinguishing genuine products from counterfeits becomes extremely difficult.

The consequences can be severe:

  • Patients receiving ineffective or dangerous treatments
  • Regulatory violations and recalls
  • Loss of trust among healthcare providers
  • Significant financial and reputational damage for pharmaceutical companies
For high-risk therapeutic categories, packaging security becomes an essential part of patient protection and regulatory compliance.

The Limitations of Standard Blister Packaging in Preventing Counterfeits

Blister packaging has long been a preferred format for pharmaceutical products due to its ability to protect tablets from moisture, contamination, and tampering.

However, standard blister foils without advanced security features primarily serve a protective function, not a security function.

Traditional blister packaging elements such as:

  • Printed foil designs
  • Batch numbers
  • Standard barcodes
  • Basic branding elements

can be replicated with increasing accuracy using modern printing technologies.

This allows counterfeiters to produce visually convincing packaging that can enter distribution channels unnoticed.

Even trained distributors or pharmacists may struggle to identify counterfeit products if packaging lacks secure authentication features.

As counterfeit methods become more sophisticated, pharmaceutical manufacturers require packaging solutions that provide visible, verifiable, and difficult-to-replicate security layers such as pharma holographic labels.

What Makes Holographic Blister Foils a Powerful Anti-Counterfeiting Solution

Holographic blister foils incorporate advanced optical security elements directly into pharmaceutical packaging materials.

These holographic effects are created using specialized technologies that produce complex light diffraction patterns which are extremely difficult to replicate using conventional printing methods.

Unlike standard foil designs, holographic blister foils include multi-layered security structures that provide both visual authentication and tamper resistance.

Key characteristics include:

  • Complex holographic patterns that cannot be easily duplicated
  • Dynamic visual effects visible under light movement
  • Integration with security printing technologies such as security holograms
  • Compatibility with serialized QR codes or authentication systems like QR code authentication labels
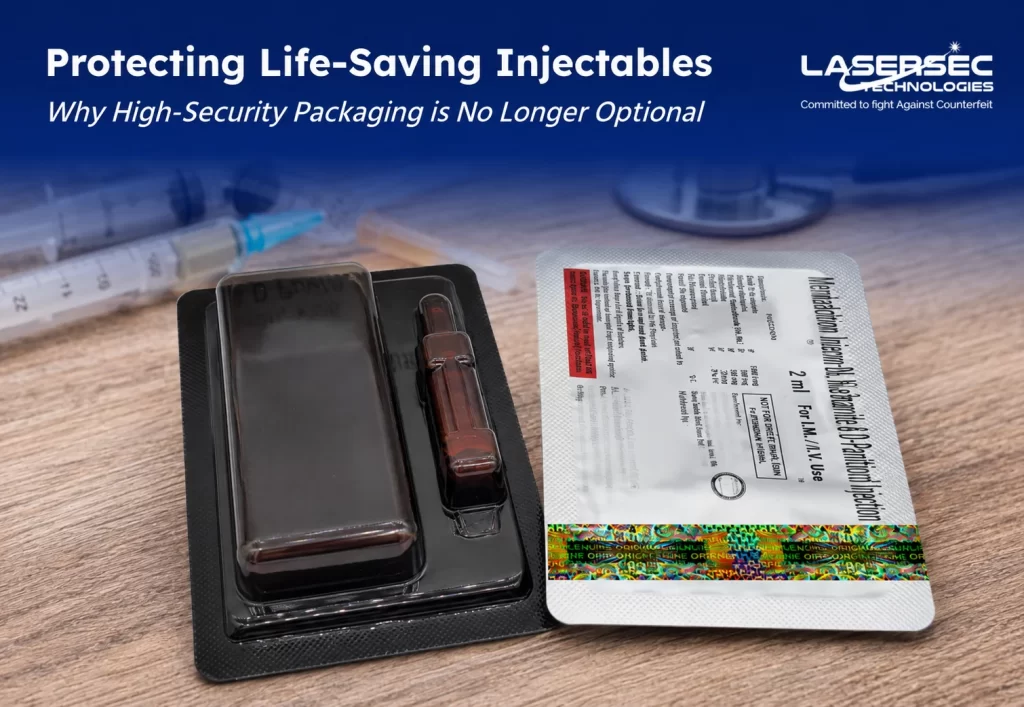
  • Secure bonding to blister packaging that reveals tampering

These features transform blister packaging from a passive protective layer into an active anti-counterfeit security system.

Healthcare professionals, distributors, and regulators can visually confirm authenticity while manufacturers benefit from stronger packaging protection.

Protecting Oncology Medicines with Secure Holographic Blister Foils

Oncology drugs represent one of the most critical and valuable pharmaceutical segments globally.

These medicines are often expensive, lifesaving, and distributed across multiple international markets. Their high value makes them frequent targets for counterfeiting networks.

Counterfeit oncology drugs can have devastating consequences because patients rely on these treatments during life-threatening conditions.

Holographic blister foils help protect oncology medicines by providing:

  • A highly visible authentication feature on each blister pack
  • Packaging elements that are extremely difficult for counterfeiters to reproduce
  • Tamper-evident indicators that reveal unauthorized access using tamper-evident holographic labels
  • Compatibility with serialization and track-and-trace systems
This ensures that genuine medicines reach hospitals, pharmacies, and patients without interference from counterfeit supply chains.

Securing Anti-Infective Drugs Against Counterfeit Distribution

Anti-infective medications such as antibiotics and antivirals are widely used across healthcare systems and are frequently distributed across international markets.

Because of their global demand, these medicines are particularly vulnerable to counterfeit manufacturing and unauthorized resale.

The distribution of counterfeit anti-infective drugs contributes to serious public health risks, including ineffective treatment and antimicrobial resistance.

Holographic blister foils add a powerful security layer by making packaging authentication easier at multiple points in the supply chain.

Distributors, pharmacists, and regulatory authorities can visually confirm that the blister packaging includes genuine security features before the product reaches patients.

Enhancing Security for Psychotropic and Controlled Substances

Psychotropic medications and controlled drugs are among the most tightly regulated pharmaceutical categories.

These medicines require strict monitoring to prevent misuse, diversion, or illegal distribution.

However, counterfeit versions of these products continue to appear in illegal markets.

Holographic blister foils help pharmaceutical manufacturers strengthen packaging security by ensuring that:

  • Genuine products include identifiable holographic authentication elements
  • Counterfeit copies are easier to detect
  • Tampering or repackaging attempts become visible
By integrating security features directly into blister packaging materials, manufacturers create a stronger defense against both counterfeiting and product diversion.

Combining Holographic Blister Foils with Track & Trace Authentication

While holographic security provides strong visual protection, combining it with digital verification systems creates an even more powerful anti-counterfeit framework.

Modern pharmaceutical brand protection strategies often combine secure packaging technologies with Track & Trace systems.

When holographic blister foils are integrated with serialized QR codes or authentication identifiers, manufacturers gain the ability to:

  • Verify product authenticity instantly
  • Track product movement across supply chains
  • Detect duplicate or suspicious codes
  • Identify unauthorized market diversion
This hybrid approach creates both physical security and digital traceability, significantly improving pharmaceutical supply chain protection.

Why High-Risk Pharmaceutical Manufacturers Are Adopting Holographic Blister Foils

Pharmaceutical companies manufacturing high-risk medicines are increasingly prioritizing packaging security as part of their broader brand protection and compliance strategies.

Holographic blister foils offer several important advantages:

  • Strong visual authentication that is difficult to replicate
  • Integration with serialization and Track & Trace technologies
  • Tamper-evident packaging protection
  • Enhanced regulatory confidence
  • Improved distributor and patient trust
These benefits make holographic blister foils an effective packaging security solution for manufacturers producing high-value or life-critical medicines.

How Lasersec Technologies Supports Secure Pharmaceutical Packaging

At Lasersec Technologies, we specialize in advanced pharmaceutical anti-counterfeit packaging solutions designed to protect high-risk medicines across global markets.

Our holographic blister foil solutions integrate complex holographic security with high-quality pharmaceutical packaging materials, enabling manufacturers to strengthen packaging authentication without disrupting production processes.

These solutions are part of our broader pharmaceutical industry solutions and help companies:

  • Prevent counterfeit drug infiltration
  • Protect high-risk therapeutic categories
  • Strengthen supply chain security
  • Improve packaging authentication
  • Support regulatory compliance
By combining advanced holographic technologies with secure packaging design, we help pharmaceutical brands safeguard both their products and their patients.

Taking Pharmaceutical Packaging Security Forward

As counterfeiting methods grow more sophisticated, the need for advanced packaging security is no longer optional — it is a critical requirement for manufacturers of high-risk medicines. Holographic blister foils represent a proven, scalable, and highly effective solution that addresses both the physical and digital dimensions of product authentication.

At Lasersec Technologies, we remain committed to continuous innovation in anti-counterfeit pharmaceutical packaging, helping manufacturers stay ahead of emerging threats while maintaining full regulatory compliance.

Meet Us at CPhI InnoPack Pharma Confex 2026

We are excited to share that Lasersec Technologies will be participating as an Exhibit Partner at the 15th Annual CPhI InnoPack Pharma Confex — one of India’s most significant platforms for pharmaceutical packaging innovation and industry collaboration.

If you are exploring how holographic blister foils or advanced anti-counterfeit packaging solutions can strengthen your product security, this is an excellent opportunity to connect with our team directly and see our latest technologies up close.

Visit us at Booth No. F1 on 18–19 June 2026 at Sahara Star, Mumbai, and let us help you find the right packaging security solution for your therapeutic category.

Tamper-evident packaging and secure seals protecting pharmaceutical and consumer products for brand protection

Across many industries today, product safety and authenticity have become critical priorities for regulators, manufacturers, and consumers.

From pharmaceuticals and food products to cosmetics and electronics, companies are expected to ensure that their products reach customers without interference or tampering. However, global supply chains often involve multiple distributors, logistics providers, and retailers before a product reaches the end user.

This complexity creates opportunities for product tampering, repackaging, and counterfeit substitution.

To address these risks, regulators around the world increasingly require tamper-evident or tamper-proof packaging systems that clearly indicate whether a product has been opened or altered.

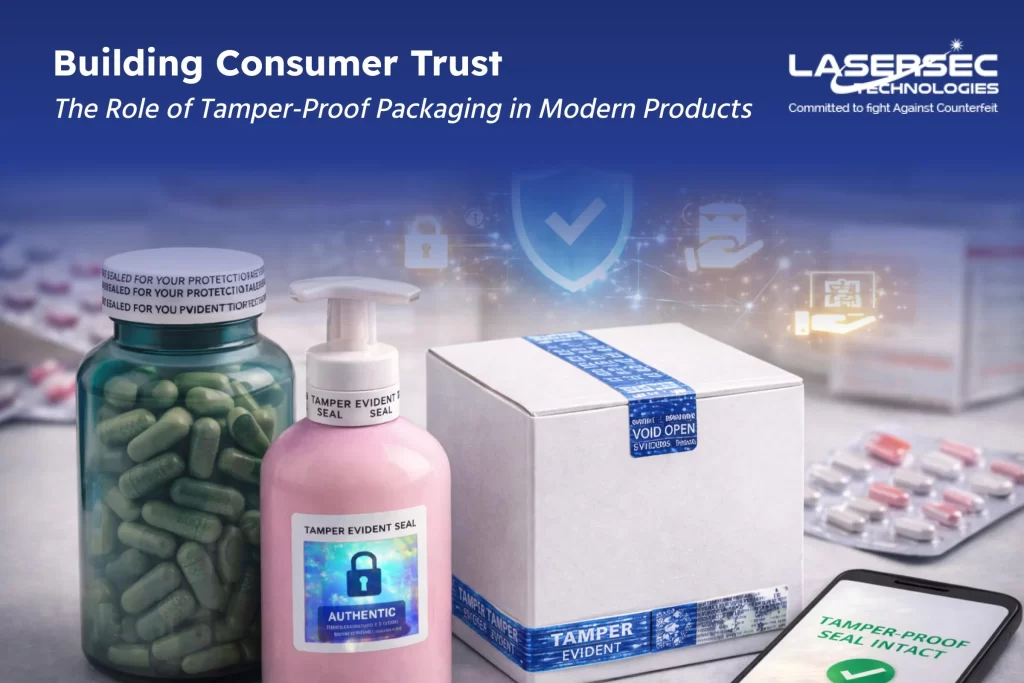
Tamper-proof packaging has therefore evolved from being a packaging enhancement to becoming a global compliance standard for product safety and brand protection using solutions like tamper proof hologram stickers and tamper-evident labels.

The Growing Importance of Tamper-Evident Packaging

Consumers today expect transparency and safety when purchasing products, especially those that affect health or personal use.

If packaging shows signs of tampering, customers immediately question the product’s safety and authenticity.

Because of this, tamper-evident packaging has become a critical requirement across many sectors.

Tamper-evident packaging solutions help ensure that:

  • Products cannot be opened without visible damage
  • Unauthorized repackaging becomes difficult
  • Counterfeiters cannot easily reuse genuine packaging
  • Consumers can identify potential tampering quickly

These protections provide an important safety layer for both manufacturers and consumers.

When tampering can be easily detected, the risk of unsafe or counterfeit products reaching the market is significantly reduced.

Industries Where Tamper-Proof Packaging Is Becoming Mandatory

Regulatory authorities and industry standards organizations are increasingly encouraging or mandating tamper-evident packaging in several sectors.

Some of the most prominent industries include:

1. Pharmaceuticals

Pharmaceutical regulators worldwide require packaging systems that protect medicines from tampering and counterfeit substitution.

Tamper-evident seals, serialized packaging, and authentication labels such as pharma holographic labels help ensure that medicines reaching patients remain safe and genuine.

2. Food and Beverage

Food safety regulations often require packaging that clearly shows whether a product has been opened before purchase.

Tamper-evident caps, seals, and labels help prevent contamination and protect consumer health. Explore more in our FMCG anti-counterfeit solutions.

3. Cosmetics and Personal Care

Cosmetic brands increasingly use tamper-evident packaging to assure consumers that products have not been opened or altered before purchase.

This helps maintain product safety and brand credibility.

4. Electronics and Consumer Goods

High-value electronics and accessories are frequently targeted by counterfeiters or repackagers.

Tamper-evident labels help ensure products remain sealed and authentic throughout distribution. Learn more in our Electronics industry solutions.

How Tamper-Proof Packaging Prevents Counterfeiting and Repackaging

Tamper-proof packaging introduces visible or structural indicators that show whether a product has been opened or altered.

Unlike traditional packaging seals, tamper-evident security features cannot be removed or reapplied without leaving clear signs of interference.

Common tamper-evident packaging technologies include:

These features make it extremely difficult for counterfeiters to open packages, replace the contents, and reseal them without detection.

As a result, tamper-proof packaging acts as a first line of defense against product tampering and counterfeit substitution.

Supporting Regulatory Compliance Through Secure Packaging

Governments and regulatory bodies are increasingly strengthening packaging requirements to improve product safety and traceability.

Many regulatory frameworks now emphasize:

  • Tamper-evident packaging requirements
  • Product authentication mechanisms
  • Supply chain transparency
  • Protection against counterfeit products

Tamper-proof packaging supports these requirements by providing a clear visual indication if a product has been interfered with.

This allows regulators, distributors, and retailers to quickly identify suspicious products during inspections.

For manufacturers exporting products across international markets, implementing tamper-evident packaging also helps demonstrate proactive compliance with global safety standards.

Strengthening Consumer Trust Through Tamper-Evident Protection

Consumer trust plays a critical role in purchasing decisions.

If customers suspect that a product has been opened, altered, or replaced, they are unlikely to use it and may avoid the brand entirely.

Tamper-evident packaging provides a simple but powerful reassurance mechanism.

When consumers see intact security seals or holographic labels such as hologram stickers, they gain confidence that the product has not been compromised.

This helps manufacturers:

  • Strengthen customer confidence in product safety
  • Reduce complaints related to product tampering
  • Protect brand credibility in competitive markets
  • Improve customer loyalty over time

Visible packaging security features also signal that the brand takes product protection seriously.

Combining Tamper-Proof Packaging with Authentication Technologies

While tamper-evident packaging prevents unauthorized opening, combining it with digital authentication technologies further strengthens product security.

For example, tamper-evident labels can be integrated with:

This combination enables both physical protection and digital verification.

Even if a product is tampered with or copied, authentication systems can help detect suspicious activity and identify counterfeit products quickly.

Together, these layers provide stronger protection across the entire product lifecycle.

How We Support Tamper-Proof Packaging and Brand Protection

At Lasersec Technologies, we provide advanced anti-counterfeit packaging solutions designed to help manufacturers implement reliable tamper-proof protection.

Our solutions integrate secure packaging features directly into product labels and packaging materials.

These include:

By combining physical tamper-evident features with authentication technologies, we help manufacturers strengthen product security across global supply chains.

To explore more solutions, visit our Product Gallery.

Why Tamper-Proof Packaging Is Essential in Modern Global Supply Chains

As global supply chains continue to expand, the risks associated with product tampering and counterfeiting are also increasing.

Tamper-proof packaging has become a critical component of modern packaging strategies because it ensures that products reach consumers in their original, uncompromised condition.

By implementing tamper-evident security features, manufacturers can strengthen compliance with global safety standards while protecting both consumers and brand reputation.

In today’s market environment, tamper-proof packaging is no longer optional. It is an essential foundation for product safety, regulatory compliance, and long-term brand protection.