Lasersec Technologies

Pharmaceutical packaging security has become a critical concern for drug manufacturers worldwide. Unit-level authentication is now the smartest way to protect every package across the supply chain.

At each stage, verifying the authenticity of the medicine becomes essential.

In many markets, counterfeit drugs and unauthorized repackaging continue to challenge pharmaceutical supply chains. Packaging may appear genuine, yet without reliable authentication systems, it can be difficult to confirm whether the medicine is authentic.

This is why pharmaceutical companies are increasingly implementing unit-level authentication systems.

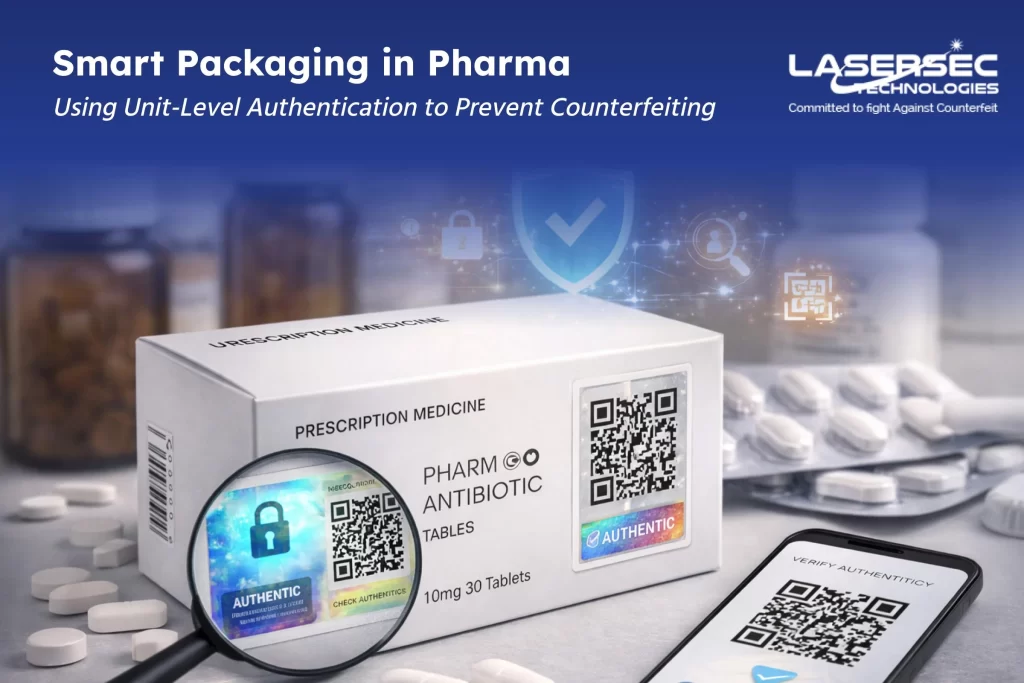
Unit-level authentication assigns a unique identity to every individual product unit, allowing manufacturers, regulators, and pharmacies to verify authenticity instantly through secure authentication technologies such as QR code authentication and Track & Trace systems.

By enabling verification at the smallest packaging level, pharmaceutical companies can significantly reduce the risk of counterfeit medicines entering the market.

The Growing Risks of Counterfeit and Repacked Medicines

Pharmaceutical products move through complex supply chains before reaching patients. These supply chains often involve multiple intermediaries such as distributors, wholesalers, and retailers.

This complexity creates opportunities for unauthorized activities, including counterfeit drug circulation and repackaging of genuine medicines.

Some common risks include:

  • Counterfeit medicines replicating genuine packaging using security hologram stickers
  • Unauthorized repackaging of original medicines
  • Reuse of genuine packaging for fake products
  • Diversion of products into unintended markets
  • Difficulty verifying authenticity at pharmacy level

These activities not only affect pharmaceutical companies but also create serious risks for patient safety.

Consequences can include:

  • Reduced trust in pharmaceutical brands
  • Regulatory compliance issues
  • Distribution channel conflicts
  • Potential health risks for patients

Without reliable authentication systems, detecting these issues early becomes extremely difficult.

What Is Unit-Level Authentication in Pharmaceutical Packaging

Unit-level authentication means assigning a unique, traceable identity to every individual medicine package.

Instead of identifying products only by batch numbers or carton-level codes, each unit receives its own authentication marker.

This is typically implemented using technologies such as:

Each identifier is connected to secure manufacturing and distribution data.

When the code is scanned, the system can instantly verify:

  • Whether the product is genuine
  • The manufacturing origin
  • Batch and production information
  • Whether the code has been duplicated

This enables reliable product verification throughout the supply chain.

How Unit-Level Authentication Prevents Fake Repackaging

One of the most common challenges in pharmaceutical markets is fake repackaging.

In this scenario, counterfeiters reuse genuine packaging materials or create look-alike packaging to insert counterfeit medicines.

Without authentication, these fake products may appear legitimate.

Unit-level authentication prevents this by ensuring that each product unit has a unique identity supported by technologies like QR code holograms.

If a counterfeiter attempts to copy or reuse a code, the authentication system can detect:

  • Duplicate code scans
  • Invalid product records
  • Suspicious verification locations

This allows manufacturers and regulators to quickly identify counterfeit activity and take corrective action. By making every package individually verifiable, unit-level authentication significantly reduces the risk of fake repackaging.

Preventing Product Diversion with Unit-Level Verification

Product diversion occurs when genuine medicines are redirected from their intended distribution markets into unauthorized regions.

This can disrupt pricing structures, violate distribution agreements, and create regulatory complications.

Unit-level authentication helps detect diversion by linking each product unit to specific manufacturing and distribution data through systems like Track & Trace technology.

When the product is scanned, the system can verify:

  • The intended market for the product
  • Whether it appears in an unexpected location
  • Whether the product has already been verified elsewhere

If the product is detected outside its authorized distribution channel, the system can immediately flag the activity. This visibility allows pharmaceutical companies to investigate unauthorized distribution and maintain better control over global supply chains.

Strengthening Pharmaceutical Compliance and Traceability

Many regulatory frameworks now require pharmaceutical manufacturers to implement serialization and traceability systems. Authorities expect companies to demonstrate the ability to verify product authenticity and track medicines across the supply chain.

Unit-level authentication supports these regulatory goals by enabling:

  • Individual product serialization
  • End-to-end supply chain traceability
  • Authentication verification at distribution points
  • Faster investigation of suspicious products

These capabilities help regulators confirm product legitimacy during inspections and market surveillance.For pharmaceutical companies operating in global markets, unit-level authentication also strengthens compliance with evolving regulatory standards using solutions such as Track & Trace systems.

Improving Patient Trust Through Product Verification

Patients rely on medicines to protect their health, which makes trust essential in the pharmaceutical industry. However, patients often cannot visually distinguish between genuine and counterfeit medicines if packaging looks similar.

Unit-level authentication enables pharmacies and even patients to verify medicines quickly using smartphone-based authentication tools. By scanning a secure QR code or authentication marker such as QR code authentication labels, users can confirm whether the product is genuine.

This level of transparency helps:

  • Improve patient confidence in medicines
  • Reduce circulation of counterfeit drugs
  • Strengthen trust in pharmaceutical brands
  • Support safer healthcare outcomes

How We Support Unit-Level Authentication in Pharmaceutical Packaging

At Lasersec Technologies, we provide advanced anti-counterfeit packaging solutions designed to help pharmaceutical manufacturers implement reliable unit-level authentication systems.

Our solutions integrate secure packaging technologies with digital authentication platforms using:

By embedding these technologies directly into pharmaceutical packaging, we help manufacturers create secure authentication systems that protect medicines across the entire supply chain. To explore more, visit our Pharma Solutions.

Why Unit-Level Authentication Is Essential for Modern Pharmaceutical Packaging

Pharmaceutical supply chains are becoming increasingly complex, and the risks associated with counterfeit medicines continue to grow. Unit-level authentication provides a powerful solution by enabling every medicine package to be individually verified.

This approach helps pharmaceutical companies detect counterfeit activity, prevent product diversion, and maintain greater visibility across their supply chains. Most importantly, it helps ensure that genuine medicines reach pharmacies and patients safely. In today’s pharmaceutical industry, unit-level authentication is no longer optional.  It is a critical foundation for protecting product integrity, regulatory compliance, and patient trust.
Share :

Frequently Asked Questions

Related Blogs

tamper-proof-food-packaging

Ready-to-eat (RTE) foods have become a major part of modern consumer lifestyles.

From packaged meals and frozen foods to ready-to-cook snacks and convenience products, consumers increasingly rely on packaged food that can be consumed quickly with minimal preparation.

However, as the demand for convenience foods grows, so does the importance of ensuring packaging safety and integrity.

Unlike traditional packaged goods, ready-to-eat products are consumed directly by consumers. Any tampering with the packaging can pose immediate health risks.

For food manufacturers and FMCG brands, ensuring that packaging clearly shows any sign of interference has become a critical safety requirement.

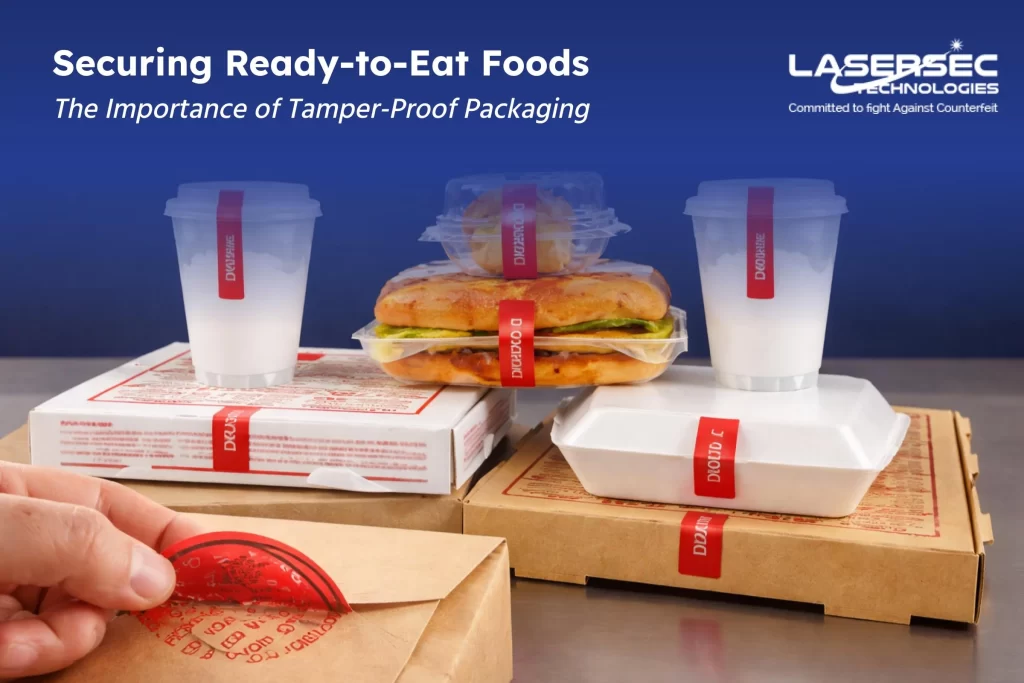
This is where tamper-proof packaging solutions such as security seals, tear bands, and tamper-evident labels play a vital role in protecting both consumers and brand reputation.

Why Ready-to-Eat Foods Require Strong Packaging Protection

Ready-to-eat foods move through complex distribution networks before reaching consumers.

Products may pass through multiple stages including manufacturing plants, cold storage facilities, transport hubs, retail stores, and delivery services.

At each stage, the product may be handled by several intermediaries.

Without proper tamper-evident protection, it can be difficult to determine whether a food package has been opened or compromised during distribution.

Even minor tampering can create serious risks such as:

  • Food contamination
  • Product spoilage
  • Loss of product freshness
  • Consumer health hazards
  • Brand reputation damage

For products that are meant to be consumed immediately, packaging integrity becomes one of the most important safety indicators.

The Rising Risk of Food Tampering in Modern Supply Chains

Food tampering incidents, although rare, can have severe consequences for both consumers and brands.

In the case of ready-to-eat products, tampering may involve:

  • Opening packaging and resealing it
  • Altering or contaminating food contents
  • Replacing products with lower-quality alternatives
  • Damaging protective seals during handling

Because ready-to-eat foods often rely on sealed packaging to maintain hygiene and freshness, any compromise in packaging integrity can undermine product safety.

For FMCG companies, preventing tampering is therefore not just a packaging concern but a food safety priority.

Key Tamper-Proof Packaging Solutions for Ready-to-Eat Foods

Modern food packaging uses several mechanisms to provide clear visual evidence of tampering.

These solutions help consumers, retailers, and inspectors easily identify whether a package has been opened or altered.

Some of the most widely used tamper-evident packaging features include:

Security Seals

Security seals are applied to food packaging to ensure that the product remains unopened until it reaches the consumer.

Once broken, the seal cannot be restored to its original state.

Security seals are commonly used for:

  • Meal trays
  • Frozen food containers
  • Jar lids
  • Beverage caps
  • Food cartons

Tear Bands and Breakable Rings

Tear bands are thin strips integrated into packaging that must be removed before opening the product.

These bands break permanently when opened, providing immediate visual evidence that the package has been accessed.

They are frequently used in:

  • Frozen food containers
  • Bottled sauces
  • Packaged beverages
  • Sealed food jars

Tamper-Evident Labels

Tamper-evident labels provide additional protection by revealing any attempt to remove or reposition the label.

These labels may include features such as:

  • Destructible material that breaks when peeled
  • Security patterns that appear when tampered with
  • Adhesive residues that indicate interference

Because these labels cannot be reapplied cleanly, they help ensure packaging authenticity.

Visual Tamper Evidence: Why It Matters to Consumers

One of the most important aspects of food packaging security is visible assurance.

Consumers often rely on simple visual cues to determine whether a product is safe to consume.

If packaging appears compromised or damaged, consumers are far less likely to purchase the product.

Clear visual tamper indicators help consumers quickly confirm that:

  • The product has not been opened
  • The packaging seal remains intact
  • The food has not been altered

This visible reassurance plays a major role in building trust between FMCG brands and consumers.

Protecting Brand Reputation in the FMCG Industry

Food brands operate in an environment where consumer trust is extremely sensitive.

A single incident involving contaminated or tampered food products can lead to:

  • Product recalls
  • Negative media coverage
  • Regulatory investigations
  • Long-term brand damage

Tamper-proof packaging acts as a preventive safeguard by ensuring that any attempt to interfere with the product becomes immediately visible.

For FMCG companies, this protection is essential for maintaining brand credibility in competitive retail markets.

Supporting Food Safety Compliance

Food safety regulations around the world increasingly emphasize the importance of packaging integrity.

Regulatory authorities expect manufacturers to implement packaging systems that protect food products from contamination and unauthorized access.

Tamper-evident packaging helps manufacturers meet these expectations by:

  • Demonstrating proactive food safety measures
  • Strengthening quality assurance processes
  • Supporting regulatory compliance during inspections
  • Providing traceable evidence of packaging integrity

For companies operating across international markets, these safeguards are especially important.

The Role of Advanced Packaging Technologies

As food supply chains grow more complex, many FMCG brands are integrating advanced technologies into their packaging systems.

These may include:

When combined with physical tamper-evident features, these technologies provide both physical and digital protection for food products.

How Lasersec Technologies Helps Secure FMCG Packaging

Lasersec Technologies develops advanced packaging security solutions designed to protect FMCG products from tampering and unauthorized interference.

Our solutions integrate tamper-evident labels, security seals, and authentication technologies that help ensure product safety throughout the supply chain.

These solutions help FMCG brands:

  • Protect ready-to-eat and frozen food packaging
  • Prevent unauthorized opening or resealing
  • Provide visible tamper evidence for consumers
  • Strengthen food safety compliance
  • Safeguard brand reputation in competitive markets

By integrating security directly into packaging, food manufacturers can maintain product integrity from production to consumption.

High-security packaging for injectable drugs

Injectable medicines are among the most critical products in modern healthcare.

From oncology therapies and vaccines to biologic and emergency medications, injectable drugs are used in situations where treatment accuracy and product integrity are essential.

Unlike many oral medications, injectable drugs enter the bloodstream directly. Any compromise in authenticity or quality can pose immediate risks to patient safety.

Yet despite strict pharmaceutical regulations, counterfeit injectables continue to appear in global supply chains.

In many cases, counterfeiters replicate packaging components such as vials, ampoules, and outer cartons so convincingly that visual inspection alone cannot confirm authenticity.

For manufacturers of sterile and injectable medicines, protecting packaging integrity has therefore become a critical part of product safety.

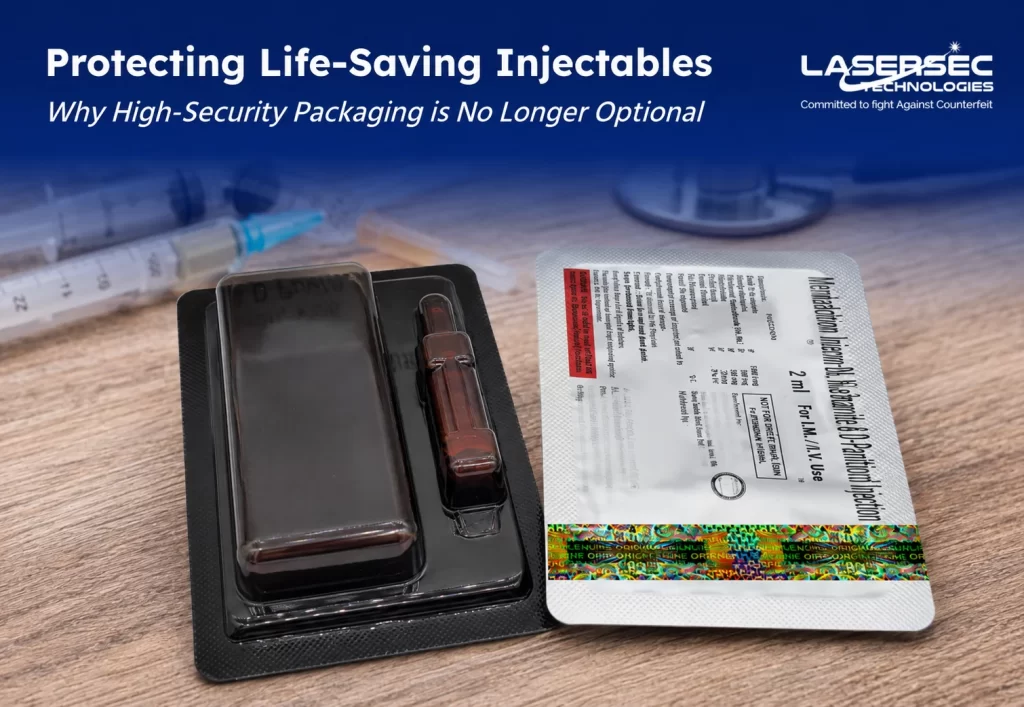
This is why high-security pharmaceutical packaging, including tamper-evident labels, holographic authentication features, and Track & Trace systems, is rapidly becoming essential for injectable drug protection.

Why Injectable Medicines Are Prime Targets for Counterfeiters

Injectable drugs are often high-value therapies used in hospitals, clinics, and specialized treatment centers.

Many injectable medicines are expensive due to complex manufacturing processes, sterile production requirements, and regulatory approvals.

These factors make injectable drugs particularly attractive targets for counterfeit operations.

Common targets include:

  • Oncology injections
  • Vaccines and biologic
  • Emergency injectable medicines
  • Hormone therapies
  • High-value specialty injectables

Counterfeiters may attempt to replicate packaging components or refill genuine containers with non-genuine substances.

Because injectable packaging formats such as vials and ampoules are relatively small, counterfeit versions can sometimes enter distribution channels without immediate detection.

The consequences of counterfeit injectables can be severe:

  • Ineffective or dangerous treatments
  • Patient safety risks
  • Hospital supply chain disruptions
  • Regulatory investigations and recalls
  • Loss of trust in pharmaceutical brands

The Unique Packaging Challenges of Injectable Medicines

Injectable medicines typically use packaging formats such as:

  • Glass vials
  • Ampoules
  • Pre-filled syringes
  • Sterile containers

These packaging types must maintain strict sterility and product stability.

However, their small size and simple structure can also make them vulnerable to tampering or counterfeit replication if additional security features are not integrated.

For example:

  • Vials may be refilled with counterfeit substances
  • Ampoules may be replicated using similar glass formats
  • Labels can be copied or replaced
  • Outer cartons may be duplicated

Because injectable products are frequently handled in clinical environments, ensuring secure and verifiable packaging is essential.

The Role of Tamper-Evident Labels in Injectable Packaging

Tamper-evident labeling is one of the most important protective mechanisms for injectable medicines.

These labels are designed to clearly reveal if a vial, ampoule, or outer packaging has been opened or altered.

Tamper-evident features may include:

  • Destructible labels that break when removed
  • VOID security indicators that appear during tampering
  • Adhesive residues that reveal interference
  • Security cuts that prevent clean label removal

Once triggered, these labels cannot be restored to their original state.

This allows healthcare providers, pharmacists, and distributors to immediately detect whether a product may have been compromised.

Strengthening Authentication with Holographic Security Features

Holographic security elements provide an additional layer of protection against counterfeit packaging replication.

Unlike traditional printing, holograms are produced using specialized optical technologies that create dynamic visual patterns.

These patterns change appearance when viewed under different lighting conditions.

For pharmaceutical packaging, holographic labels help:

  • Provide visible authentication for distributors and healthcare providers
  • Deter counterfeit packaging replication
  • Enhance brand identification on sterile packaging

Because holographic features require specialized manufacturing capabilities, they are extremely difficult for counterfeiters to reproduce accurately.

Securing Vials and Ampoules with High-Security Labeling

High-security labels can be applied directly to injectable packaging components such as:

  • Glass vials
  • Ampoule containers
  • Injection cartons
  • Sterile packaging seals

These labels serve multiple purposes.

They provide tamper evidence, authenticate the product visually, and help protect the packaging from unauthorized opening or substitution.

When applied strategically, security labels ensure that any attempt to alter the packaging becomes immediately visible.

This strengthens product integrity across distribution channels.

Integrating Serialization and Digital Verification

In addition to physical packaging security, many pharmaceutical manufacturers are implementing serialization and digital authentication systems.

Serialized identification codes allow each product unit to carry a unique digital identity.

These codes may be integrated through:

  • Data matrix codes
  • Serialized QR codes
  • Unique product identifiers linked to authentication platforms

When scanned, the system can verify whether the product matches its registered identity within a secure database.

If duplicate codes appear or if products are detected in unauthorized locations, the system can immediately flag potential counterfeit activity.

Improving Supply Chain Security for Injectable Drugs

Injectable medicines typically move through tightly controlled pharmaceutical supply chains that include manufacturers, distributors, hospitals, and pharmacies.

Despite these controls, supply chain vulnerabilities can still occur.

High-security packaging helps strengthen supply chain protection by enabling:

  • Immediate detection of tampering
  • Easier authentication for distributors and regulators
  • Better traceability through serialization systems
  • Faster identification of suspicious products

This visibility helps pharmaceutical companies prevent counterfeit injectables from reaching healthcare environments.

Why Injectable Drug Manufacturers Are Adopting High-Security Packaging

Manufacturers of sterile pharmaceutical products are increasingly recognizing that packaging security is directly connected to patient safety and regulatory compliance.

High-security packaging provides several advantages:

  • Protection against counterfeit injectables
  • Clear tamper evidence for sterile packaging
  • Improved authentication for healthcare providers
  • Integration with serialization and Track & Trace systems
  • Stronger regulatory confidence and brand protection

For life-saving injectable medicines, these protections are becoming essential rather than optional.

How Lasersec Technologies Supports Secure Injectable Packaging

At Lasersec Technologies, we develop advanced anti-counterfeit packaging and labeling solutions designed to protect high-risk pharmaceutical products.

Our high-security solutions combine tamper-evident labeling, holographic authentication technologies, and serialization-ready packaging features to secure injectable medicines throughout the supply chain.

These solutions help pharmaceutical manufacturers:

  • Protect injectable drugs from counterfeiting
  • Secure vials and ampoules against tampering
  • Strengthen packaging authentication
  • Support regulatory compliance and serialization
  • Improve supply chain transparency

By integrating advanced security technologies directly into pharmaceutical packaging, we help ensure that life-saving medicines reach healthcare providers and patients safely.