We're leading manufacturer of anti-counterfeit solutions and
safeguard brands across industries with cutting-edge security
solutions that prevent counterfeiting and ensure product
authenticity.
Counterfeit products can be really unsafe for consumers. It becomes difficult for consumers to identify the original products. The list is huge ranging from phone accessories to automobiles to apparels to watches. We all have unintentionally bought these at some point in time. Consumers are spending their money on the brands they are not getting.
Most of us count every single penny before spending and spending that amount into what is not original is heart-breaking. It’s not always about money. Counterfeits can impact consumer health too. As these products do not abide by the health and safety regulations. Counterfeits use substandard materials to lower the costing and who knows they might be using the substances not approved. Electronics items may contain cheap wiring that may catch fire, apparels might contain illegal & harmful chemical substances which may lead to allergic reactions.
For instance, Counterfeit medicines can be fatal.
Counterfeit pharmaceutical formulations can impose serious health issues and are a big threat to the life of consumers. They can create a multitude of problems not only for the consumers but also for the manufacturers and the retailers. It’s even staking the credibility of Food & Drug Administration. Counterfeit medicine is a vast market and fast growing also because of the increasing demand for cheap drugs. US govt. seized counterfeit medicines worth $28.1 million in the year 2008 (Chaudhry and Stumpf, 2011) and the numbers are growing exponentially every year. This market has grown so much that it now becomes difficult to differentiate between the two. Visual inspection has become ineffective leaving the chemical analysis as the only option to reveal the identity whether legitimate or not.
Counterfeit electronics can be dangerous
Counterfeit electronics appliances may not last long because of the substandard materials being used in their manufacturing to meet the low costing. Their internal wiring may be cheap and might even cause a fire. Even the shelf life might be less than the original one.
It’s not always about money. Sometimes, consumers are happy about buying a cheap product. But awareness must be created among the consumers about the long-term repercussions. They should receive what they are buying for. Following a few tips, one can easily identify fake products. So, be a smart consumer and a happy consumer.
Across many industries today, product safety and authenticity have become critical priorities for regulators, manufacturers, and consumers.
From pharmaceuticals and food products to cosmetics and electronics, companies are expected to ensure that their products reach customers without interference or tampering. However, global supply chains often involve multiple distributors, logistics providers, and retailers before a product reaches the end user.
This complexity creates opportunities for product tampering, repackaging, and counterfeit substitution.
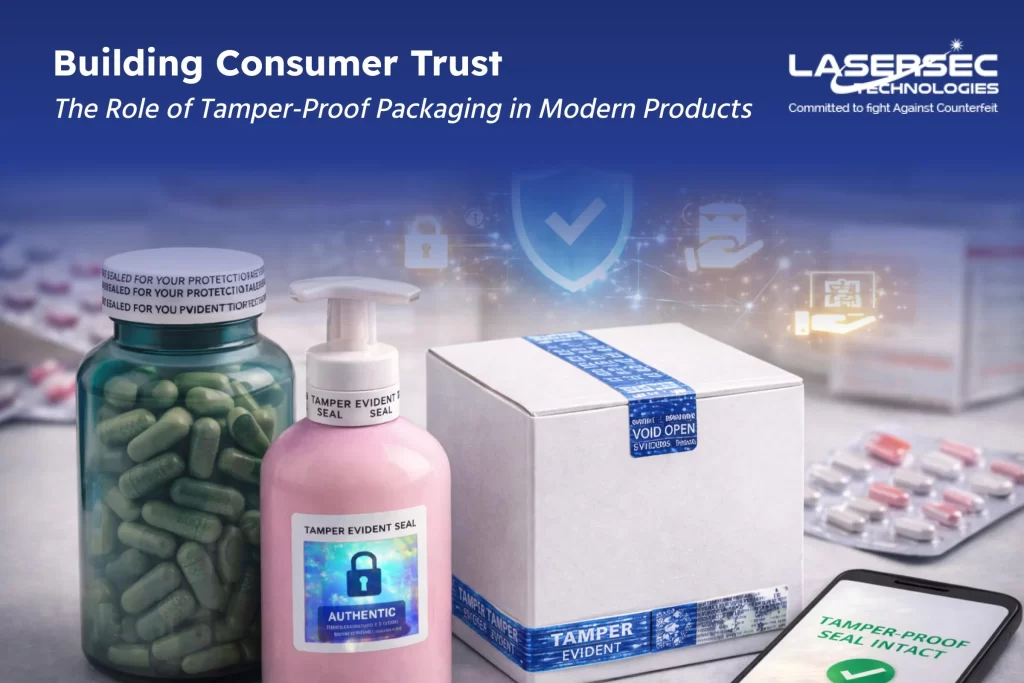
To address these risks, regulators around the world increasingly require tamper-evident or tamper-proof packaging systems that clearly indicate whether a product has been opened or altered.
Tamper-proof packaging has therefore evolved from being a packaging enhancement to becoming a global compliance standard for product safety and brand protection using solutions like tamper proof hologram stickers and tamper-evident labels.
The Growing Importance of Tamper-Evident Packaging
Consumers today expect transparency and safety when purchasing products, especially those that affect health or personal use.
If packaging shows signs of tampering, customers immediately question the product’s safety and authenticity.
Because of this, tamper-evident packaging has become a critical requirement across many sectors.
Tamper-evident packaging solutions help ensure that:
Consumers can identify potential tampering quickly
These protections provide an important safety layer for both manufacturers and consumers.
When tampering can be easily detected, the risk of unsafe or counterfeit products reaching the market is significantly reduced.
Industries Where Tamper-Proof Packaging Is Becoming Mandatory
Regulatory authorities and industry standards organizations are increasingly encouraging or mandating tamper-evident packaging in several sectors.
Some of the most prominent industries include:
1. Pharmaceuticals
Pharmaceutical regulators worldwide require packaging systems that protect medicines from tampering and counterfeit substitution.
Tamper-evident seals, serialized packaging, and authentication labels such as pharma holographic labels help ensure that medicines reaching patients remain safe and genuine.
2. Food and Beverage
Food safety regulations often require packaging that clearly shows whether a product has been opened before purchase.
Tamper-evident caps, seals, and labels help prevent contamination and protect consumer health. Explore more in our FMCG anti-counterfeit solutions.
3. Cosmetics and Personal Care
Cosmetic brands increasingly use tamper-evident packaging to assure consumers that products have not been opened or altered before purchase.
This helps maintain product safety and brand credibility.
4. Electronics and Consumer Goods
High-value electronics and accessories are frequently targeted by counterfeiters or repackagers.
Tamper-evident labels help ensure products remain sealed and authentic throughout distribution. Learn more in our Electronics industry solutions.
How Tamper-Proof Packaging Prevents Counterfeiting and Repackaging
Tamper-proof packaging introduces visible or structural indicators that show whether a product has been opened or altered.
Unlike traditional packaging seals, tamper-evident security features cannot be removed or reapplied without leaving clear signs of interference.
Common tamper-evident packaging technologies include:
Security hologram stickers integrated into packaging using security holograms
These features make it extremely difficult for counterfeiters to open packages, replace the contents, and reseal them without detection.
As a result, tamper-proof packaging acts as a first line of defense against product tampering and counterfeit substitution.
Supporting Regulatory Compliance Through Secure Packaging
Governments and regulatory bodies are increasingly strengthening packaging requirements to improve product safety and traceability.
Many regulatory frameworks now emphasize:
Tamper-evident packaging requirements
Product authentication mechanisms
Supply chain transparency
Protection against counterfeit products
Tamper-proof packaging supports these requirements by providing a clear visual indication if a product has been interfered with.
This allows regulators, distributors, and retailers to quickly identify suspicious products during inspections.
For manufacturers exporting products across international markets, implementing tamper-evident packaging also helps demonstrate proactive compliance with global safety standards.
Strengthening Consumer Trust Through Tamper-Evident Protection
Consumer trust plays a critical role in purchasing decisions.
If customers suspect that a product has been opened, altered, or replaced, they are unlikely to use it and may avoid the brand entirely.
Tamper-evident packaging provides a simple but powerful reassurance mechanism.
When consumers see intact security seals or holographic labels such as hologram stickers, they gain confidence that the product has not been compromised.
This helps manufacturers:
Strengthen customer confidence in product safety
Reduce complaints related to product tampering
Protect brand credibility in competitive markets
Improve customer loyalty over time
Visible packaging security features also signal that the brand takes product protection seriously.
Combining Tamper-Proof Packaging with Authentication Technologies
While tamper-evident packaging prevents unauthorized opening, combining it with digital authentication technologies further strengthens product security.
For example, tamper-evident labels can be integrated with:
This combination enables both physical protection and digital verification.
Even if a product is tampered with or copied, authentication systems can help detect suspicious activity and identify counterfeit products quickly.
Together, these layers provide stronger protection across the entire product lifecycle.
How We Support Tamper-Proof Packaging and Brand Protection
At Lasersec Technologies, we provide advanced anti-counterfeit packaging solutions designed to help manufacturers implement reliable tamper-proof protection.
Our solutions integrate secure packaging features directly into product labels and packaging materials.
By combining physical tamper-evident features with authentication technologies, we help manufacturers strengthen product security across global supply chains.
Why Tamper-Proof Packaging Is Essential in Modern Global Supply Chains
As global supply chains continue to expand, the risks associated with product tampering and counterfeiting are also increasing.
Tamper-proof packaging has become a critical component of modern packaging strategies because it ensures that products reach consumers in their original, uncompromised condition.
By implementing tamper-evident security features, manufacturers can strengthen compliance with global safety standards while protecting both consumers and brand reputation.
In today’s market environment, tamper-proof packaging is no longer optional. It is an essential foundation for product safety, regulatory compliance, and long-term brand protection.
Pharmaceutical packaging security has become a critical concern for drug manufacturers worldwide. Unit-level authentication is now the smartest way to protect every package across the supply chain.
At each stage, verifying the authenticity of the medicine becomes essential.
In many markets, counterfeit drugs and unauthorized repackaging continue to challenge pharmaceutical supply chains. Packaging may appear genuine, yet without reliable authentication systems, it can be difficult to confirm whether the medicine is authentic.
This is why pharmaceutical companies are increasingly implementing unit-level authentication systems.
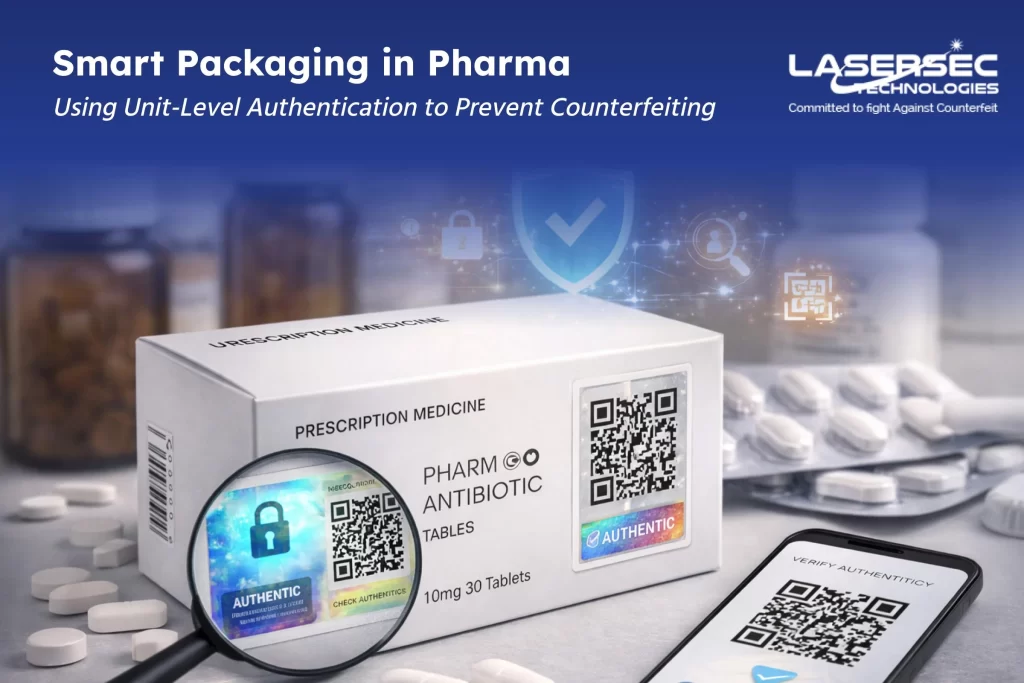
Unit-level authentication assigns a unique identity to every individual product unit, allowing manufacturers, regulators, and pharmacies to verify authenticity instantly through secure authentication technologies such as QR code authentication and Track & Trace systems.
By enabling verification at the smallest packaging level, pharmaceutical companies can significantly reduce the risk of counterfeit medicines entering the market.
The Growing Risks of Counterfeit and Repacked Medicines
Pharmaceutical products move through complex supply chains before reaching patients. These supply chains often involve multiple intermediaries such as distributors, wholesalers, and retailers.
This complexity creates opportunities for unauthorized activities, including counterfeit drug circulation and repackaging of genuine medicines.
Each identifier is connected to secure manufacturing and distribution data.
When the code is scanned, the system can instantly verify:
Whether the product is genuine
The manufacturing origin
Batch and production information
Whether the code has been duplicated
This enables reliable product verification throughout the supply chain.
How Unit-Level Authentication Prevents Fake Repackaging
One of the most common challenges in pharmaceutical markets is fake repackaging.
In this scenario, counterfeiters reuse genuine packaging materials or create look-alike packaging to insert counterfeit medicines.
Without authentication, these fake products may appear legitimate.
Unit-level authentication prevents this by ensuring that each product unit has a unique identity supported by technologies like QR code holograms.
If a counterfeiter attempts to copy or reuse a code, the authentication system can detect:
Duplicate code scans
Invalid product records
Suspicious verification locations
This allows manufacturers and regulators to quickly identify counterfeit activity and take corrective action. By making every package individually verifiable, unit-level authentication significantly reduces the risk of fake repackaging.
Preventing Product Diversion with Unit-Level Verification
Product diversion occurs when genuine medicines are redirected from their intended distribution markets into unauthorized regions.
This can disrupt pricing structures, violate distribution agreements, and create regulatory complications.
Unit-level authentication helps detect diversion by linking each product unit to specific manufacturing and distribution data through systems like Track & Trace technology.
When the product is scanned, the system can verify:
The intended market for the product
Whether it appears in an unexpected location
Whether the product has already been verified elsewhere
If the product is detected outside its authorized distribution channel, the system can immediately flag the activity. This visibility allows pharmaceutical companies to investigate unauthorized distribution and maintain better control over global supply chains.
Strengthening Pharmaceutical Compliance and Traceability
Many regulatory frameworks now require pharmaceutical manufacturers to implement serialization and traceability systems. Authorities expect companies to demonstrate the ability to verify product authenticity and track medicines across the supply chain.
Unit-level authentication supports these regulatory goals by enabling:
Individual product serialization
End-to-end supply chain traceability
Authentication verification at distribution points
Faster investigation of suspicious products
These capabilities help regulators confirm product legitimacy during inspections and market surveillance.For pharmaceutical companies operating in global markets, unit-level authentication also strengthens compliance with evolving regulatory standards using solutions such as Track & Trace systems.
Improving Patient Trust Through Product Verification
Patients rely on medicines to protect their health, which makes trust essential in the pharmaceutical industry. However, patients often cannot visually distinguish between genuine and counterfeit medicines if packaging looks similar.
Unit-level authentication enables pharmacies and even patients to verify medicines quickly using smartphone-based authentication tools. By scanning a secure QR code or authentication marker such as QR code authentication labels, users can confirm whether the product is genuine.
This level of transparency helps:
Improve patient confidence in medicines
Reduce circulation of counterfeit drugs
Strengthen trust in pharmaceutical brands
Support safer healthcare outcomes
How We Support Unit-Level Authentication in Pharmaceutical Packaging
At Lasersec Technologies, we provide advanced anti-counterfeit packaging solutions designed to help pharmaceutical manufacturers implement reliable unit-level authentication systems.
Our solutions integrate secure packaging technologies with digital authentication platforms using:
By embedding these technologies directly into pharmaceutical packaging, we help manufacturers create secure authentication systems that protect medicines across the entire supply chain. To explore more, visit our Pharma Solutions.
Why Unit-Level Authentication Is Essential for Modern Pharmaceutical Packaging
Pharmaceutical supply chains are becoming increasingly complex, and the risks associated with counterfeit medicines continue to grow. Unit-level authentication provides a powerful solution by enabling every medicine package to be individually verified.
This approach helps pharmaceutical companies detect counterfeit activity, prevent product diversion, and maintain greater visibility across their supply chains. Most importantly, it helps ensure that genuine medicines reach pharmacies and patients safely. In today’s pharmaceutical industry, unit-level authentication is no longer optional. It is a critical foundation for protecting product integrity, regulatory compliance, and patient trust.
Injectable medicines are among the most critical products in modern healthcare.
From oncology therapies and vaccines to biologic and emergency medications, injectable drugs are used in situations where treatment accuracy and product integrity are essential.
Unlike many oral medications, injectable drugs enter the bloodstream directly. Any compromise in authenticity or quality can pose immediate risks to patient safety.
Yet despite strict pharmaceutical regulations, counterfeit injectables continue to appear in global supply chains.
In many cases, counterfeiters replicate packaging components such as vials, ampoules, and outer cartons so convincingly that visual inspection alone cannot confirm authenticity.
For manufacturers of sterile and injectable medicines, protecting packaging integrity has therefore become a critical part of product safety.
Why Injectable Medicines Are Prime Targets for Counterfeiters
Injectable drugs are often high-value therapies used in hospitals, clinics, and specialized treatment centers.
Many injectable medicines are expensive due to complex manufacturing processes, sterile production requirements, and regulatory approvals.
These factors make injectable drugs particularly attractive targets for counterfeit operations.
Common targets include:
Oncology injections
Vaccines and biologic
Emergency injectable medicines
Hormone therapies
High-value specialty injectables
Counterfeiters may attempt to replicate packaging components or refill genuine containers with non-genuine substances.
Because injectable packaging formats such as vials and ampoules are relatively small, counterfeit versions can sometimes enter distribution channels without immediate detection.
The consequences of counterfeit injectables can be severe:
Ineffective or dangerous treatments
Patient safety risks
Hospital supply chain disruptions
Regulatory investigations and recalls
Loss of trust in pharmaceutical brands
The Unique Packaging Challenges of Injectable Medicines
Injectable medicines typically use packaging formats such as:
Glass vials
Ampoules
Pre-filled syringes
Sterile containers
These packaging types must maintain strict sterility and product stability.
However, their small size and simple structure can also make them vulnerable to tampering or counterfeit replication if additional security features are not integrated.
For example:
Vials may be refilled with counterfeit substances
Ampoules may be replicated using similar glass formats
Labels can be copied or replaced
Outer cartons may be duplicated
Because injectable products are frequently handled in clinical environments, ensuring secure and verifiable packaging is essential.
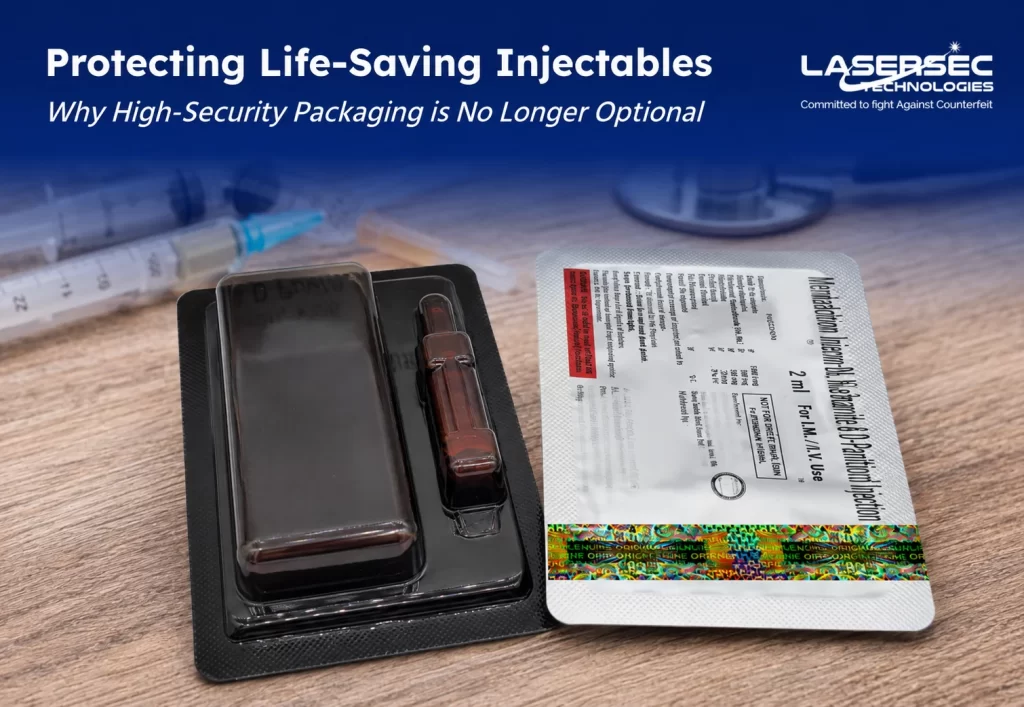
The Role of Tamper-Evident Labels in Injectable Packaging
Tamper-evident labeling is one of the most important protective mechanisms for injectable medicines.
These labels are designed to clearly reveal if a vial, ampoule, or outer packaging has been opened or altered.
Provide visible authentication for distributors and healthcare providers
Deter counterfeit packaging replication
Enhance brand identification on sterile packaging
Because holographic features require specialized manufacturing capabilities, they are extremely difficult for counterfeiters to reproduce accurately.
Securing Vials and Ampoules with High-Security Labeling
High-security labels can be applied directly to injectable packaging components such as:
Glass vials
Ampoule containers
Injection cartons
Sterile packaging seals
These labels serve multiple purposes.
They provide tamper evidence, authenticate the product visually, and help protect the packaging from unauthorized opening or substitution.
When applied strategically, security labels ensure that any attempt to alter the packaging becomes immediately visible.
This strengthens product integrity across distribution channels.
Integrating Serialization and Digital Verification
In addition to physical packaging security, many pharmaceutical manufacturers are implementing serialization and digital authentication systems.
Serialized identification codes allow each product unit to carry a unique digital identity.
These codes may be integrated through:
Data matrix codes
Serialized QR codes
Unique product identifiers linked to authentication platforms
When scanned, the system can verify whether the product matches its registered identity within a secure database.
If duplicate codes appear or if products are detected in unauthorized locations, the system can immediately flag potential counterfeit activity.
Improving Supply Chain Security for Injectable Drugs
Injectable medicines typically move through tightly controlled pharmaceutical supply chains that include manufacturers, distributors, hospitals, and pharmacies.
Despite these controls, supply chain vulnerabilities can still occur.
High-security packaging helps strengthen supply chain protection by enabling:
Immediate detection of tampering
Easier authentication for distributors and regulators
Better traceability through serialization systems
Faster identification of suspicious products
This visibility helps pharmaceutical companies prevent counterfeit injectables from reaching healthcare environments.
Why Injectable Drug Manufacturers Are Adopting High-Security Packaging
Manufacturers of sterile pharmaceutical products are increasingly recognizing that packaging security is directly connected to patient safety and regulatory compliance.
High-security packaging provides several advantages:
Stronger regulatory confidence and brand protection
For life-saving injectable medicines, these protections are becoming essential rather than optional.
How Lasersec Technologies Supports Secure Injectable Packaging
At Lasersec Technologies, we develop advanced anti-counterfeit packaging and labeling solutions designed to protect high-risk pharmaceutical products.
Our high-security solutions combine tamper-evident labeling, holographic authentication technologies, and serialization-ready packaging features to secure injectable medicines throughout the supply chain.
These solutions help pharmaceutical manufacturers:
Protect injectable drugs from counterfeiting
Secure vials and ampoules against tampering
Strengthen packaging authentication
Support regulatory compliance and serialization
Improve supply chain transparency
By integrating advanced security technologies directly into pharmaceutical packaging, we help ensure that life-saving medicines reach healthcare providers and patients safely.
Sustainability is becoming a major priority for FMCG brands worldwide.
Many companies are redesigning packaging systems to reduce plastic waste, minimize environmental impact, and encourage circular consumption models.
One of the most widely adopted approaches is refillable packaging.
Consumers purchase a durable container once and then refill it with product pouches, sachets, or refill packs. This model significantly reduces packaging waste and supports long-term sustainability goals.
However, while refillable packaging improves environmental performance, it also introduces new security challenges.
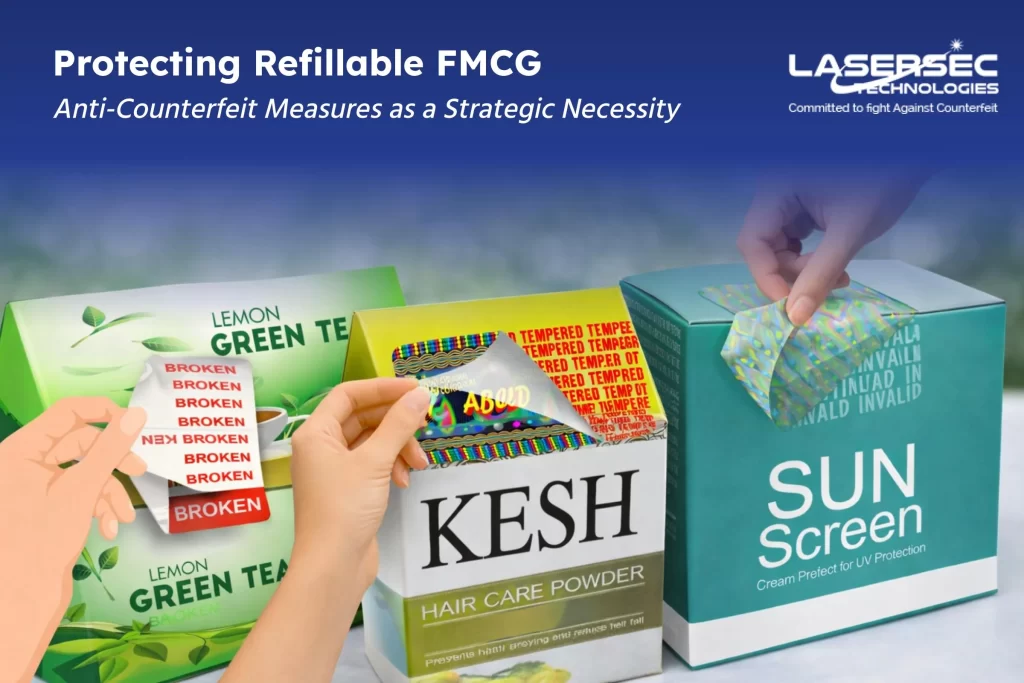
Refill packs and reusable containers can become targets for counterfeit products if authentication mechanisms are not integrated into the packaging system.
For FMCG brands focused on sustainability innovation, ensuring both environmental responsibility and product authenticity is becoming increasingly important.
The Rise of Refillable Packaging in the FMCG Industry
Refillable packaging systems are becoming increasingly common across FMCG categories such as:
Personal care products
Household cleaning products
Liquid detergents
Beauty and skincare products
Food and beverage concentrates
In these systems, consumers typically purchase a primary container that is designed for repeated use.
Refill packs allow the consumer to replenish the product without discarding the main container.
This model offers several sustainability benefits:
Reduced plastic consumption
Lower packaging waste
Reduced transportation impact due to lighter refill packs
Improved lifecycle efficiency for packaging materials
While these advantages are significant, refillable systems also create new vulnerabilities for product authenticity.
The Counterfeit Risk in Refillable FMCG Products
In refill-based systems, the original container often remains in use for a long period of time.
Consumers rely on refill packs to maintain product quality and performance.
However, counterfeiters may attempt to exploit this system by introducing fake refill packs or unauthorized refilling practices.
Unauthorized refill stations offering diluted or fake products
Reused containers filled with non-genuine formulations
Repackaged counterfeit products sold as genuine refills
Because consumers already possess the original container, they may assume that any refill product associated with that brand is authentic.
Without authentication features, distinguishing genuine refills from counterfeit ones becomes extremely difficult.
Why Traditional Packaging Security May Not Work for Refill Systems
Traditional anti-counterfeit strategies often focus on protecting the primary product packaging.
However, refill systems change the structure of product distribution.
Instead of purchasing a completely new packaged product each time, consumers rely on secondary refill formats.
These refill packs are often:
Smaller
Flexible pouches or sachets
Lightweight packaging formats
Because refill packs are designed to reduce material usage, they may contain fewer physical security elements.
This creates opportunities for counterfeiters to replicate packaging designs more easily.
For FMCG brands investing in sustainability-driven packaging systems, security must evolve alongside sustainability initiatives.
The Authentication Challenges of Reusable Containers
Reusable containers present another layer of complexity for product authentication.
Since the primary container may remain in use for months or even years, the container itself does not necessarily verify the authenticity of the product inside.
A consumer may refill the container multiple times, but there is no guarantee that the refill used is genuine.
Without proper authentication mechanisms, several issues can arise:
Consumers unknowingly using counterfeit refills
Diluted or substandard products affecting performance
Negative brand experiences caused by fake formulations
Difficulty tracing product origin
In such scenarios, the brand may still be blamed even though the counterfeit refill was not produced by the manufacturer.
Integrating Authentication into Refill Packaging
To address these risks, FMCG brands are increasingly integrating authentication technologies directly into refill packaging systems.
These technologies help verify product authenticity while maintaining the sustainability advantages of refill models.
These features allow consumers, retailers, and manufacturers to confirm that the refill product originates from an authorized source.
How QR-Based Authentication Supports Refillable Packaging
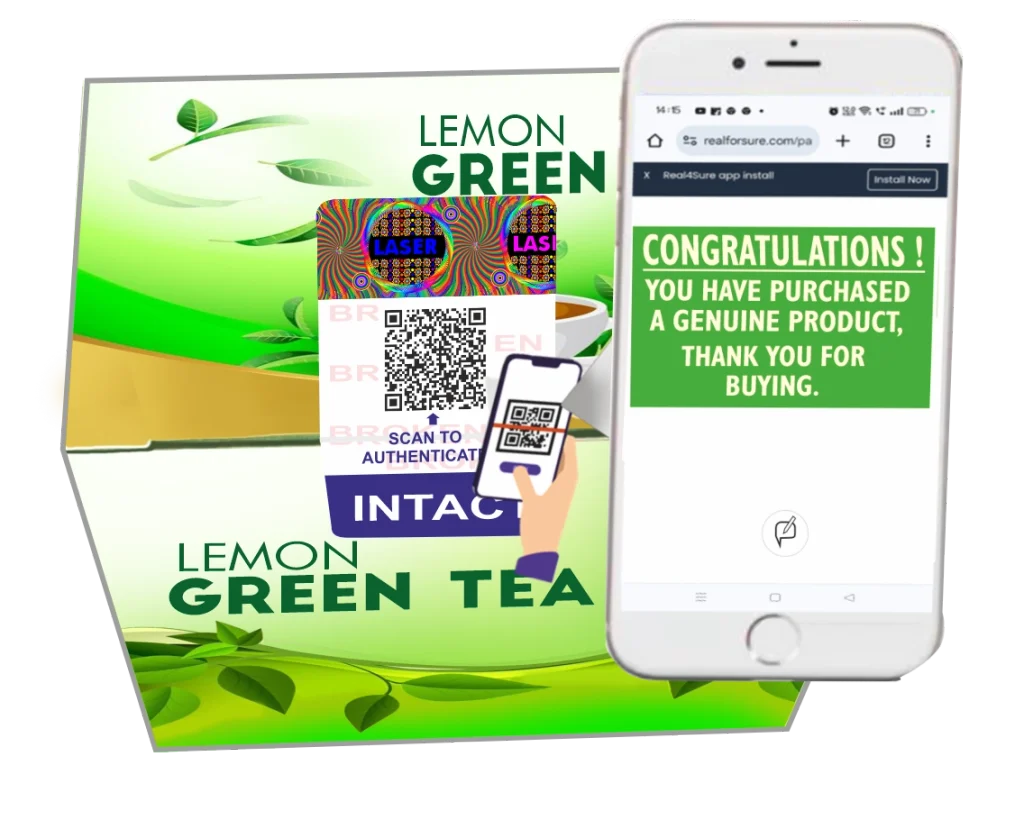
QR code authentication is particularly well suited for refill packaging because it requires minimal packaging material while enabling powerful verification capabilities.
Each refill pack can carry a unique scannable QR code linked to a secure authentication system.
When scanned, the system can verify:
Whether the refill product is genuine
Manufacturing origin and batch details
Product authenticity status
Brand verification information
This creates a simple verification process that consumers can perform using their smartphones.
If duplicate scans or suspicious activity occurs, the system can flag potential counterfeit distribution.
Supporting Transparency in Sustainable FMCG Supply Chains
Consumers who choose refillable products are often highly conscious about sustainability and brand ethics.
These consumers value transparency regarding product origin, formulation quality, and environmental impact.
Authentication technologies allow brands to provide this transparency through digital engagement.
When consumers scan refill packaging, brands can share information such as:
Product authenticity confirmation
Sustainability commitments
Responsible sourcing practices
Product usage guidance
This interaction strengthens consumer trust while reinforcing the brand’s sustainability messaging.
Why Sustainability and Security Must Work Together
Sustainability innovations should not compromise product security.
If refill systems are vulnerable to counterfeit infiltration, the consequences can include:
Consumer safety concerns
Product performance failures
Damage to brand credibility
Loss of consumer trust in refill systems
Therefore, packaging innovators and sustainability leaders must design refillable packaging systems that balance environmental responsibility with authentication security.
Integrating anti-counterfeit technologies ensures that refillable models remain safe, reliable, and trustworthy.
How Lasersec Technologies Supports Secure Refillable Packaging
At Lasersec Technologies, we help FMCG brands integrate authentication and anti-counterfeit protection into modern packaging systems.
Our solutions combine secure holographic labels, QR-based authentication, tamper-evident packaging features, and Track & Trace systems to protect products across evolving packaging formats.
These technologies help FMCG brands:
Prevent counterfeit refill products
Protect reusable container ecosystems
Enable consumer-level product authentication
Strengthen supply chain visibility
Support sustainable packaging strategies without compromising security
By integrating smart authentication technologies into refill packaging, brands can maintain both environmental responsibility and product integrity.
A pharmaceutical product begins its journey inside a controlled manufacturing environment where every process is carefully monitored.
The formulation is verified, production batches are documented, and packaging operations follow strict regulatory protocols. Once the medicine is packaged, it begins moving through warehouses, distributors, logistics partners, pharmacies, and healthcare facilities before reaching patients.
However, the moment a product leaves the manufacturing facility, visibility often becomes limited.
Without strong traceability systems, pharmaceutical companies may struggle to monitor product movement across global supply chains. This lack of visibility creates opportunities for counterfeit infiltration, product diversion, and unauthorized distribution.
To address these risks, pharmaceutical manufacturers are increasingly adopting Track & Trace technology combined with secure packaging solutions.
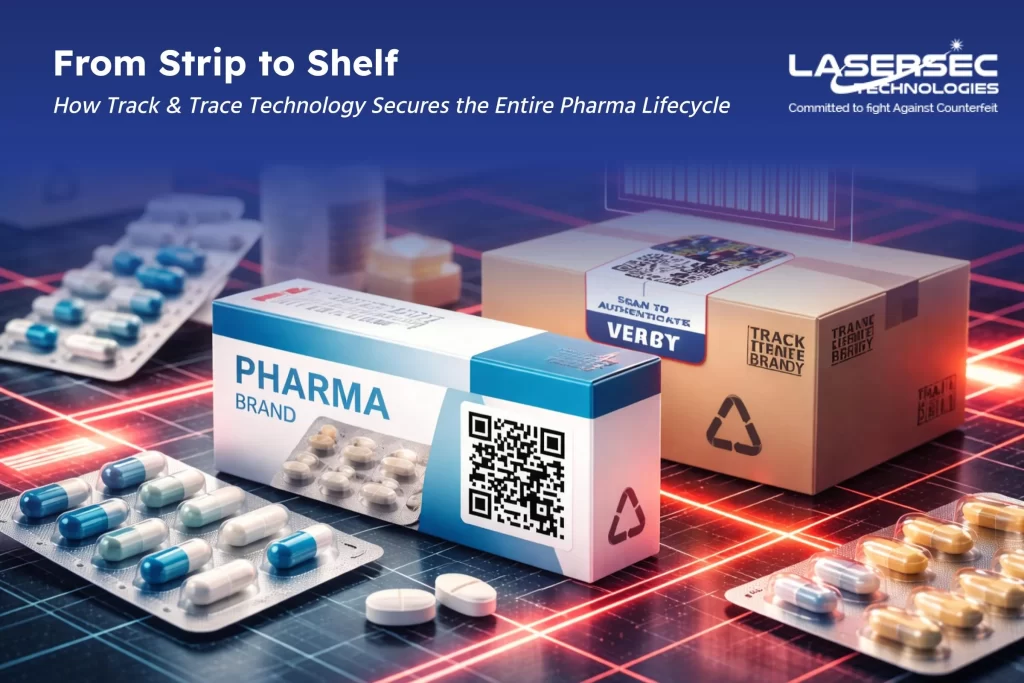
By integrating serialization, tamper-evident packaging, and digital product identities, Track & Trace systems enable manufacturers to secure the pharmaceutical life cycle—from the packaging strip to the pharmacy shelf.
Why End-to-End Traceability Is Critical in Modern Pharmaceutical Supply Chains
The pharmaceutical supply chain is one of the most complex and tightly regulated supply networks in the world.
Medicines often move across multiple countries and pass through various intermediaries including:
Manufacturing facilities
Packaging lines
Distribution warehouses
Export and import channels
Regional distributors
Pharmacies and healthcare providers
At each stage, the product may face risks such as:
Counterfeit drug infiltration
Unauthorized parallel trade
Repackaging or relabeling
Diversion to unapproved markets
Without reliable traceability systems, identifying where a product originated or how it entered a specific market becomes extremely difficult.
This is why global regulatory frameworks increasingly require serialization and Track & Trace systems that allow medicines to be tracked throughout their life cycle.
The Limitations of Traditional Pharmaceutical Packaging
Traditional pharmaceutical packaging primarily focuses on protecting the product from environmental exposure such as moisture, contamination, or physical damage.
While this is essential for product stability, conventional packaging alone cannot provide full supply chain visibility.
Standard packaging elements such as:
Printed batch numbers
bar codes
Product labeling
Packaging artwork
are designed for identification and logistics rather than authentication and traceability.
These elements can be copied or replicated by counterfeiters, making it difficult to confirm product authenticity based solely on visual inspection.
To secure modern pharmaceutical supply chains, packaging must evolve beyond protection and become a source of verifiable product identity.
What Is Track & Trace Technology in Pharmaceutical Packaging
Track & Trace technology enables pharmaceutical manufacturers to assign a unique digital identity to every product unit.
This identity is typically created through serialization during the packaging process.
Serialized identifiers may include:
Unique QR codes
Data Matrix codes
Alphanumeric product identifiers
Each code is linked to a secure database containing product information such as:
Manufacturing origin
Batch and production details
Packaging line information
Distribution records
Every time the product moves through the supply chain and the code is scanned, the system records a verification event. This creates a transparent history of the product’s movement from production to final delivery.
From Strip to Shelf: How Track & Trace Secures Each Stage of the life cycle
Track & Trace systems secure the pharmaceutical life cycle by providing visibility at every stage of product movement.
The process begins during primary packaging, such as blister strips or strip foils, where serialization codes may be applied or linked to the packaging unit.
During secondary packaging, serialized codes are integrated into cartons or labels that carry the product identity.
At this stage, tamper-evident packaging features are often added to ensure that the product cannot be opened or altered without detection.
As the product moves through warehouses and distribution channels, each scan event confirms that the product remains authentic and within authorized supply networks.
By the time the medicine reaches pharmacies or healthcare providers, its complete traceability record can be verified through the Track & Trace system.
The Role of Tamper-Evident Packaging in life cycle Security
If tampering occurs, the packaging clearly indicates interference, allowing distributors and regulators to identify compromised products quickly.
When combined with serialization, tamper-evident packaging provides both physical protection and digital verification.
Understanding the Role of Digital Twins in Pharmaceutical Traceability
A key concept in modern Track & Trace systems is the creation of a digital twin for each pharmaceutical product unit.
A digital twin is a digital representation of a physical product that exists within a secure data environment.
When a serialized product is packaged, its digital twin is created within the authentication platform.
This digital identity contains important information including:
Manufacturing records
Packaging data
Supply chain verification history
Product authentication status
Whenever the product code is scanned, the system verifies whether the physical product matches its digital twin.
If discrepancies appear—such as duplicate codes or scans in unauthorized regions—the system immediately flags potential counterfeit activity. This allows manufacturers to detect risks early and respond quickly.
Strengthening Regulatory Compliance with Track & Trace Systems
Regulatory agencies around the world are increasingly requiring pharmaceutical companies to implement traceability systems.
These requirements are designed to improve transparency, prevent counterfeit drugs, and protect patient safety.
Track & Trace systems help manufacturers meet these regulatory expectations by enabling:
Unit-level serialization
Supply chain verification
Product authentication
Rapid recall management
Distribution monitoring
When regulators or inspectors need to verify a product’s origin or authenticity, the system can provide instant verification data. This strengthens regulatory confidence and reduces compliance risks.
Why Pharmaceutical Manufacturers Are Upgrading to End-to-End Traceability
Pharmaceutical manufacturers are increasingly moving toward integrated packaging and traceability systems rather than relying on isolated security measures.
End-to-end Track & Trace systems provide several strategic benefits:
Strong protection against counterfeit drug infiltration
Real-time visibility across supply chains
Faster identification of unauthorized distribution
Improved recall management capabilities
Stronger compliance with global regulatory requirements
By combining serialization, tamper-evident packaging, and authentication systems, manufacturers can secure their products throughout the entire life cycle.
How Lasersec Technologies Supports End-to-End Pharmaceutical Security
At Lasersec Technologies, we provide integrated pharmaceutical packaging and authentication solutions designed to support end-to-end product security.
Our technologies combine secure packaging features, serialization-ready labeling, holographic authentication elements, and Track & Trace systems to create a comprehensive pharmaceutical protection framework.
These solutions help pharmaceutical manufacturers:
Implement reliable product serialization
Protect packaging through tamper-evident technologies
Enable secure authentication through QR-based verification
Improve supply chain monitoring
Strengthen regulatory compliance and brand protection
By integrating physical packaging security with digital traceability systems, we help pharmaceutical companies maintain full control over their products from manufacturing to patient delivery.