Lasersec Technologies

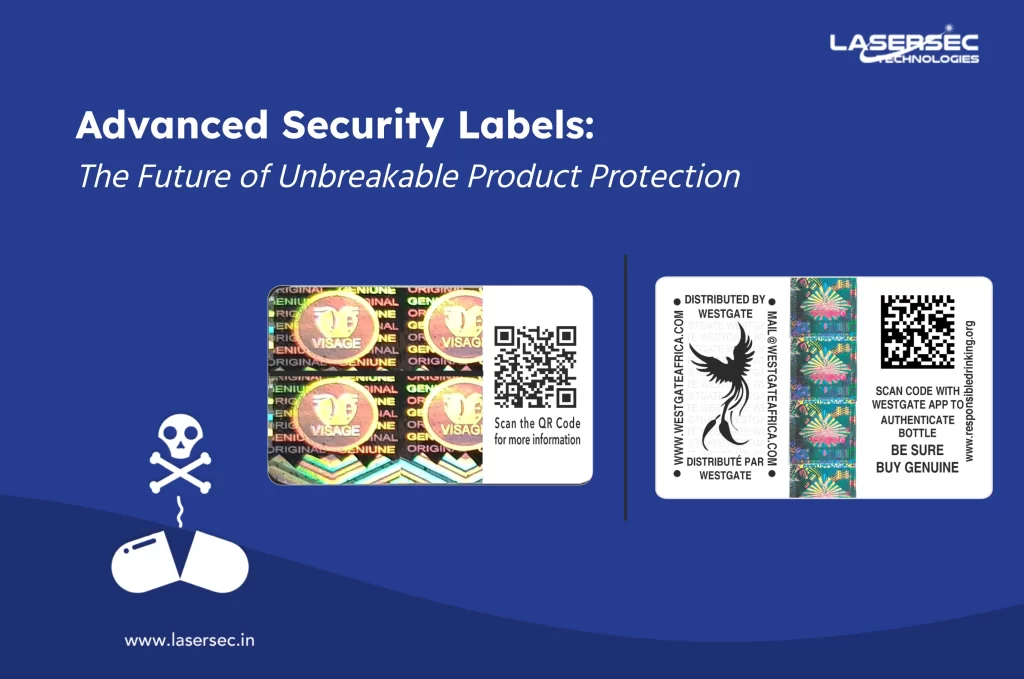
Advanced Security Labels

What if there was a way to make counterfeiting not just challenging but nearly impossible? Advanced Security Labels are revolutionizing product security, providing brands and industries with cutting-edge solutions to combat the growing counterfeit epidemic.

Counterfeiting affects us all—from the trust we place in the brands we buy to the safety of critical products like medicines and electronics. Advanced Security Labels offer a groundbreaking solution, ensuring that every product is exactly what it claims to be.

Why Counterfeiting Demands Smarter Solutions

From luxury goods and electronics to life-saving medications, counterfeit products have infiltrated every sector. Beyond financial losses, these imitations can jeopardize lives, disrupt markets, and erode trust in even the most reputable brands.

Traditional security methods like holographic seals, barcodes, and RFID Labels have been useful. However, with counterfeiters employing increasingly sophisticated techniques, these methods are no longer foolproof. Advanced Security Labels represent a transformative leap forward, offering a future-proof and unbreakable approach to safeguarding products.

What Are Advanced Security Labels, and How Do They Work?

Advanced Security Labels act as a digital fingerprint for products—uniquely encrypted, tamper-proof, and unhackable. Built on cutting-edge technology, they encode information in ways that become irreversibly altered when tampered with.

Key Features of Advanced Security Labels:

  • Tamper-Proof Security: Any attempt to manipulate the tag alters its state permanently, making tampering instantly detectable.
  • Scalable Authentication: Products equipped with these Labels can be authenticated within seconds, streamlining supply chain transparency.
  • Enhanced Traceability: These Labels store immutable records of a product’s journey from origin to end-user, bolstering trust and accountability.

Real-World Applications of Advanced Security Labels

  • Shutting Down Counterfeiters: Advanced Security Labels don’t just make counterfeiting difficult—they render it virtually impossible. Their complex encryption creates barriers that current counterfeit technology cannot breach.
    Example: Imagine purchasing a premium watch online. When it arrives, a simple scan confirms its authenticity, ensuring it’s not a convincing knock-off.
  • Strengthening Supply Chain Control: Advanced Security Labels empower brands with granular visibility into their supply chains, making it easy to identify and mitigate unauthorized substitutions or breaches.
    Example: A tech company uses these Labels on microchips to detect counterfeit components instantly, ensuring defective chips don’t reach consumers.
  • Empowering Consumers: With Advanced Security Labels, authenticity checks are at consumers’ fingertips. They can verify products using their smartphones, fostering trust and confidence in brands.
  • Broad Industry Applications: Advanced Security Labels adapt seamlessly to diverse industries, including:
  1. Pharmaceuticals: Guaranteeing that patients receive genuine, safe medications.
  2. Luxury Goods: Safeguarding exclusivity for brands and protecting their reputation.
  3. Technology: Ensuring component authenticity in critical devices.
  4. Fine Art and Collectibles: Verifying provenance for high-value investments.

Success Stories of Advanced Security Tag Implementation

  • Pharmaceutical Industry: In an environment where counterfeit drugs pose grave health risks, these Labels ensure that every package reaching a patient is genuine. This enhances patient safety and upholds brand integrity for pharmaceutical companies.
  • Luxury Market: Premium brands leverage Advanced Security Labels to confirm the authenticity of high-value items like bags, shoes, and watches, reducing the risk of counterfeit products diluting their reputation.
  • Technology Sector: Hardware companies apply these Labels on critical components, minimizing the risk of defective or unauthorized items infiltrating their supply chain.

Why Advanced Security Labels Are a Game-Changer

As technology continues to advance, Advanced Security Labels are setting new standards in anti-counterfeit security. Their combination of advanced encryption, adaptability across industries, and user-friendly verification methods ensures unprecedented safety, trust, and product integrity.

Key Benefits Recap:

  • Unbreakable Security: Built on principles that cannot be circumvented by traditional hacking techniques.
  • Supply Chain Transparency: End-to-end visibility with tamper-proof authentication records.
  • Consumer Empowerment: Simplified authenticity checks, improving consumer confidence.

Embracing the Future of Product Security

Counterfeit prevention is no longer optional—it’s an essential strategy for protecting businesses, consumers, and industries in a rapidly evolving market. By adopting Advanced Security Labels, brands can establish robust defenses against counterfeiting, ensuring product integrity, consumer trust, and supply chain transparency.

At Lasersec Technologies, we are committed to innovation in anti-counterfeit solutions. With our expertise in Advanced Security Labels, holograms, and secure packaging technologies, we collaborate with businesses to address their unique challenges. Our goal is to help you stay ahead in the fight against counterfeiting while empowering your brand with unparalleled security.

Ready to explore how Advanced Security Labels can transform your product security? Reach out to us at mktg@lasersec.in or call us at +91-9810213127.
Share :

Frequently Asked Questions

Related Blogs

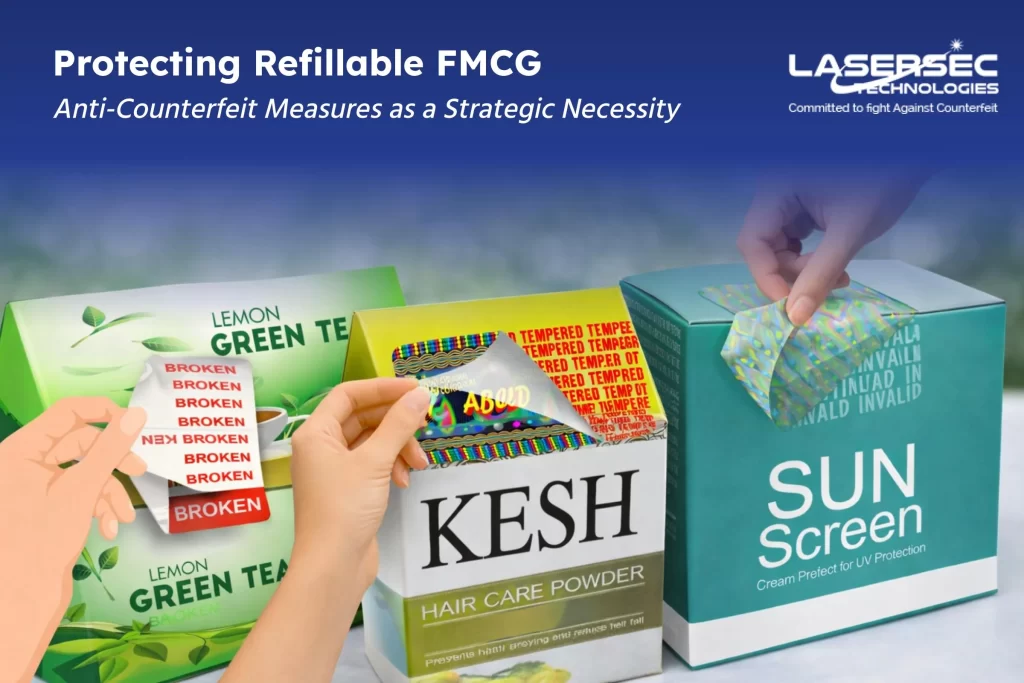
Anti-counterfeit packaging for refillable FMCG products

Sustainability is becoming a major priority for FMCG brands worldwide.

Many companies are redesigning packaging systems to reduce plastic waste, minimize environmental impact, and encourage circular consumption models.

One of the most widely adopted approaches is refillable packaging.

Consumers purchase a durable container once and then refill it with product pouches, sachets, or refill packs. This model significantly reduces packaging waste and supports long-term sustainability goals.

However, while refillable packaging improves environmental performance, it also introduces new security challenges.

Refill packs and reusable containers can become targets for counterfeit products if authentication mechanisms are not integrated into the packaging system.

For FMCG brands focused on sustainability innovation, ensuring both environmental responsibility and product authenticity is becoming increasingly important.

The Rise of Refillable Packaging in the FMCG Industry

Refillable packaging systems are becoming increasingly common across FMCG categories such as:

  • Personal care products
  • Household cleaning products
  • Liquid detergents
  • Beauty and skincare products
  • Food and beverage concentrates

In these systems, consumers typically purchase a primary container that is designed for repeated use.

Refill packs allow the consumer to replenish the product without discarding the main container.

This model offers several sustainability benefits:

  • Reduced plastic consumption
  • Lower packaging waste
  • Reduced transportation impact due to lighter refill packs
  • Improved lifecycle efficiency for packaging materials
While these advantages are significant, refillable systems also create new vulnerabilities for product authenticity.

The Counterfeit Risk in Refillable FMCG Products

In refill-based systems, the original container often remains in use for a long period of time.

Consumers rely on refill packs to maintain product quality and performance.

However, counterfeiters may attempt to exploit this system by introducing fake refill packs or unauthorized refilling practices.

Some common risks include:

  • Counterfeit refill pouches imitating branded refill packs
  • Unauthorized refill stations offering diluted or fake products
  • Reused containers filled with non-genuine formulations
  • Repackaged counterfeit products sold as genuine refills

Because consumers already possess the original container, they may assume that any refill product associated with that brand is authentic.

Without authentication features, distinguishing genuine refills from counterfeit ones becomes extremely difficult.

Why Traditional Packaging Security May Not Work for Refill Systems

Traditional anti-counterfeit strategies often focus on protecting the primary product packaging.

However, refill systems change the structure of product distribution.

Instead of purchasing a completely new packaged product each time, consumers rely on secondary refill formats.

These refill packs are often:

  • Smaller
  • Flexible pouches or sachets
  • Lightweight packaging formats

Because refill packs are designed to reduce material usage, they may contain fewer physical security elements.

This creates opportunities for counterfeiters to replicate packaging designs more easily.

For FMCG brands investing in sustainability-driven packaging systems, security must evolve alongside sustainability initiatives.

The Authentication Challenges of Reusable Containers

Reusable containers present another layer of complexity for product authentication.

Since the primary container may remain in use for months or even years, the container itself does not necessarily verify the authenticity of the product inside.

A consumer may refill the container multiple times, but there is no guarantee that the refill used is genuine.

Without proper authentication mechanisms, several issues can arise:

  • Consumers unknowingly using counterfeit refills
  • Diluted or substandard products affecting performance
  • Negative brand experiences caused by fake formulations
  • Difficulty tracing product origin
In such scenarios, the brand may still be blamed even though the counterfeit refill was not produced by the manufacturer.

Integrating Authentication into Refill Packaging

To address these risks, FMCG brands are increasingly integrating authentication technologies directly into refill packaging systems.

These technologies help verify product authenticity while maintaining the sustainability advantages of refill models.

Common authentication solutions include:

These features allow consumers, retailers, and manufacturers to confirm that the refill product originates from an authorized source.

How QR-Based Authentication Supports Refillable Packaging

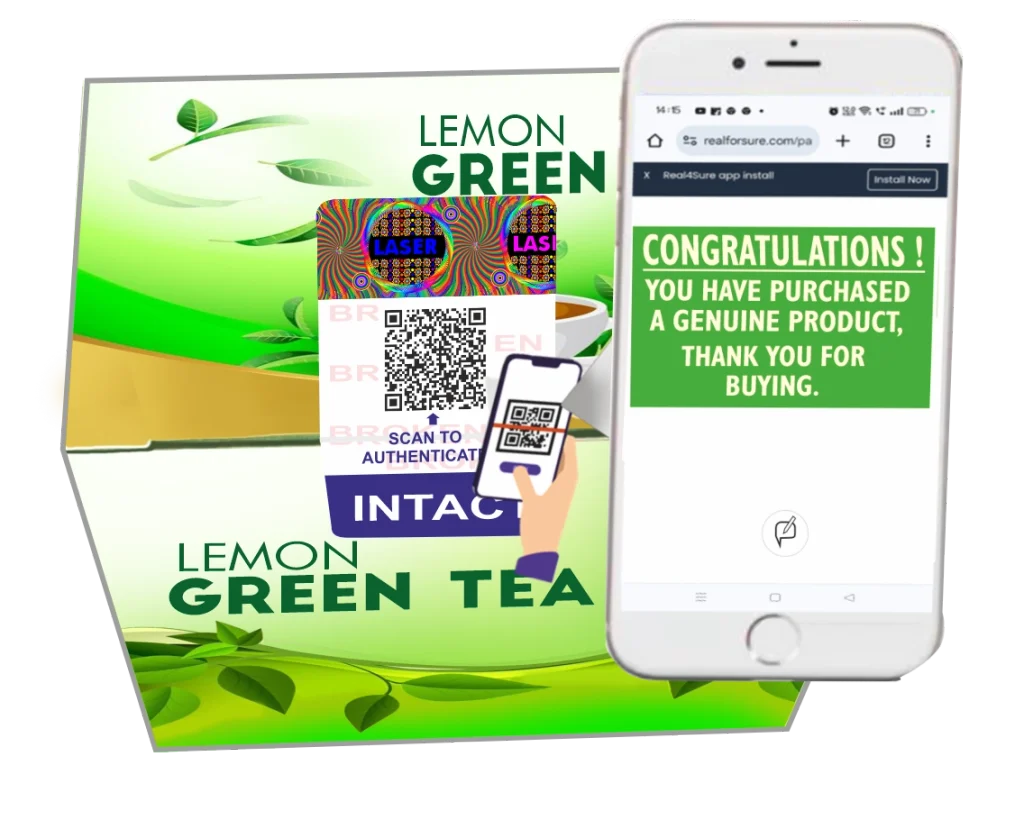
QR code authentication is particularly well suited for refill packaging because it requires minimal packaging material while enabling powerful verification capabilities.

Each refill pack can carry a unique scannable QR code linked to a secure authentication system.

When scanned, the system can verify:

  • Whether the refill product is genuine
  • Manufacturing origin and batch details
  • Product authenticity status
  • Brand verification information

This creates a simple verification process that consumers can perform using their smartphones.

If duplicate scans or suspicious activity occurs, the system can flag potential counterfeit distribution.

Supporting Transparency in Sustainable FMCG Supply Chains

Consumers who choose refillable products are often highly conscious about sustainability and brand ethics.

These consumers value transparency regarding product origin, formulation quality, and environmental impact.

Authentication technologies allow brands to provide this transparency through digital engagement.

When consumers scan refill packaging, brands can share information such as:

  • Product authenticity confirmation
  • Sustainability commitments
  • Responsible sourcing practices
  • Product usage guidance
This interaction strengthens consumer trust while reinforcing the brand’s sustainability messaging.

Why Sustainability and Security Must Work Together

Sustainability innovations should not compromise product security.

If refill systems are vulnerable to counterfeit infiltration, the consequences can include:

  • Consumer safety concerns
  • Product performance failures
  • Damage to brand credibility
  • Loss of consumer trust in refill systems

Therefore, packaging innovators and sustainability leaders must design refillable packaging systems that balance environmental responsibility with authentication security.

Integrating anti-counterfeit technologies ensures that refillable models remain safe, reliable, and trustworthy.

How Lasersec Technologies Supports Secure Refillable Packaging

At Lasersec Technologies, we help FMCG brands integrate authentication and anti-counterfeit protection into modern packaging systems.

Our solutions combine secure holographic labels, QR-based authentication, tamper-evident packaging features, and Track & Trace systems to protect products across evolving packaging formats.

These technologies help FMCG brands:

  • Prevent counterfeit refill products
  • Protect reusable container ecosystems
  • Enable consumer-level product authentication
  • Strengthen supply chain visibility
  • Support sustainable packaging strategies without compromising security

By integrating smart authentication technologies into refill packaging, brands can maintain both environmental responsibility and product integrity.

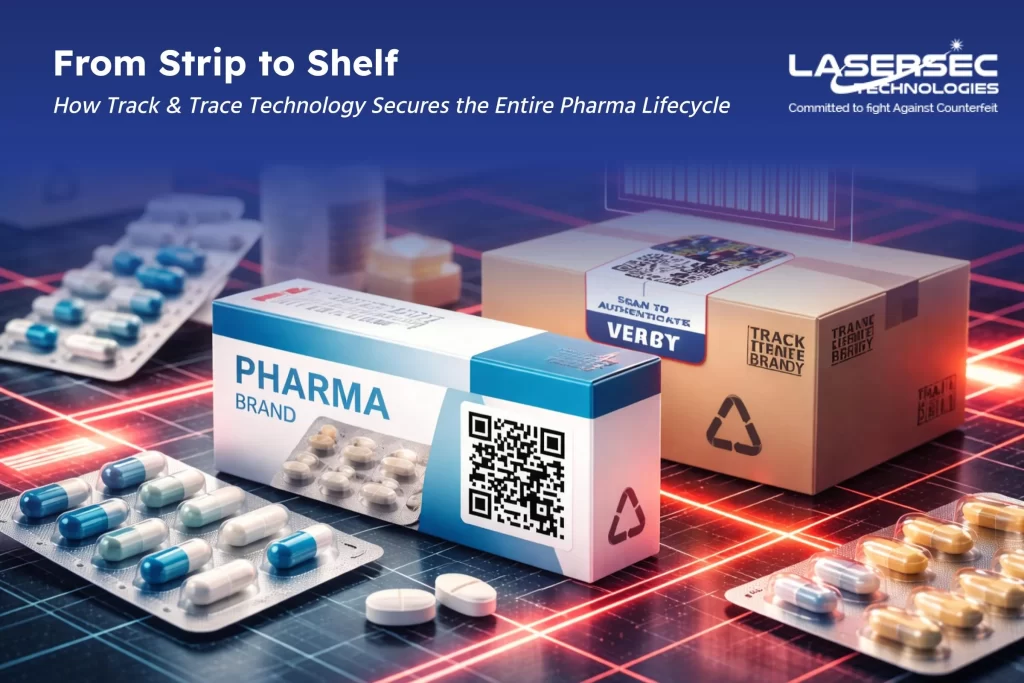
Track and trace technology across pharma supply chain lifecycle

A pharmaceutical product begins its journey inside a controlled manufacturing environment where every process is carefully monitored.

The formulation is verified, production batches are documented, and packaging operations follow strict regulatory protocols. Once the medicine is packaged, it begins moving through warehouses, distributors, logistics partners, pharmacies, and healthcare facilities before reaching patients.

However, the moment a product leaves the manufacturing facility, visibility often becomes limited.

Without strong traceability systems, pharmaceutical companies may struggle to monitor product movement across global supply chains. This lack of visibility creates opportunities for counterfeit infiltration, product diversion, and unauthorized distribution.

To address these risks, pharmaceutical manufacturers are increasingly adopting Track & Trace technology combined with secure packaging solutions.

By integrating serialization, tamper-evident packaging, and digital product identities, Track & Trace systems enable manufacturers to secure the pharmaceutical life cycle—from the packaging strip to the pharmacy shelf.

Why End-to-End Traceability Is Critical in Modern Pharmaceutical Supply Chains

The pharmaceutical supply chain is one of the most complex and tightly regulated supply networks in the world.

Medicines often move across multiple countries and pass through various intermediaries including:

  • Manufacturing facilities
  • Packaging lines
  • Distribution warehouses
  • Export and import channels
  • Regional distributors
  • Pharmacies and healthcare providers

At each stage, the product may face risks such as:

  • Counterfeit drug infiltration
  • Unauthorized parallel trade
  • Repackaging or relabeling
  • Diversion to unapproved markets

Without reliable traceability systems, identifying where a product originated or how it entered a specific market becomes extremely difficult.

This is why global regulatory frameworks increasingly require serialization and Track & Trace systems that allow medicines to be tracked throughout their life cycle.

The Limitations of Traditional Pharmaceutical Packaging

Traditional pharmaceutical packaging primarily focuses on protecting the product from environmental exposure such as moisture, contamination, or physical damage.

While this is essential for product stability, conventional packaging alone cannot provide full supply chain visibility.

Standard packaging elements such as:

  • Printed batch numbers
  • bar codes
  • Product labeling
  • Packaging artwork

are designed for identification and logistics rather than authentication and traceability.

These elements can be copied or replicated by counterfeiters, making it difficult to confirm product authenticity based solely on visual inspection.

To secure modern pharmaceutical supply chains, packaging must evolve beyond protection and become a source of verifiable product identity.

What Is Track & Trace Technology in Pharmaceutical Packaging

Track & Trace technology enables pharmaceutical manufacturers to assign a unique digital identity to every product unit.

This identity is typically created through serialization during the packaging process.

Serialized identifiers may include:

  • Unique QR codes
  • Data Matrix codes
  • Alphanumeric product identifiers

Each code is linked to a secure database containing product information such as:

  • Manufacturing origin
  • Batch and production details
  • Packaging line information
  • Distribution records
Every time the product moves through the supply chain and the code is scanned, the system records a verification event. This creates a transparent history of the product’s movement from production to final delivery.

From Strip to Shelf: How Track & Trace Secures Each Stage of the life cycle

Track & Trace systems secure the pharmaceutical life cycle by providing visibility at every stage of product movement.

The process begins during primary packaging, such as blister strips or strip foils, where serialization codes may be applied or linked to the packaging unit.

During secondary packaging, serialized codes are integrated into cartons or labels that carry the product identity.

At this stage, tamper-evident packaging features are often added to ensure that the product cannot be opened or altered without detection.

As the product moves through warehouses and distribution channels, each scan event confirms that the product remains authentic and within authorized supply networks.

By the time the medicine reaches pharmacies or healthcare providers, its complete traceability record can be verified through the Track & Trace system.

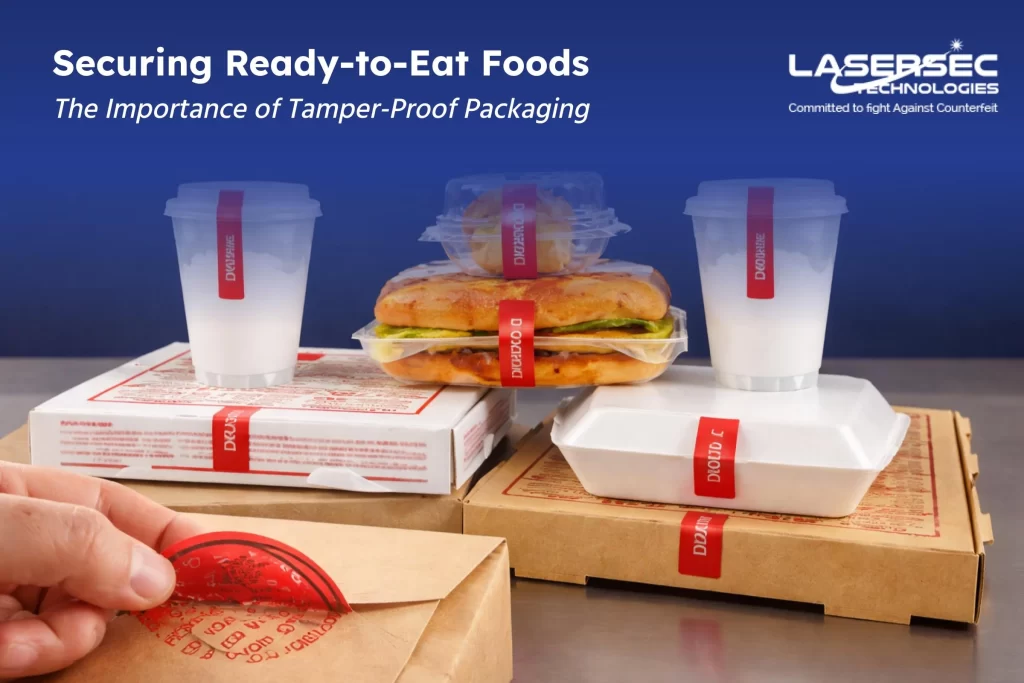
The Role of Tamper-Evident Packaging in life cycle Security

While Track & Trace technology provides digital visibility, tamper-evident packaging ensures physical product integrity.

Tamper-evident features reveal if packaging has been opened, altered, or manipulated after leaving the manufacturing facility.

These features may include:

If tampering occurs, the packaging clearly indicates interference, allowing distributors and regulators to identify compromised products quickly.

When combined with serialization, tamper-evident packaging provides both physical protection and digital verification.

Understanding the Role of Digital Twins in Pharmaceutical Traceability

A key concept in modern Track & Trace systems is the creation of a digital twin for each pharmaceutical product unit.

A digital twin is a digital representation of a physical product that exists within a secure data environment.

When a serialized product is packaged, its digital twin is created within the authentication platform.

This digital identity contains important information including:

  • Manufacturing records
  • Packaging data
  • Supply chain verification history
  • Product authentication status

Whenever the product code is scanned, the system verifies whether the physical product matches its digital twin.

If discrepancies appear—such as duplicate codes or scans in unauthorized regions—the system immediately flags potential counterfeit activity. This allows manufacturers to detect risks early and respond quickly.

Strengthening Regulatory Compliance with Track & Trace Systems

Regulatory agencies around the world are increasingly requiring pharmaceutical companies to implement traceability systems.

These requirements are designed to improve transparency, prevent counterfeit drugs, and protect patient safety.

Track & Trace systems help manufacturers meet these regulatory expectations by enabling:

  • Unit-level serialization
  • Supply chain verification
  • Product authentication
  • Rapid recall management
  • Distribution monitoring
When regulators or inspectors need to verify a product’s origin or authenticity, the system can provide instant verification data. This strengthens regulatory confidence and reduces compliance risks.

Why Pharmaceutical Manufacturers Are Upgrading to End-to-End Traceability

Pharmaceutical manufacturers are increasingly moving toward integrated packaging and traceability systems rather than relying on isolated security measures.

End-to-end Track & Trace systems provide several strategic benefits:

  • Strong protection against counterfeit drug infiltration
  • Real-time visibility across supply chains
  • Faster identification of unauthorized distribution
  • Improved recall management capabilities
  • Stronger compliance with global regulatory requirements
By combining serialization, tamper-evident packaging, and authentication systems, manufacturers can secure their products throughout the entire life cycle.

How Lasersec Technologies Supports End-to-End Pharmaceutical Security

At Lasersec Technologies, we provide integrated pharmaceutical packaging and authentication solutions designed to support end-to-end product security.

Our technologies combine secure packaging features, serialization-ready labeling, holographic authentication elements, and Track & Trace systems to create a comprehensive pharmaceutical protection framework.

These solutions help pharmaceutical manufacturers:

  • Implement reliable product serialization
  • Protect packaging through tamper-evident technologies
  • Enable secure authentication through QR-based verification
  • Improve supply chain monitoring
  • Strengthen regulatory compliance and brand protection

By integrating physical packaging security with digital traceability systems, we help pharmaceutical companies maintain full control over their products from manufacturing to patient delivery.