Lasersec Technologies

Track and trace technology across pharma supply chain lifecycle

A pharmaceutical product begins its journey inside a controlled manufacturing environment where every process is carefully monitored.

The formulation is verified, production batches are documented, and packaging operations follow strict regulatory protocols. Once the medicine is packaged, it begins moving through warehouses, distributors, logistics partners, pharmacies, and healthcare facilities before reaching patients.

However, the moment a product leaves the manufacturing facility, visibility often becomes limited.

Without strong traceability systems, pharmaceutical companies may struggle to monitor product movement across global supply chains. This lack of visibility creates opportunities for counterfeit infiltration, product diversion, and unauthorized distribution.

To address these risks, pharmaceutical manufacturers are increasingly adopting Track & Trace technology combined with secure packaging solutions.

By integrating serialization, tamper-evident packaging, and digital product identities, Track & Trace systems enable manufacturers to secure the pharmaceutical life cycle—from the packaging strip to the pharmacy shelf.

Why End-to-End Traceability Is Critical in Modern Pharmaceutical Supply Chains

The pharmaceutical supply chain is one of the most complex and tightly regulated supply networks in the world.

Medicines often move across multiple countries and pass through various intermediaries including:

  • Manufacturing facilities
  • Packaging lines
  • Distribution warehouses
  • Export and import channels
  • Regional distributors
  • Pharmacies and healthcare providers

At each stage, the product may face risks such as:

  • Counterfeit drug infiltration
  • Unauthorized parallel trade
  • Repackaging or relabeling
  • Diversion to unapproved markets

Without reliable traceability systems, identifying where a product originated or how it entered a specific market becomes extremely difficult.

This is why global regulatory frameworks increasingly require serialization and Track & Trace systems that allow medicines to be tracked throughout their life cycle.

The Limitations of Traditional Pharmaceutical Packaging

Traditional pharmaceutical packaging primarily focuses on protecting the product from environmental exposure such as moisture, contamination, or physical damage.

While this is essential for product stability, conventional packaging alone cannot provide full supply chain visibility.

Standard packaging elements such as:

  • Printed batch numbers
  • bar codes
  • Product labeling
  • Packaging artwork

are designed for identification and logistics rather than authentication and traceability.

These elements can be copied or replicated by counterfeiters, making it difficult to confirm product authenticity based solely on visual inspection.

To secure modern pharmaceutical supply chains, packaging must evolve beyond protection and become a source of verifiable product identity.

What Is Track & Trace Technology in Pharmaceutical Packaging

Track & Trace technology enables pharmaceutical manufacturers to assign a unique digital identity to every product unit.

This identity is typically created through serialization during the packaging process.

Serialized identifiers may include:

  • Unique QR codes
  • Data Matrix codes
  • Alphanumeric product identifiers

Each code is linked to a secure database containing product information such as:

  • Manufacturing origin
  • Batch and production details
  • Packaging line information
  • Distribution records
Every time the product moves through the supply chain and the code is scanned, the system records a verification event. This creates a transparent history of the product’s movement from production to final delivery.

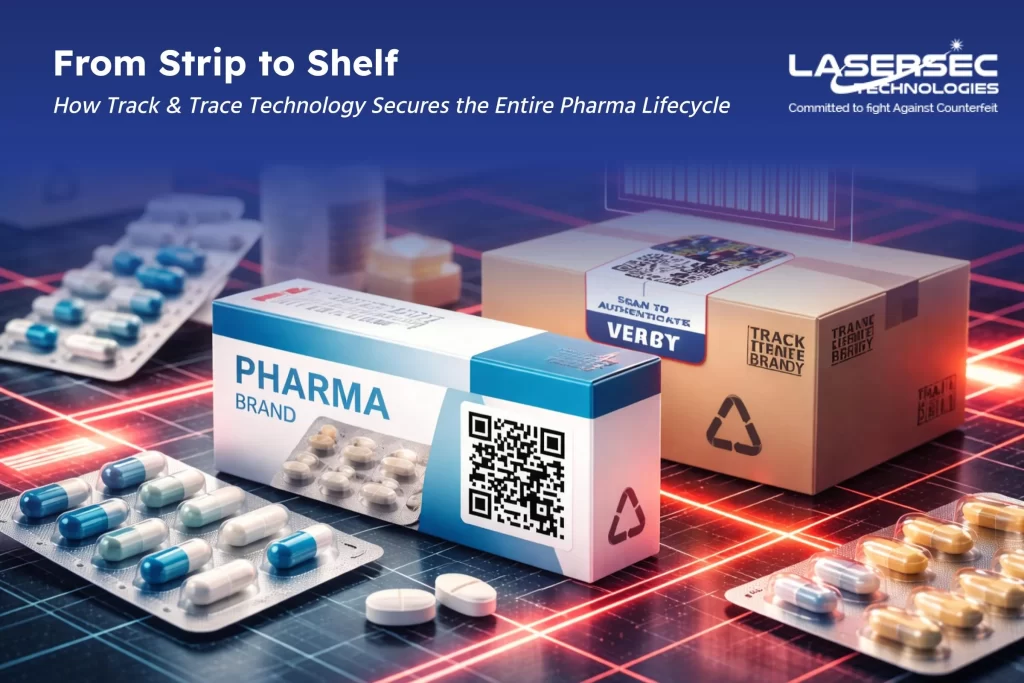
From Strip to Shelf: How Track & Trace Secures Each Stage of the life cycle

Track & Trace systems secure the pharmaceutical life cycle by providing visibility at every stage of product movement.

The process begins during primary packaging, such as blister strips or strip foils, where serialization codes may be applied or linked to the packaging unit.

During secondary packaging, serialized codes are integrated into cartons or labels that carry the product identity.

At this stage, tamper-evident packaging features are often added to ensure that the product cannot be opened or altered without detection.

As the product moves through warehouses and distribution channels, each scan event confirms that the product remains authentic and within authorized supply networks.

By the time the medicine reaches pharmacies or healthcare providers, its complete traceability record can be verified through the Track & Trace system.

The Role of Tamper-Evident Packaging in life cycle Security

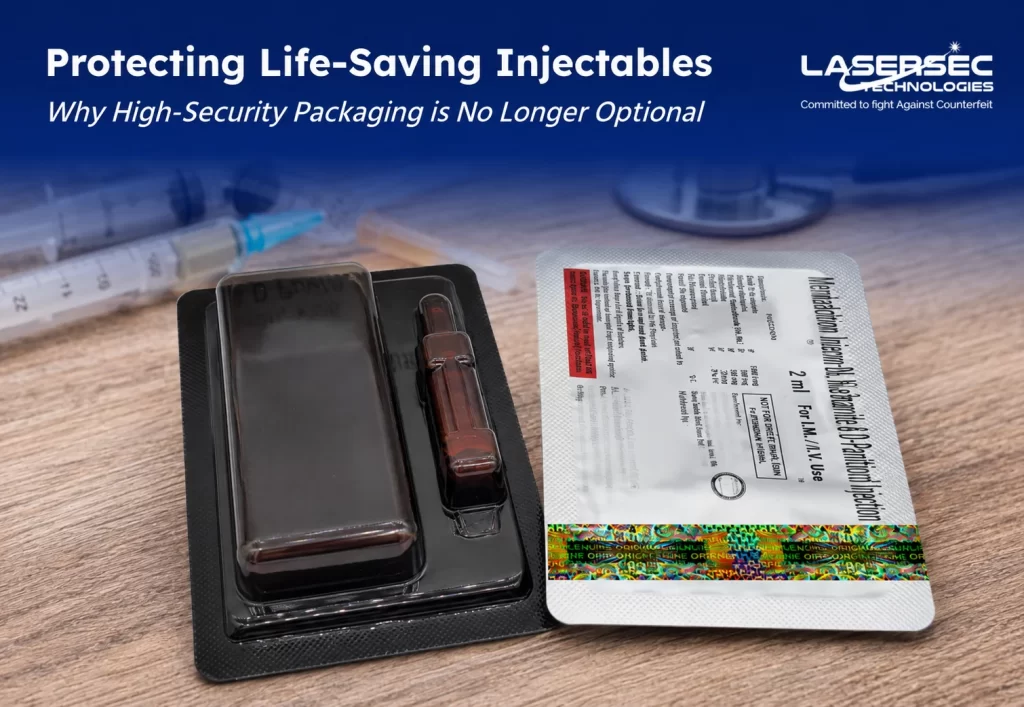
While Track & Trace technology provides digital visibility, tamper-evident packaging ensures physical product integrity.

Tamper-evident features reveal if packaging has been opened, altered, or manipulated after leaving the manufacturing facility.

These features may include:

If tampering occurs, the packaging clearly indicates interference, allowing distributors and regulators to identify compromised products quickly.

When combined with serialization, tamper-evident packaging provides both physical protection and digital verification.

Understanding the Role of Digital Twins in Pharmaceutical Traceability

A key concept in modern Track & Trace systems is the creation of a digital twin for each pharmaceutical product unit.

A digital twin is a digital representation of a physical product that exists within a secure data environment.

When a serialized product is packaged, its digital twin is created within the authentication platform.

This digital identity contains important information including:

  • Manufacturing records
  • Packaging data
  • Supply chain verification history
  • Product authentication status

Whenever the product code is scanned, the system verifies whether the physical product matches its digital twin.

If discrepancies appear—such as duplicate codes or scans in unauthorized regions—the system immediately flags potential counterfeit activity. This allows manufacturers to detect risks early and respond quickly.

Strengthening Regulatory Compliance with Track & Trace Systems

Regulatory agencies around the world are increasingly requiring pharmaceutical companies to implement traceability systems.

These requirements are designed to improve transparency, prevent counterfeit drugs, and protect patient safety.

Track & Trace systems help manufacturers meet these regulatory expectations by enabling:

  • Unit-level serialization
  • Supply chain verification
  • Product authentication
  • Rapid recall management
  • Distribution monitoring
When regulators or inspectors need to verify a product’s origin or authenticity, the system can provide instant verification data. This strengthens regulatory confidence and reduces compliance risks.

Why Pharmaceutical Manufacturers Are Upgrading to End-to-End Traceability

Pharmaceutical manufacturers are increasingly moving toward integrated packaging and traceability systems rather than relying on isolated security measures.

End-to-end Track & Trace systems provide several strategic benefits:

  • Strong protection against counterfeit drug infiltration
  • Real-time visibility across supply chains
  • Faster identification of unauthorized distribution
  • Improved recall management capabilities
  • Stronger compliance with global regulatory requirements
By combining serialization, tamper-evident packaging, and authentication systems, manufacturers can secure their products throughout the entire life cycle.

How Lasersec Technologies Supports End-to-End Pharmaceutical Security

At Lasersec Technologies, we provide integrated pharmaceutical packaging and authentication solutions designed to support end-to-end product security.

Our technologies combine secure packaging features, serialization-ready labeling, holographic authentication elements, and Track & Trace systems to create a comprehensive pharmaceutical protection framework.

These solutions help pharmaceutical manufacturers:

  • Implement reliable product serialization
  • Protect packaging through tamper-evident technologies
  • Enable secure authentication through QR-based verification
  • Improve supply chain monitoring
  • Strengthen regulatory compliance and brand protection

By integrating physical packaging security with digital traceability systems, we help pharmaceutical companies maintain full control over their products from manufacturing to patient delivery.
Share :

Frequently Asked Questions

Track & Trace technology assigns a unique identity to each product and records its movement throughout the supply chain. This enables manufacturers to monitor distribution, verify authenticity, detect suspicious activity, and respond quickly to potential counterfeiting or diversion incidents. Explore our Track & Trace Technology to see how it supports end-to-end pharmaceutical security, and learn how phygital packaging stops counterfeit medicines by combining digital verification with physical authentication.

Serialization gives every medicine pack a unique identifier that can be verified throughout its lifecycle. This improves product traceability, supports regulatory compliance, and helps identify counterfeit or duplicated products before they reach patients. Discover how smart label technology meets EU serialization and compliance requirements and how best practices for pharmaceutical anti-counterfeiting combine serialization with QR Code Authentication and Track & Trace to strengthen supply chain transparency and brand protection.

Tamper-evident packaging protects the physical integrity of a product by revealing signs of interference, while Track & Trace technology provides digital visibility into its journey across the supply chain. Together, they create a layered security approach that helps pharmaceutical companies detect tampering, authenticate products, and reduce supply chain risks. See exactly how tamper-evident packaging and Track & Trace strengthen anti-counterfeiting measures and learn how to ensure regulatory compliance with tamper-evident packaging for integrated protection.

Yes. End-to-end traceability can reduce counterfeit risks, improve recall management, strengthen regulatory compliance, and provide greater visibility into product movement. It also helps protect patient safety and reinforces trust in pharmaceutical brands. Explore how building a multi-layered anti-counterfeit strategy for pharma exports maximizes the value of Track & Trace investment, and see how pairing it with Security Holograms creates a comprehensive authentication system.

An effective Track & Trace solution should support serialization, real-time product verification, secure data management, tamper-evident packaging integration, and scalability across global supply chains. It should also enable rapid authentication and compliance with evolving regulations. Explore our Track & Trace Technology and QR Code Authentication solutions, and discover how holographic Alu-Alu foil with serialization delivers compliance-ready traceability to build a comprehensive pharmaceutical protection strategy.

Related Blogs

Traceable labels improving fashion supply chain transparency

In today’s apparel industry, transparency is no longer optional. Customers expect to know where their garments come from, how materials were sourced, and whether the brand operates responsibly. Export buyers demand even more — they require verified proof, backed by data, not claims.

This shift has pushed apparel manufacturers to strengthen supply chain visibility. Among all available tools, traceable labels have emerged as one of the most effective ways to build trust, ensure compliance, and protect brand authenticity. They are now becoming a core requirement across global fashion supply chains.

You can explore a detailed overview of these solutions in our apparel anti-counterfeit and traceability solutions section.

Why the Apparel Industry Needs Stronger Transparency

The fashion supply chain moves through multiple factories, vendors, dyeing units, finishing plants, and regions. With so many touchpoints, information becomes scattered — creating challenges such as:

  • Buyers requiring verified sourcing and production details
  • Consumers demanding clarity before trusting brands
  • Sustainability teams needing accurate reporting data
  • Export shipments requiring strict traceability documentation
  • Counterfeit garments entering the market and diluting brand value

When information is difficult to verify, trust is lost even before the product is evaluated.

What Traceable Labels Actually Do

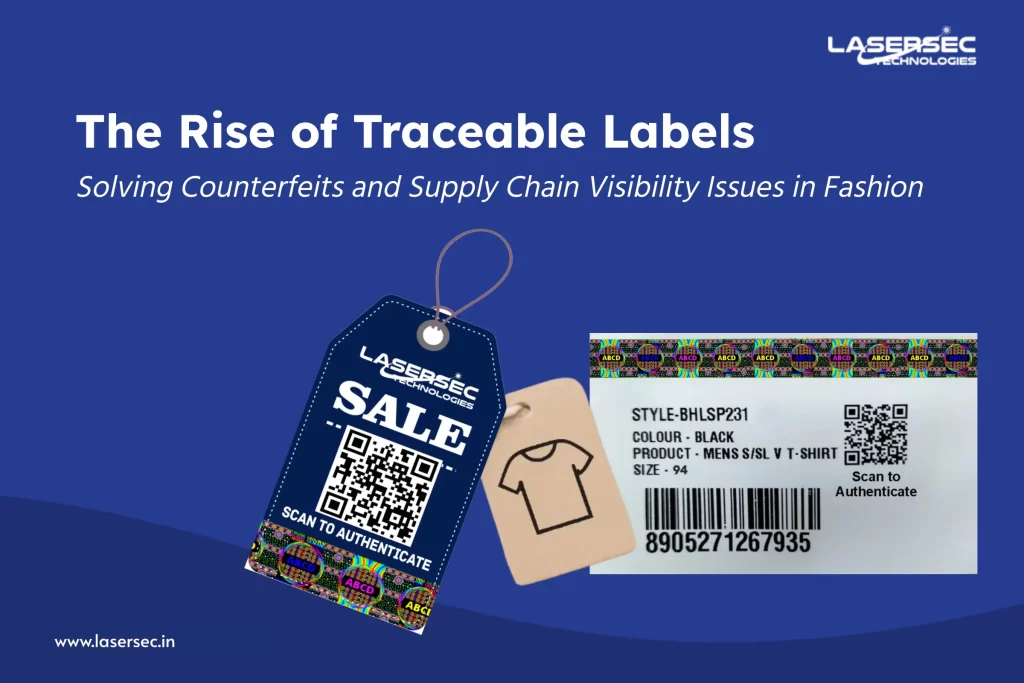
Traceable apparel labels give customers, buyers, auditors, and compliance teams instant access to reliable information.

With a single scan, they can view:

  • Sourcing origin of the garment
  • Material composition and sustainability data
  • End-to-end journey from factory to store
  • Processing and manufacturing checkpoints
  • Care instructions, ethics, and certifications
  • Authenticity verification to stop counterfeits

In seconds, the garment becomes a transparent digital product passport — simple for brands, reassuring for buyers, and reliable for audits. Learn more about the technology behind this in our Track & Trace systems.

How Traceable Labels Strengthen Your Brand

1. They Build Instant Trust

Clear, verified, and accessible information increases customer confidence and loyalty.

2. They Protect Against Counterfeits

Fast fashion and export markets face high imitation risks. One scan verifies authenticity instantly. Explore the solutions used for this in our anti-counterfeit product gallery.

3. They Help You Win Export Orders

EU and global buyers expect traceability, documentation, and proof of responsible sourcing. Verified labeling helps your products stand out.

4. They Make Sustainability Measurable

Traceability allows brands to back sustainability claims with data — improving credibility.

5. They Reduce Audit Delays

All manufacturing and sourcing information is digitized, making buyer inspections faster and smoother.

A Moment Every Apparel Team Will Recognize

A European buyer asks your production team:

“Can you provide the complete sourcing journey of this garment?”

Your team searches through emails, spreadsheets, and vendor files.

Now imagine a different scenario:

The buyer scans the label — the entire journey appears instantly, verified and timestamped.

That is the efficiency of a traceable apparel supply chain.
No confusion. No delays. No gaps.

Why This Matters to Today’s Apparel Professionals

If you are an apparel manufacturer, sustainability officer, export merchandiser, or compliance lead, you know the landscape is changing:

  • Buyers are stricter than ever
  • Sustainability claims must be data-backed
  • Export errors can result in cancelled orders
  • Customers prefer responsible, ethical brands
  • Transparency now improves trust more than pricing

Traceable labels help you meet these demands while reducing errors across the supply chain. For deeper guidance, explore our apparel compliance and traceability resources.

How Lasersec Technologies Helps You Deliver True Transparency

We support apparel brands with ready-to-deploy traceability and anti-counterfeit solutions built for real manufacturing conditions. Our systems are simple to adopt, scalable across factories, and aligned with global compliance demands.

We offer:

  • Traceable labels with instant scan-based information
  • Anti-counterfeit garment tags
  • QR-enabled fabric and apparel tracking
  • Digital product journeys for full supply chain visibility
  • Authenticity verification tools
  • Sustainable material tagging systems

These solutions help brands present their true story — clearly, responsibly, and confidently — whether the focus is export, premium retail, or sustainable fashion.

With us, you can deliver the transparency your buyers expect today and stay ready for the global standards of tomorrow. Explore how these work:

Our goal is to help you present your brand’s true story clearly, responsibly, and confidently — whether you’re targeting exports, premium retail, or sustainable fashion.

With us, you can deliver the transparency your buyers expect today and stay fully prepared for the global standards of tomorrow.

For project discussions, feel free to contact our team or visit our FAQ section for more clarity.

tamper-proof-food-packaging

Ready-to-eat (RTE) foods have become a major part of modern consumer lifestyles.

From packaged meals and frozen foods to ready-to-cook snacks and convenience products, consumers increasingly rely on packaged food that can be consumed quickly with minimal preparation.

However, as the demand for convenience foods grows, so does the importance of ensuring packaging safety and integrity.

Unlike traditional packaged goods, ready-to-eat products are consumed directly by consumers. Any tampering with the packaging can pose immediate health risks.

For food manufacturers and FMCG brands, ensuring that packaging clearly shows any sign of interference has become a critical safety requirement.

This is where tamper-proof packaging solutions such as security seals, tear bands, and tamper-evident labels play a vital role in protecting both consumers and brand reputation.

Why Ready-to-Eat Foods Require Strong Packaging Protection

Ready-to-eat foods move through complex distribution networks before reaching consumers.

Products may pass through multiple stages including manufacturing plants, cold storage facilities, transport hubs, retail stores, and delivery services.

At each stage, the product may be handled by several intermediaries.

Without proper tamper-evident protection, it can be difficult to determine whether a food package has been opened or compromised during distribution.

Even minor tampering can create serious risks such as:

  • Food contamination
  • Product spoilage
  • Loss of product freshness
  • Consumer health hazards
  • Brand reputation damage

For products that are meant to be consumed immediately, packaging integrity becomes one of the most important safety indicators.

The Rising Risk of Food Tampering in Modern Supply Chains

Food tampering incidents, although rare, can have severe consequences for both consumers and brands.

In the case of ready-to-eat products, tampering may involve:

  • Opening packaging and resealing it
  • Altering or contaminating food contents
  • Replacing products with lower-quality alternatives
  • Damaging protective seals during handling

Because ready-to-eat foods often rely on sealed packaging to maintain hygiene and freshness, any compromise in packaging integrity can undermine product safety.

For FMCG companies, preventing tampering is therefore not just a packaging concern but a food safety priority.

Key Tamper-Proof Packaging Solutions for Ready-to-Eat Foods

Modern food packaging uses several mechanisms to provide clear visual evidence of tampering.

These solutions help consumers, retailers, and inspectors easily identify whether a package has been opened or altered.

Some of the most widely used tamper-evident packaging features include:

Security Seals

Security seals are applied to food packaging to ensure that the product remains unopened until it reaches the consumer.

Once broken, the seal cannot be restored to its original state.

Security seals are commonly used for:

  • Meal trays
  • Frozen food containers
  • Jar lids
  • Beverage caps
  • Food cartons

Tear Bands and Breakable Rings

Tear bands are thin strips integrated into packaging that must be removed before opening the product.

These bands break permanently when opened, providing immediate visual evidence that the package has been accessed.

They are frequently used in:

  • Frozen food containers
  • Bottled sauces
  • Packaged beverages
  • Sealed food jars

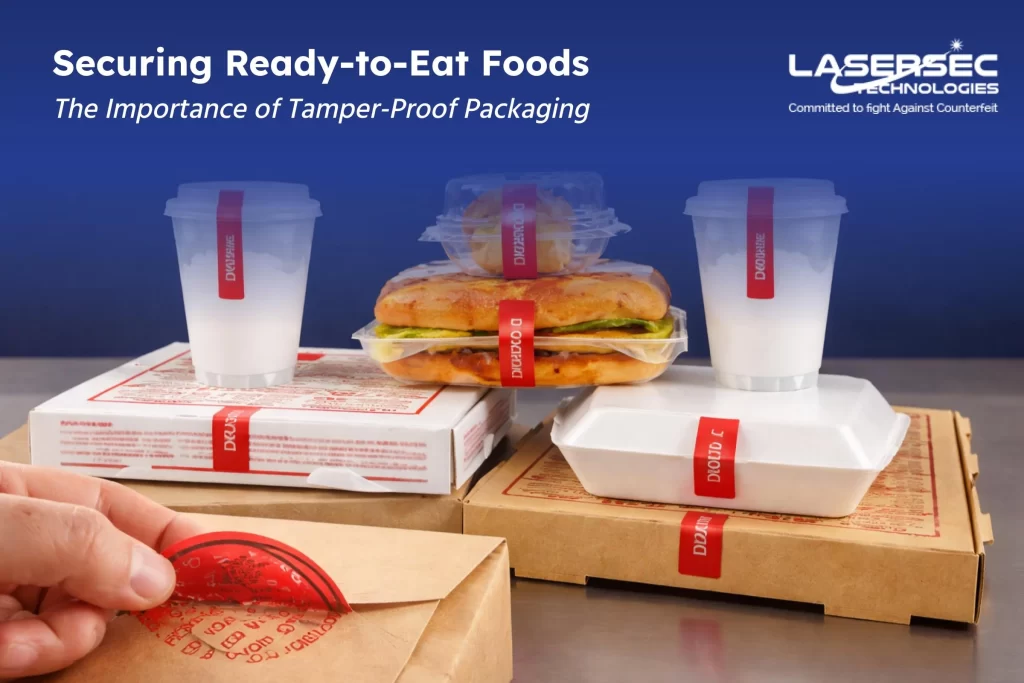
Tamper-Evident Labels

Tamper-evident labels provide additional protection by revealing any attempt to remove or reposition the label.

These labels may include features such as:

  • Destructible material that breaks when peeled
  • Security patterns that appear when tampered with
  • Adhesive residues that indicate interference

Because these labels cannot be reapplied cleanly, they help ensure packaging authenticity.

Visual Tamper Evidence: Why It Matters to Consumers

One of the most important aspects of food packaging security is visible assurance.

Consumers often rely on simple visual cues to determine whether a product is safe to consume.

If packaging appears compromised or damaged, consumers are far less likely to purchase the product.

Clear visual tamper indicators help consumers quickly confirm that:

  • The product has not been opened
  • The packaging seal remains intact
  • The food has not been altered

This visible reassurance plays a major role in building trust between FMCG brands and consumers.

Protecting Brand Reputation in the FMCG Industry

Food brands operate in an environment where consumer trust is extremely sensitive.

A single incident involving contaminated or tampered food products can lead to:

  • Product recalls
  • Negative media coverage
  • Regulatory investigations
  • Long-term brand damage

Tamper-proof packaging acts as a preventive safeguard by ensuring that any attempt to interfere with the product becomes immediately visible.

For FMCG companies, this protection is essential for maintaining brand credibility in competitive retail markets.

Supporting Food Safety Compliance

Food safety regulations around the world increasingly emphasize the importance of packaging integrity.

Regulatory authorities expect manufacturers to implement packaging systems that protect food products from contamination and unauthorized access.

Tamper-evident packaging helps manufacturers meet these expectations by:

  • Demonstrating proactive food safety measures
  • Strengthening quality assurance processes
  • Supporting regulatory compliance during inspections
  • Providing traceable evidence of packaging integrity

For companies operating across international markets, these safeguards are especially important.

The Role of Advanced Packaging Technologies

As food supply chains grow more complex, many FMCG brands are integrating advanced technologies into their packaging systems.

These may include:

When combined with physical tamper-evident features, these technologies provide both physical and digital protection for food products.

How Lasersec Technologies Helps Secure FMCG Packaging

Lasersec Technologies develops advanced packaging security solutions designed to protect FMCG products from tampering and unauthorized interference.

Our solutions integrate tamper-evident labels, security seals, and authentication technologies that help ensure product safety throughout the supply chain.

These solutions help FMCG brands:

  • Protect ready-to-eat and frozen food packaging
  • Prevent unauthorized opening or resealing
  • Provide visible tamper evidence for consumers
  • Strengthen food safety compliance
  • Safeguard brand reputation in competitive markets

By integrating security directly into packaging, food manufacturers can maintain product integrity from production to consumption.