We're leading manufacturer of anti-counterfeit solutions and
safeguard brands across industries with cutting-edge security
solutions that prevent counterfeiting and ensure product
authenticity.
In today’s apparel industry, transparency is no longer optional. Customers expect to know where their garments come from, how materials were sourced, and whether the brand operates responsibly. Export buyers demand even more — they require verified proof, backed by data, not claims.
This shift has pushed apparel manufacturers to strengthen supply chain visibility. Among all available tools, traceable labels have emerged as one of the most effective ways to build trust, ensure compliance, and protect brand authenticity. They are now becoming a core requirement across global fashion supply chains.
Why the Apparel Industry Needs Stronger Transparency
The fashion supply chain moves through multiple factories, vendors, dyeing units, finishing plants, and regions. With so many touchpoints, information becomes scattered — creating challenges such as:
Buyers requiring verified sourcing and production details
Consumers demanding clarity before trusting brands
Sustainability teams needing accurate reporting data
Counterfeit garments entering the market and diluting brand value
When information is difficult to verify, trust is lost even before the product is evaluated.
What Traceable Labels Actually Do
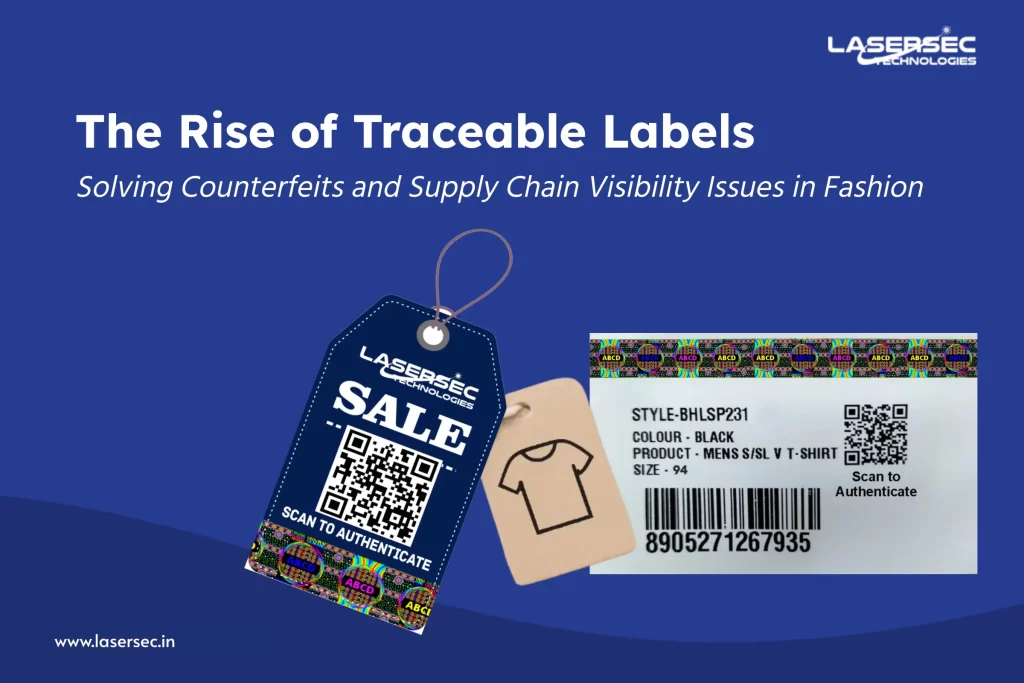
Traceable apparel labels give customers, buyers, auditors, and compliance teams instant access to reliable information.
With a single scan, they can view:
Sourcing origin of the garment
Material composition and sustainability data
End-to-end journey from factory to store
Processing and manufacturing checkpoints
Care instructions, ethics, and certifications
Authenticity verification to stop counterfeits
In seconds, the garment becomes a transparent digital product passport — simple for brands, reassuring for buyers, and reliable for audits. Learn more about the technology behind this in our Track & Trace systems.
How Traceable Labels Strengthen Your Brand
1. They Build Instant Trust
Clear, verified, and accessible information increases customer confidence and loyalty.
2. They Protect Against Counterfeits
Fast fashion and export markets face high imitation risks. One scan verifies authenticity instantly. Explore the solutions used for this in our anti-counterfeit product gallery.
3. They Help You Win Export Orders
EU and global buyers expect traceability, documentation, and proof of responsible sourcing. Verified labeling helps your products stand out.
4. They Make Sustainability Measurable
Traceability allows brands to back sustainability claims with data — improving credibility.
5. They Reduce Audit Delays
All manufacturing and sourcing information is digitized, making buyer inspections faster and smoother.
A Moment Every Apparel Team Will Recognize
A European buyer asks your production team:
“Can you provide the complete sourcing journey of this garment?”
Your team searches through emails, spreadsheets, and vendor files.
Now imagine a different scenario:
The buyer scans the label — the entire journey appears instantly, verified and timestamped.
That is the efficiency of a traceable apparel supply chain. No confusion. No delays. No gaps.
Why This Matters to Today’s Apparel Professionals
If you are an apparel manufacturer, sustainability officer, export merchandiser, or compliance lead, you know the landscape is changing:
How Lasersec Technologies Helps You Deliver True Transparency
We support apparel brands with ready-to-deploy traceability and anti-counterfeit solutions built for real manufacturing conditions. Our systems are simple to adopt, scalable across factories, and aligned with global compliance demands.
We offer:
Traceable labels with instant scan-based information
Anti-counterfeit garment tags
QR-enabled fabric and apparel tracking
Digital product journeys for full supply chain visibility
Authenticity verification tools
Sustainable material tagging systems
These solutions help brands present their true story — clearly, responsibly, and confidently — whether the focus is export, premium retail, or sustainable fashion.
With us, you can deliver the transparency your buyers expect today and stay ready for the global standards of tomorrow. Explore how these work:
Our goal is to help you present your brand’s true story clearly, responsibly, and confidently — whether you’re targeting exports, premium retail, or sustainable fashion.
With us, you can deliver the transparency your buyers expect today and stay fully prepared for the global standards of tomorrow.
What are traceable labels, and why are they important for the apparel industry?
Traceable labels connect physical garments with digital information, enabling brands, buyers, and consumers to verify sourcing, manufacturing, authenticity, and product history through a simple scan. They improve supply chain transparency, support compliance efforts, and help build trust in increasingly competitive global markets. Discover howholographic tags with QR codes help apparel manufacturers trace products from production to purchase and explore ourApparel Industry Anti-Counterfeit Solutions including Track & Trace Technology and apparel traceability solutions.
How do traceable labels help prevent counterfeit apparel products?
Can traceable labels improve export compliance and buyer confidence?
Yes. International buyers increasingly expect transparent documentation and verifiable sourcing information. Traceable labels provide instant access to manufacturing and supply chain data, making audits, compliance checks, and buyer verification more efficient while strengthening confidence in your products. See howQR-based authentication strengthens brand protection across global supply chains, and learn how pairing traceable labels with ourTrack & Trace Technology can further enhance end-to-end visibility for export-ready apparel brands.
Are traceable labels worth investing in for fashion and apparel brands?
For many brands, traceable labels deliver value beyond anti-counterfeiting by supporting sustainability initiatives, improving supply chain visibility, reducing manual documentation, and enhancing customer trust. They also help brands demonstrate responsible sourcing with verifiable data. Read howrecognizing fake apparel and building brand trust drives the case for investment, and explore how integratingQR Code Authentication andTrack & Trace Technology creates a scalable foundation for long-term transparency.
What should apparel manufacturers look for in a traceability solution?
An effective traceability solution should provide unique product identification, secure QR-based verification, end-to-end supply chain visibility, scalability across manufacturing operations, and support for sustainability and compliance initiatives. Explore ourApparel Industry Anti-Counterfeit Solutions andHolographic Cloth Tags, and see howthe future of anti-counterfeit solutions for apparel manufacturers combines Track & Trace Technology, QR Code Authentication, and holographic security to protect authenticity while delivering greater transparency to buyers and consumers.
Frequently Asked Questions
What are traceable labels, and why are they important for the apparel industry?
Traceable labels connect physical garments with digital information, enabling brands, buyers, and consumers to verify sourcing, manufacturing, authenticity, and product history through a simple scan. They improve supply chain transparency, support compliance efforts, and help build trust in increasingly competitive global markets. Discover howholographic tags with QR codes help apparel manufacturers trace products from production to purchase and explore ourApparel Industry Anti-Counterfeit Solutions including Track & Trace Technology and apparel traceability solutions.
How do traceable labels help prevent counterfeit apparel products?
Can traceable labels improve export compliance and buyer confidence?
Yes. International buyers increasingly expect transparent documentation and verifiable sourcing information. Traceable labels provide instant access to manufacturing and supply chain data, making audits, compliance checks, and buyer verification more efficient while strengthening confidence in your products. See howQR-based authentication strengthens brand protection across global supply chains, and learn how pairing traceable labels with ourTrack & Trace Technology can further enhance end-to-end visibility for export-ready apparel brands.
Are traceable labels worth investing in for fashion and apparel brands?
For many brands, traceable labels deliver value beyond anti-counterfeiting by supporting sustainability initiatives, improving supply chain visibility, reducing manual documentation, and enhancing customer trust. They also help brands demonstrate responsible sourcing with verifiable data. Read howrecognizing fake apparel and building brand trust drives the case for investment, and explore how integratingQR Code Authentication andTrack & Trace Technology creates a scalable foundation for long-term transparency.
What should apparel manufacturers look for in a traceability solution?
An effective traceability solution should provide unique product identification, secure QR-based verification, end-to-end supply chain visibility, scalability across manufacturing operations, and support for sustainability and compliance initiatives. Explore ourApparel Industry Anti-Counterfeit Solutions andHolographic Cloth Tags, and see howthe future of anti-counterfeit solutions for apparel manufacturers combines Track & Trace Technology, QR Code Authentication, and holographic security to protect authenticity while delivering greater transparency to buyers and consumers.
Related Blogs
A pharmaceutical product moves through years of research, regulatory approvals, clinical validation, and strict manufacturing protocols before it reaches patients.
For critical therapeutic categories such as oncology medicines, anti-infectives, and psychotropic drugs, the stakes are even higher. These medicines are often life-saving, tightly regulated, and distributed through controlled supply chains.
Yet despite these safeguards, counterfeit drugs continue to infiltrate global pharmaceutical markets.
In many cases, counterfeit products replicate packaging so closely that visual inspection alone cannot identify the difference. A blister pack may appear genuine while the tablets inside are ineffective, contaminated, or entirely fake.
For manufacturers of high-risk medicines, this creates a serious challenge. Traditional packaging is no longer sufficient to protect products against sophisticated counterfeiting operations.
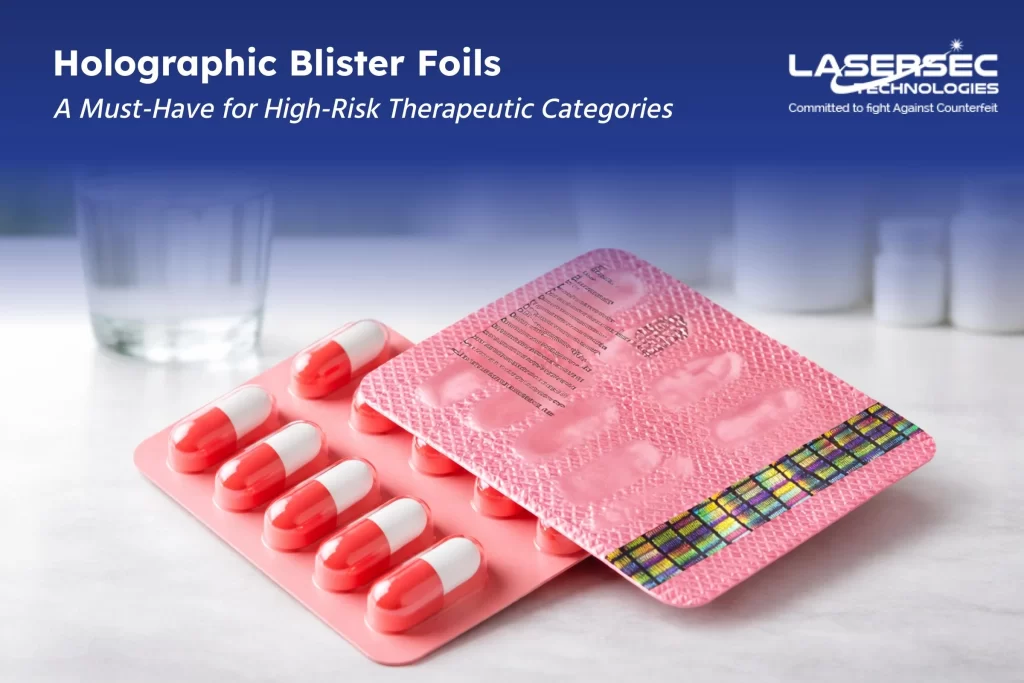
This is why holographic blister foils have emerged as a critical pharmaceutical packaging security solution. By integrating advanced holographic security directly into blister packaging, manufacturers can significantly strengthen product authentication, supply chain integrity, and patient safety.
Why High-Risk Therapeutic Categories Are Prime Targets for Counterfeit Drugs
Counterfeit pharmaceutical products do not affect all drug categories equally. Certain therapeutic segments are more vulnerable due to their high value, global demand, and critical medical importance.
These include:
Oncology drugs
Anti-infective medications such as antibiotics and antivirals
Psychotropic and controlled substances
Specialty and high-value prescription medicines
Counterfeiters often target these medicines because they command higher prices and move through complex international supply chains.
In some cases, counterfeiters attempt to replicate genuine packaging using advanced printing techniques. Without strong security features integrated into packaging, distinguishing genuine products from counterfeits becomes extremely difficult.
The consequences can be severe:
Patients receiving ineffective or dangerous treatments
Regulatory violations and recalls
Loss of trust among healthcare providers
Significant financial and reputational damage for pharmaceutical companies
For high-risk therapeutic categories, packaging security becomes an essential part of patient protection and regulatory compliance.
The Limitations of Standard Blister Packaging in Preventing Counterfeits
Blister packaging has long been a preferred format for pharmaceutical products due to its ability to protect tablets from moisture, contamination, and tampering.
However, standard blister foils without advanced security features primarily serve a protective function, not a security function.
Traditional blister packaging elements such as:
Printed foil designs
Batch numbers
Standard barcodes
Basic branding elements
can be replicated with increasing accuracy using modern printing technologies.
This allows counterfeiters to produce visually convincing packaging that can enter distribution channels unnoticed.
Even trained distributors or pharmacists may struggle to identify counterfeit products if packaging lacks secure authentication features.
As counterfeit methods become more sophisticated, pharmaceutical manufacturers require packaging solutions that provide visible, verifiable, and difficult-to-replicate security layers such as pharma holographic labels.
What Makes Holographic Blister Foils a Powerful Anti-Counterfeiting Solution
Holographic blister foils incorporate advanced optical security elements directly into pharmaceutical packaging materials.
These holographic effects are created using specialized technologies that produce complex light diffraction patterns which are extremely difficult to replicate using conventional printing methods.
Unlike standard foil designs, holographic blister foils include multi-layered security structures that provide both visual authentication and tamper resistance.
Key characteristics include:
Complex holographic patterns that cannot be easily duplicated
Dynamic visual effects visible under light movement
Secure bonding to blister packaging that reveals tampering
These features transform blister packaging from a passive protective layer into an active anti-counterfeit security system.
Healthcare professionals, distributors, and regulators can visually confirm authenticity while manufacturers benefit from stronger packaging protection.
Protecting Oncology Medicines with Secure Holographic Blister Foils
Oncology drugs represent one of the most critical and valuable pharmaceutical segments globally.
These medicines are often expensive, lifesaving, and distributed across multiple international markets. Their high value makes them frequent targets for counterfeiting networks.
Counterfeit oncology drugs can have devastating consequences because patients rely on these treatments during life-threatening conditions.
Holographic blister foils help protect oncology medicines by providing:
A highly visible authentication feature on each blister pack
Packaging elements that are extremely difficult for counterfeiters to reproduce
Compatibility with serialization and track-and-trace systems
This ensures that genuine medicines reach hospitals, pharmacies, and patients without interference from counterfeit supply chains.
Securing Anti-Infective Drugs Against Counterfeit Distribution
Anti-infective medications such as antibiotics and antivirals are widely used across healthcare systems and are frequently distributed across international markets.
Because of their global demand, these medicines are particularly vulnerable to counterfeit manufacturing and unauthorized resale.
The distribution of counterfeit anti-infective drugs contributes to serious public health risks, including ineffective treatment and antimicrobial resistance.
Holographic blister foils add a powerful security layer by making packaging authentication easier at multiple points in the supply chain.
Distributors, pharmacists, and regulatory authorities can visually confirm that the blister packaging includes genuine security features before the product reaches patients.
Enhancing Security for Psychotropic and Controlled Substances
Psychotropic medications and controlled drugs are among the most tightly regulated pharmaceutical categories.
These medicines require strict monitoring to prevent misuse, diversion, or illegal distribution.
However, counterfeit versions of these products continue to appear in illegal markets.
Holographic blister foils help pharmaceutical manufacturers strengthen packaging security by ensuring that:
Genuine products include identifiable holographic authentication elements
Counterfeit copies are easier to detect
Tampering or repackaging attempts become visible
By integrating security features directly into blister packaging materials, manufacturers create a stronger defense against both counterfeiting and product diversion.
Combining Holographic Blister Foils with Track & Trace Authentication
While holographic security provides strong visual protection, combining it with digital verification systems creates an even more powerful anti-counterfeit framework.
Modern pharmaceutical brand protection strategies often combine secure packaging technologies with Track & Trace systems.
When holographic blister foils are integrated with serialized QR codes or authentication identifiers, manufacturers gain the ability to:
Verify product authenticity instantly
Track product movement across supply chains
Detect duplicate or suspicious codes
Identify unauthorized market diversion
This hybrid approach creates both physical security and digital traceability, significantly improving pharmaceutical supply chain protection.
Why High-Risk Pharmaceutical Manufacturers Are Adopting Holographic Blister Foils
Pharmaceutical companies manufacturing high-risk medicines are increasingly prioritizing packaging security as part of their broader brand protection and compliance strategies.
Holographic blister foils offer several important advantages:
Strong visual authentication that is difficult to replicate
Integration with serialization and Track & Trace technologies
Tamper-evident packaging protection
Enhanced regulatory confidence
Improved distributor and patient trust
These benefits make holographic blister foils an effective packaging security solution for manufacturers producing high-value or life-critical medicines.
How Lasersec Technologies Supports Secure Pharmaceutical Packaging
At Lasersec Technologies, we specialize in advanced pharmaceutical anti-counterfeit packaging solutions designed to protect high-risk medicines across global markets.
Our holographic blister foil solutions integrate complex holographic security with high-quality pharmaceutical packaging materials, enabling manufacturers to strengthen packaging authentication without disrupting production processes.
These solutions are part of our broader pharmaceutical industry solutions and help companies:
Prevent counterfeit drug infiltration
Protect high-risk therapeutic categories
Strengthen supply chain security
Improve packaging authentication
Support regulatory compliance
By combining advanced holographic technologies with secure packaging design, we help pharmaceutical brands safeguard both their products and their patients.
Taking Pharmaceutical Packaging Security Forward
As counterfeiting methods grow more sophisticated, the need for advanced packaging security is no longer optional — it is a critical requirement for manufacturers of high-risk medicines. Holographic blister foils represent a proven, scalable, and highly effective solution that addresses both the physical and digital dimensions of product authentication.
At Lasersec Technologies, we remain committed to continuous innovation in anti-counterfeit pharmaceutical packaging, helping manufacturers stay ahead of emerging threats while maintaining full regulatory compliance.
Meet Us at CPhI InnoPack Pharma Confex 2026
We are excited to share thatLasersec Technologies will be participating as an Exhibit Partner at the 15th Annual CPhI InnoPack Pharma Confex — one of India’s most significant platforms for pharmaceutical packaging innovation and industry collaboration.
If you are exploring how holographic blister foils or advanced anti-counterfeit packaging solutions can strengthen your product security, this is an excellent opportunity to connect with our team directly and see our latest technologies up close.
Visit us at Booth No. F1 on 18–19 June 2026 at Sahara Star, Mumbai, and let us help you find the right packaging security solution for your therapeutic category.
Across many industries today, product safety and authenticity have become critical priorities for regulators, manufacturers, and consumers.
From pharmaceuticals and food products to cosmetics and electronics, companies are expected to ensure that their products reach customers without interference or tampering. However, global supply chains often involve multiple distributors, logistics providers, and retailers before a product reaches the end user.
This complexity creates opportunities for product tampering, repackaging, and counterfeit substitution.
To address these risks, regulators around the world increasingly require tamper-evident or tamper-proof packaging systems that clearly indicate whether a product has been opened or altered.
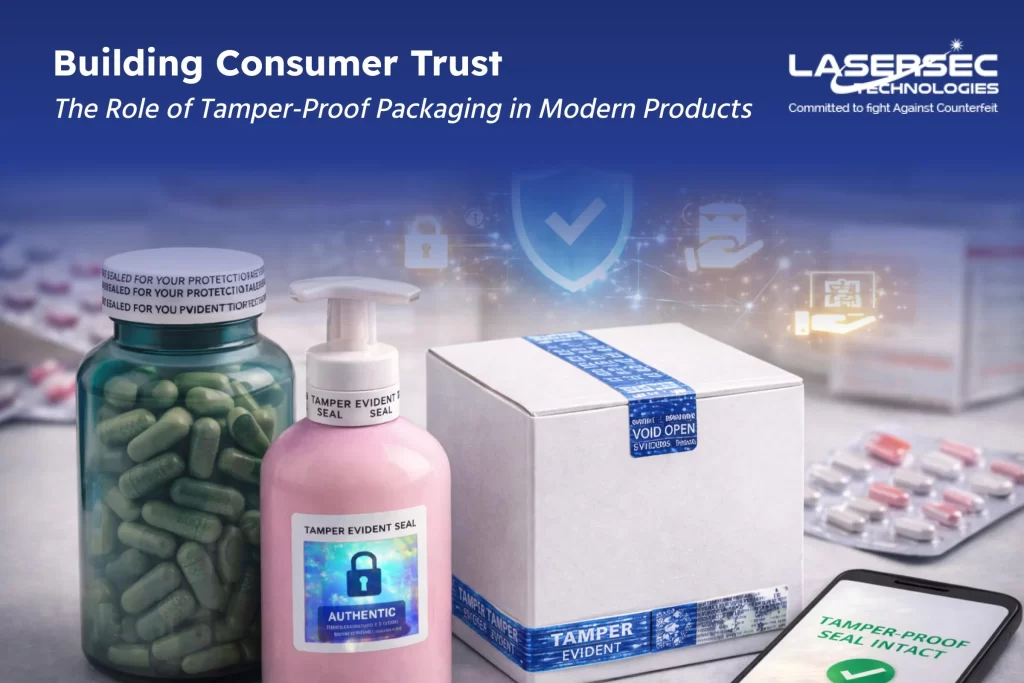
Tamper-proof packaging has therefore evolved from being a packaging enhancement to becoming a global compliance standard for product safety and brand protection using solutions like tamper proof hologram stickers and tamper-evident labels.
The Growing Importance of Tamper-Evident Packaging
Consumers today expect transparency and safety when purchasing products, especially those that affect health or personal use.
If packaging shows signs of tampering, customers immediately question the product’s safety and authenticity.
Because of this, tamper-evident packaging has become a critical requirement across many sectors.
Tamper-evident packaging solutions help ensure that:
Consumers can identify potential tampering quickly
These protections provide an important safety layer for both manufacturers and consumers.
When tampering can be easily detected, the risk of unsafe or counterfeit products reaching the market is significantly reduced.
Industries Where Tamper-Proof Packaging Is Becoming Mandatory
Regulatory authorities and industry standards organizations are increasingly encouraging or mandating tamper-evident packaging in several sectors.
Some of the most prominent industries include:
1. Pharmaceuticals
Pharmaceutical regulators worldwide require packaging systems that protect medicines from tampering and counterfeit substitution.
Tamper-evident seals, serialized packaging, and authentication labels such as pharma holographic labels help ensure that medicines reaching patients remain safe and genuine.
2. Food and Beverage
Food safety regulations often require packaging that clearly shows whether a product has been opened before purchase.
Tamper-evident caps, seals, and labels help prevent contamination and protect consumer health. Explore more in our FMCG anti-counterfeit solutions.
3. Cosmetics and Personal Care
Cosmetic brands increasingly use tamper-evident packaging to assure consumers that products have not been opened or altered before purchase.
This helps maintain product safety and brand credibility.
4. Electronics and Consumer Goods
High-value electronics and accessories are frequently targeted by counterfeiters or repackagers.
Tamper-evident labels help ensure products remain sealed and authentic throughout distribution. Learn more in our Electronics industry solutions.
How Tamper-Proof Packaging Prevents Counterfeiting and Repackaging
Tamper-proof packaging introduces visible or structural indicators that show whether a product has been opened or altered.
Unlike traditional packaging seals, tamper-evident security features cannot be removed or reapplied without leaving clear signs of interference.
Common tamper-evident packaging technologies include:
Security hologram stickers integrated into packaging using security holograms
These features make it extremely difficult for counterfeiters to open packages, replace the contents, and reseal them without detection.
As a result, tamper-proof packaging acts as a first line of defense against product tampering and counterfeit substitution.
Supporting Regulatory Compliance Through Secure Packaging
Governments and regulatory bodies are increasingly strengthening packaging requirements to improve product safety and traceability.
Many regulatory frameworks now emphasize:
Tamper-evident packaging requirements
Product authentication mechanisms
Supply chain transparency
Protection against counterfeit products
Tamper-proof packaging supports these requirements by providing a clear visual indication if a product has been interfered with.
This allows regulators, distributors, and retailers to quickly identify suspicious products during inspections.
For manufacturers exporting products across international markets, implementing tamper-evident packaging also helps demonstrate proactive compliance with global safety standards.
Strengthening Consumer Trust Through Tamper-Evident Protection
Consumer trust plays a critical role in purchasing decisions.
If customers suspect that a product has been opened, altered, or replaced, they are unlikely to use it and may avoid the brand entirely.
Tamper-evident packaging provides a simple but powerful reassurance mechanism.
When consumers see intact security seals or holographic labels such as hologram stickers, they gain confidence that the product has not been compromised.
This helps manufacturers:
Strengthen customer confidence in product safety
Reduce complaints related to product tampering
Protect brand credibility in competitive markets
Improve customer loyalty over time
Visible packaging security features also signal that the brand takes product protection seriously.
Combining Tamper-Proof Packaging with Authentication Technologies
While tamper-evident packaging prevents unauthorized opening, combining it with digital authentication technologies further strengthens product security.
For example, tamper-evident labels can be integrated with:
This combination enables both physical protection and digital verification.
Even if a product is tampered with or copied, authentication systems can help detect suspicious activity and identify counterfeit products quickly.
Together, these layers provide stronger protection across the entire product lifecycle.
How We Support Tamper-Proof Packaging and Brand Protection
At Lasersec Technologies, we provide advanced anti-counterfeit packaging solutions designed to help manufacturers implement reliable tamper-proof protection.
Our solutions integrate secure packaging features directly into product labels and packaging materials.
By combining physical tamper-evident features with authentication technologies, we help manufacturers strengthen product security across global supply chains.
Why Tamper-Proof Packaging Is Essential in Modern Global Supply Chains
As global supply chains continue to expand, the risks associated with product tampering and counterfeiting are also increasing.
Tamper-proof packaging has become a critical component of modern packaging strategies because it ensures that products reach consumers in their original, uncompromised condition.
By implementing tamper-evident security features, manufacturers can strengthen compliance with global safety standards while protecting both consumers and brand reputation.
In today’s market environment, tamper-proof packaging is no longer optional. It is an essential foundation for product safety, regulatory compliance, and long-term brand protection.
Ready-to-eat (RTE) foods have become a major part of modern consumer lifestyles.
From packaged meals and frozen foods to ready-to-cook snacks and convenience products, consumers increasingly rely on packaged food that can be consumed quickly with minimal preparation.
However, as the demand for convenience foods grows, so does the importance of ensuring packaging safety and integrity.
Unlike traditional packaged goods, ready-to-eat products are consumed directly by consumers. Any tampering with the packaging can pose immediate health risks.
For food manufacturers and FMCG brands, ensuring that packaging clearly shows any sign of interference has become a critical safety requirement.
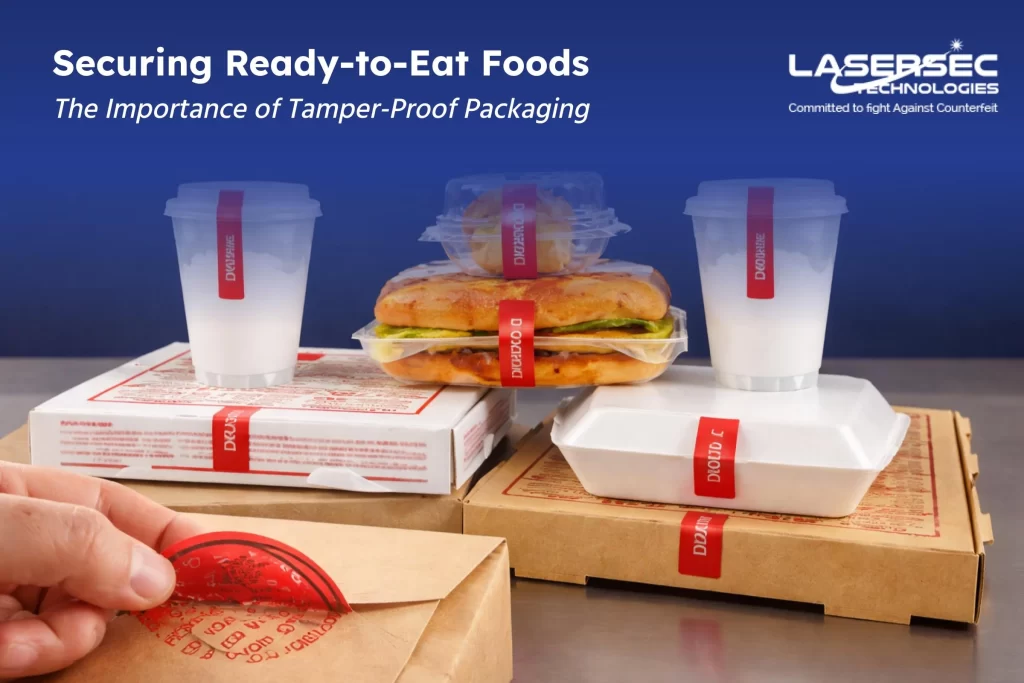
This is where tamper-proof packaging solutions such as security seals, tear bands, and tamper-evident labels play a vital role in protecting both consumers and brand reputation.
Ready-to-eat foods move through complex distribution networks before reaching consumers.
Products may pass through multiple stages including manufacturing plants, cold storage facilities, transport hubs, retail stores, and delivery services.
At each stage, the product may be handled by several intermediaries.
Without proper tamper-evident protection, it can be difficult to determine whether a food package has been opened or compromised during distribution.
Even minor tampering can create serious risks such as:
Food contamination
Product spoilage
Loss of product freshness
Consumer health hazards
Brand reputation damage
For products that are meant to be consumed immediately, packaging integrity becomes one of the most important safety indicators.
The Rising Risk of Food Tampering in Modern Supply Chains
Food tampering incidents, although rare, can have severe consequences for both consumers and brands.
In the case of ready-to-eat products, tampering may involve:
Opening packaging and resealing it
Altering or contaminating food contents
Replacing products with lower-quality alternatives
Damaging protective seals during handling
Because ready-to-eat foods often rely on sealed packaging to maintain hygiene and freshness, any compromise in packaging integrity can undermine product safety.
For FMCG companies, preventing tampering is therefore not just a packaging concern but a food safety priority.
Key Tamper-Proof Packaging Solutions for Ready-to-Eat Foods
Modern food packaging uses several mechanisms to provide clear visual evidence of tampering.
These solutions help consumers, retailers, and inspectors easily identify whether a package has been opened or altered.
Some of the most widely used tamper-evident packaging features include:
Security Seals
Security seals are applied to food packaging to ensure that the product remains unopened until it reaches the consumer.
Once broken, the seal cannot be restored to its original state.
Security seals are commonly used for:
Meal trays
Frozen food containers
Jar lids
Beverage caps
Food cartons
Tear Bands and Breakable Rings
Tear bands are thin strips integrated into packaging that must be removed before opening the product.
These bands break permanently when opened, providing immediate visual evidence that the package has been accessed.
They are frequently used in:
Frozen food containers
Bottled sauces
Packaged beverages
Sealed food jars
Tamper-Evident Labels
Tamper-evident labels provide additional protection by revealing any attempt to remove or reposition the label.
These labels may include features such as:
Destructible material that breaks when peeled
Security patterns that appear when tampered with
Adhesive residues that indicate interference
Because these labels cannot be reapplied cleanly, they help ensure packaging authenticity.
Visual Tamper Evidence: Why It Matters to Consumers
One of the most important aspects of food packaging security is visible assurance.
Consumers often rely on simple visual cues to determine whether a product is safe to consume.
If packaging appears compromised or damaged, consumers are far less likely to purchase the product.
Clear visual tamper indicators help consumers quickly confirm that:
Our solutions integrate tamper-evident labels, security seals, and authentication technologies that help ensure product safety throughout the supply chain.
These solutions help FMCG brands:
Protect ready-to-eat and frozen food packaging
Prevent unauthorized opening or resealing
Provide visible tamper evidence for consumers
Strengthen food safety compliance
Safeguard brand reputation in competitive markets
By integrating security directly into packaging, food manufacturers can maintain product integrity from production to consumption.
Injectable medicines are among the most critical products in modern healthcare.
From oncology therapies and vaccines to biologic and emergency medications, injectable drugs are used in situations where treatment accuracy and product integrity are essential.
Unlike many oral medications, injectable drugs enter the bloodstream directly. Any compromise in authenticity or quality can pose immediate risks to patient safety.
Yet despite strict pharmaceutical regulations, counterfeit injectables continue to appear in global supply chains.
In many cases, counterfeiters replicate packaging components such as vials, ampoules, and outer cartons so convincingly that visual inspection alone cannot confirm authenticity.
For manufacturers of sterile and injectable medicines, protecting packaging integrity has therefore become a critical part of product safety.
Why Injectable Medicines Are Prime Targets for Counterfeiters
Injectable drugs are often high-value therapies used in hospitals, clinics, and specialized treatment centers.
Many injectable medicines are expensive due to complex manufacturing processes, sterile production requirements, and regulatory approvals.
These factors make injectable drugs particularly attractive targets for counterfeit operations.
Common targets include:
Oncology injections
Vaccines and biologic
Emergency injectable medicines
Hormone therapies
High-value specialty injectables
Counterfeiters may attempt to replicate packaging components or refill genuine containers with non-genuine substances.
Because injectable packaging formats such as vials and ampoules are relatively small, counterfeit versions can sometimes enter distribution channels without immediate detection.
The consequences of counterfeit injectables can be severe:
Ineffective or dangerous treatments
Patient safety risks
Hospital supply chain disruptions
Regulatory investigations and recalls
Loss of trust in pharmaceutical brands
The Unique Packaging Challenges of Injectable Medicines
Injectable medicines typically use packaging formats such as:
Glass vials
Ampoules
Pre-filled syringes
Sterile containers
These packaging types must maintain strict sterility and product stability.
However, their small size and simple structure can also make them vulnerable to tampering or counterfeit replication if additional security features are not integrated.
For example:
Vials may be refilled with counterfeit substances
Ampoules may be replicated using similar glass formats
Labels can be copied or replaced
Outer cartons may be duplicated
Because injectable products are frequently handled in clinical environments, ensuring secure and verifiable packaging is essential.
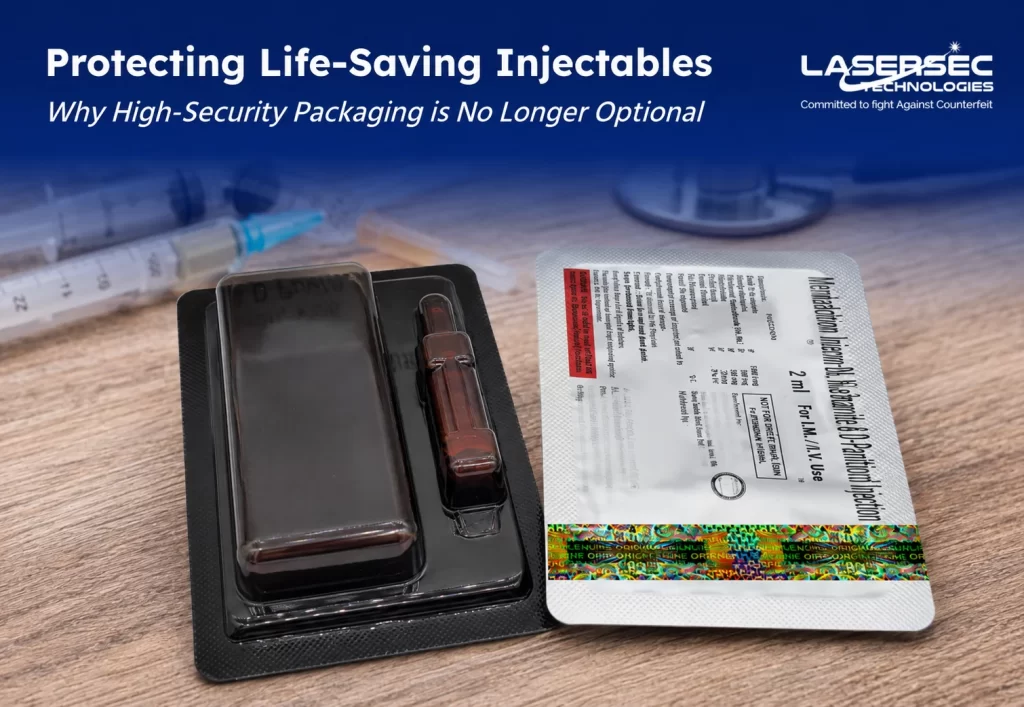
The Role of Tamper-Evident Labels in Injectable Packaging
Tamper-evident labeling is one of the most important protective mechanisms for injectable medicines.
These labels are designed to clearly reveal if a vial, ampoule, or outer packaging has been opened or altered.
Provide visible authentication for distributors and healthcare providers
Deter counterfeit packaging replication
Enhance brand identification on sterile packaging
Because holographic features require specialized manufacturing capabilities, they are extremely difficult for counterfeiters to reproduce accurately.
Securing Vials and Ampoules with High-Security Labeling
High-security labels can be applied directly to injectable packaging components such as:
Glass vials
Ampoule containers
Injection cartons
Sterile packaging seals
These labels serve multiple purposes.
They provide tamper evidence, authenticate the product visually, and help protect the packaging from unauthorized opening or substitution.
When applied strategically, security labels ensure that any attempt to alter the packaging becomes immediately visible.
This strengthens product integrity across distribution channels.
Integrating Serialization and Digital Verification
In addition to physical packaging security, many pharmaceutical manufacturers are implementing serialization and digital authentication systems.
Serialized identification codes allow each product unit to carry a unique digital identity.
These codes may be integrated through:
Data matrix codes
Serialized QR codes
Unique product identifiers linked to authentication platforms
When scanned, the system can verify whether the product matches its registered identity within a secure database.
If duplicate codes appear or if products are detected in unauthorized locations, the system can immediately flag potential counterfeit activity.
Improving Supply Chain Security for Injectable Drugs
Injectable medicines typically move through tightly controlled pharmaceutical supply chains that include manufacturers, distributors, hospitals, and pharmacies.
Despite these controls, supply chain vulnerabilities can still occur.
High-security packaging helps strengthen supply chain protection by enabling:
Immediate detection of tampering
Easier authentication for distributors and regulators
Better traceability through serialization systems
Faster identification of suspicious products
This visibility helps pharmaceutical companies prevent counterfeit injectables from reaching healthcare environments.
Why Injectable Drug Manufacturers Are Adopting High-Security Packaging
Manufacturers of sterile pharmaceutical products are increasingly recognizing that packaging security is directly connected to patient safety and regulatory compliance.
High-security packaging provides several advantages:
Stronger regulatory confidence and brand protection
For life-saving injectable medicines, these protections are becoming essential rather than optional.
How Lasersec Technologies Supports Secure Injectable Packaging
At Lasersec Technologies, we develop advanced anti-counterfeit packaging and labeling solutions designed to protect high-risk pharmaceutical products.
Our high-security solutions combine tamper-evident labeling, holographic authentication technologies, and serialization-ready packaging features to secure injectable medicines throughout the supply chain.
These solutions help pharmaceutical manufacturers:
Protect injectable drugs from counterfeiting
Secure vials and ampoules against tampering
Strengthen packaging authentication
Support regulatory compliance and serialization
Improve supply chain transparency
By integrating advanced security technologies directly into pharmaceutical packaging, we help ensure that life-saving medicines reach healthcare providers and patients safely.