Lasersec Technologies

Counterfeit, Pharma, Pharma Industry, Fake, Duplicate, Medicine, India, Drugs, Drug, Indian Market

Drug counterfeiting is a growing problem in India. As people become more aware of the need to take medication, but can’t afford their prescribed drugs, more consumers are turning to alternative sources. The result? A thriving black market for cheap drugs, as well as a growing number of dangerous and fake drugs finding their way into the legitimate supply chain.

India is the third largest pharmaceutical market in the world. Counterfeit and substandard drugs are big business in India, and the country is fast becoming a major source for pharma counterfeiting, at a time when the world is grappling with drug-resistant superbugs.

How Drug counterfeiting is rising in India?

The Indian market is full of counterfeit products, due to the lack of regulation. This makes it easy for fake sellers to access the market and distribute their products through conventional channels. The long and complicated supply chains are full of loopholes which allow counterfeiters to operate with ease. With more sophisticated techniques being used by counterfeiters, it is becoming increasingly difficult for customers to identify fake products.

With drug shortages and high demands during a pandemic, fake drugs are being sold more due to a lack of awareness and proper surveillance. 

To combat this problem, multiple stakeholders such as India’s Drugs Controller General (DCGI), state drug control authorities, and pharma industry are working  together. In India, when a complaint about a drug is raised, samples are seized and sent for quality testing by regulatory authorities.

What is the impact of the substandard medicines?

Substandard medicines are manufactured, packed, or distributed that do not conform to the official standards of quality. These medicines can be ineffective, dangerous or cause health problems. The most common causes of substandard medicines are counterfeits, expired drugs and poor quality controls. 

Poor-quality medicines may cause treatment failure, disease worsening, decreased quality of life, and even death and the consequences of poorly manufactured drugs reach beyond India’s borders so it is crucial that medicine manufacturers create standards to ensure the quality of their products. The healthcare industry needs to provide greater awareness about counterfeiting in order to preserve access to safe, effective treatments worldwide.

How can the industry combat the counterfeiting menace?

India began to adopt anti-counterfeit technologies. These technologies are being used to prevent counterfeiting, catch criminals, and help consumers identify genuine products. There’s a need for manufacturers and distributors to plug gaps in the supply chain and use mechanisms which verify drug quality. Stronger regulations can govern product discrepancies, weed out counterfeiters, and protect public health and the economy.

One of the biggest things that brands can do to help combat counterfeiting in India by using secure and safe packaging which cannot be replicated by any fake manufacturers. 

Our company recently introduced a new product as “BLISTER FOIL with Security Printing” and “VOID & TAMPER PROOF LABELS,” which adds an extra layer of protection to the products and their packaging.

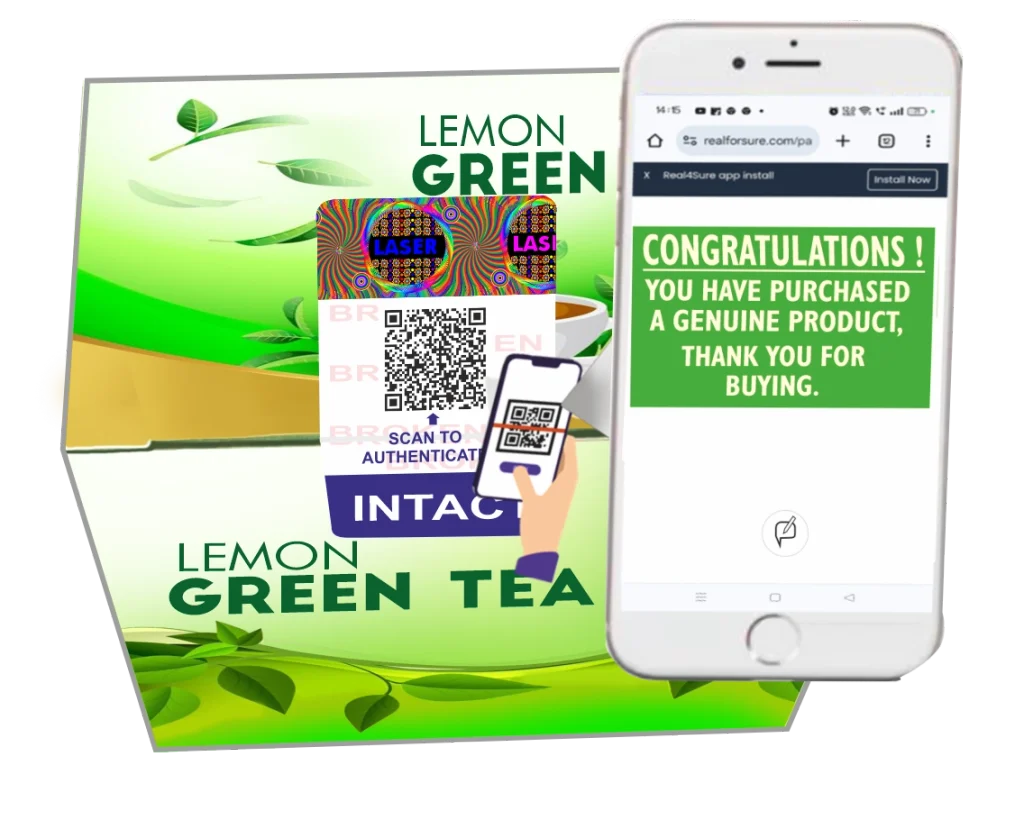
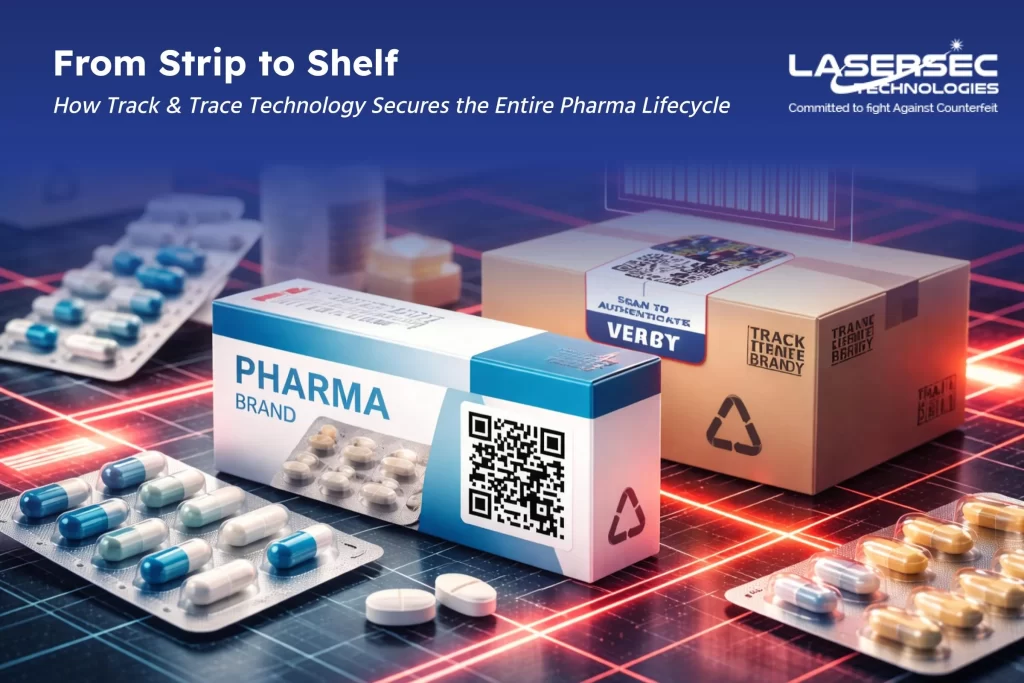
Another is “PHYGITAL“, a lethal combination of PHYsical and diGITAL that fights drug falsification with 100% accuracy using this innovative technology. The physical form is enhanced with the most secure yet tamper-evident labels, as well as a QR code for digital security.

About Lasersec Technologies

One of the leading and most trusted manufacturers and innovators of Anti-Counterfeiting products that provides practical solutions by constantly identifying any requirement from different aspects of the industry. 

Lasersec Technologies develop and customize products based on the requirements of a specific industry. Sustained Research and Development by a qualified team of professionals supported by well-equipped facilities, and keeping abreast of the latest technology and pioneering new products and applications.

Contact us at mktg@lasersec.in  or reach out on +91 –11-45637955 
Share :

Frequently Asked Questions

Related Blogs

Tamper-evident packaging and secure seals protecting pharmaceutical and consumer products for brand protection

Across many industries today, product safety and authenticity have become critical priorities for regulators, manufacturers, and consumers.

From pharmaceuticals and food products to cosmetics and electronics, companies are expected to ensure that their products reach customers without interference or tampering. However, global supply chains often involve multiple distributors, logistics providers, and retailers before a product reaches the end user.

This complexity creates opportunities for product tampering, repackaging, and counterfeit substitution.

To address these risks, regulators around the world increasingly require tamper-evident or tamper-proof packaging systems that clearly indicate whether a product has been opened or altered.

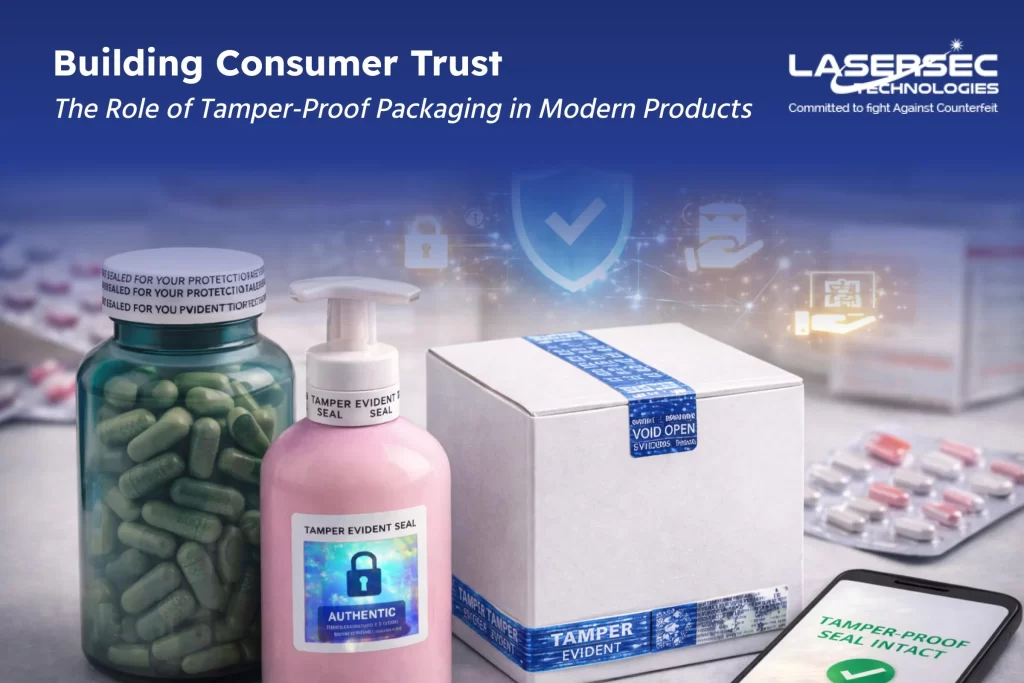
Tamper-proof packaging has therefore evolved from being a packaging enhancement to becoming a global compliance standard for product safety and brand protection using solutions like tamper proof hologram stickers and tamper-evident labels.

The Growing Importance of Tamper-Evident Packaging

Consumers today expect transparency and safety when purchasing products, especially those that affect health or personal use.

If packaging shows signs of tampering, customers immediately question the product’s safety and authenticity.

Because of this, tamper-evident packaging has become a critical requirement across many sectors.

Tamper-evident packaging solutions help ensure that:

  • Products cannot be opened without visible damage
  • Unauthorized repackaging becomes difficult
  • Counterfeiters cannot easily reuse genuine packaging
  • Consumers can identify potential tampering quickly

These protections provide an important safety layer for both manufacturers and consumers.

When tampering can be easily detected, the risk of unsafe or counterfeit products reaching the market is significantly reduced.

Industries Where Tamper-Proof Packaging Is Becoming Mandatory

Regulatory authorities and industry standards organizations are increasingly encouraging or mandating tamper-evident packaging in several sectors.

Some of the most prominent industries include:

1. Pharmaceuticals

Pharmaceutical regulators worldwide require packaging systems that protect medicines from tampering and counterfeit substitution.

Tamper-evident seals, serialized packaging, and authentication labels such as pharma holographic labels help ensure that medicines reaching patients remain safe and genuine.

2. Food and Beverage

Food safety regulations often require packaging that clearly shows whether a product has been opened before purchase.

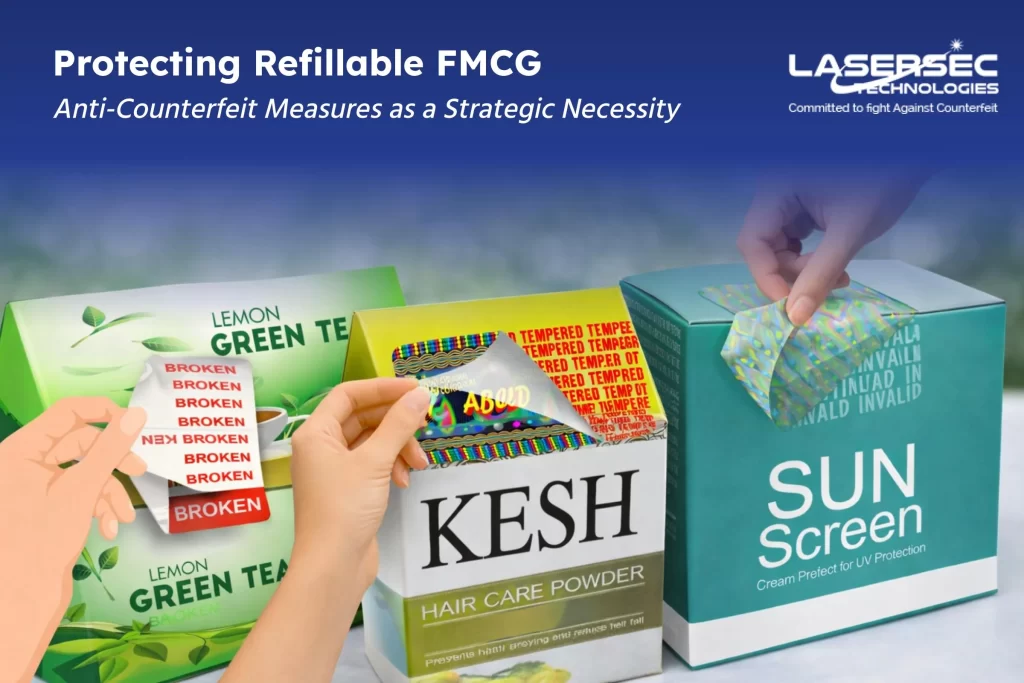
Tamper-evident caps, seals, and labels help prevent contamination and protect consumer health. Explore more in our FMCG anti-counterfeit solutions.

3. Cosmetics and Personal Care

Cosmetic brands increasingly use tamper-evident packaging to assure consumers that products have not been opened or altered before purchase.

This helps maintain product safety and brand credibility.

4. Electronics and Consumer Goods

High-value electronics and accessories are frequently targeted by counterfeiters or repackagers.

Tamper-evident labels help ensure products remain sealed and authentic throughout distribution. Learn more in our Electronics industry solutions.

How Tamper-Proof Packaging Prevents Counterfeiting and Repackaging

Tamper-proof packaging introduces visible or structural indicators that show whether a product has been opened or altered.

Unlike traditional packaging seals, tamper-evident security features cannot be removed or reapplied without leaving clear signs of interference.

Common tamper-evident packaging technologies include:

These features make it extremely difficult for counterfeiters to open packages, replace the contents, and reseal them without detection.

As a result, tamper-proof packaging acts as a first line of defense against product tampering and counterfeit substitution.

Supporting Regulatory Compliance Through Secure Packaging

Governments and regulatory bodies are increasingly strengthening packaging requirements to improve product safety and traceability.

Many regulatory frameworks now emphasize:

  • Tamper-evident packaging requirements
  • Product authentication mechanisms
  • Supply chain transparency
  • Protection against counterfeit products

Tamper-proof packaging supports these requirements by providing a clear visual indication if a product has been interfered with.

This allows regulators, distributors, and retailers to quickly identify suspicious products during inspections.

For manufacturers exporting products across international markets, implementing tamper-evident packaging also helps demonstrate proactive compliance with global safety standards.

Strengthening Consumer Trust Through Tamper-Evident Protection

Consumer trust plays a critical role in purchasing decisions.

If customers suspect that a product has been opened, altered, or replaced, they are unlikely to use it and may avoid the brand entirely.

Tamper-evident packaging provides a simple but powerful reassurance mechanism.

When consumers see intact security seals or holographic labels such as hologram stickers, they gain confidence that the product has not been compromised.

This helps manufacturers:

  • Strengthen customer confidence in product safety
  • Reduce complaints related to product tampering
  • Protect brand credibility in competitive markets
  • Improve customer loyalty over time

Visible packaging security features also signal that the brand takes product protection seriously.

Combining Tamper-Proof Packaging with Authentication Technologies

While tamper-evident packaging prevents unauthorized opening, combining it with digital authentication technologies further strengthens product security.

For example, tamper-evident labels can be integrated with:

This combination enables both physical protection and digital verification.

Even if a product is tampered with or copied, authentication systems can help detect suspicious activity and identify counterfeit products quickly.

Together, these layers provide stronger protection across the entire product lifecycle.

How We Support Tamper-Proof Packaging and Brand Protection

At Lasersec Technologies, we provide advanced anti-counterfeit packaging solutions designed to help manufacturers implement reliable tamper-proof protection.

Our solutions integrate secure packaging features directly into product labels and packaging materials.

These include:

By combining physical tamper-evident features with authentication technologies, we help manufacturers strengthen product security across global supply chains.

To explore more solutions, visit our Product Gallery.

Why Tamper-Proof Packaging Is Essential in Modern Global Supply Chains

As global supply chains continue to expand, the risks associated with product tampering and counterfeiting are also increasing.

Tamper-proof packaging has become a critical component of modern packaging strategies because it ensures that products reach consumers in their original, uncompromised condition.

By implementing tamper-evident security features, manufacturers can strengthen compliance with global safety standards while protecting both consumers and brand reputation.

In today’s market environment, tamper-proof packaging is no longer optional. It is an essential foundation for product safety, regulatory compliance, and long-term brand protection.

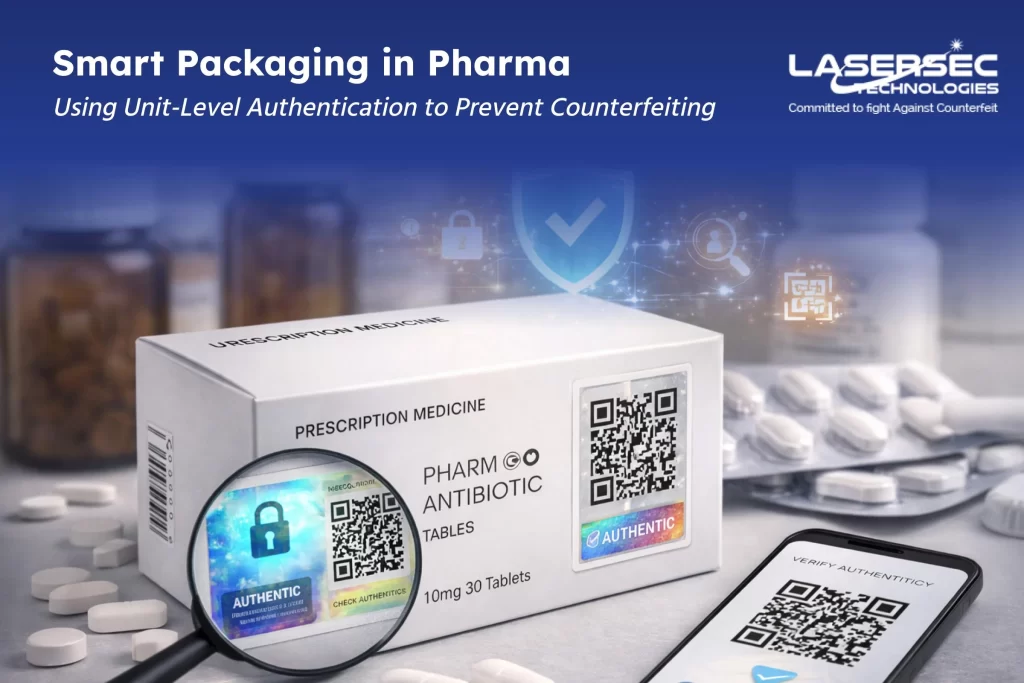
Pharmaceutical packaging security has become a critical concern for drug manufacturers worldwide. Unit-level authentication is now the smartest way to protect every package across the supply chain.

At each stage, verifying the authenticity of the medicine becomes essential.

In many markets, counterfeit drugs and unauthorized repackaging continue to challenge pharmaceutical supply chains. Packaging may appear genuine, yet without reliable authentication systems, it can be difficult to confirm whether the medicine is authentic.

This is why pharmaceutical companies are increasingly implementing unit-level authentication systems.

Unit-level authentication assigns a unique identity to every individual product unit, allowing manufacturers, regulators, and pharmacies to verify authenticity instantly through secure authentication technologies such as QR code authentication and Track & Trace systems.

By enabling verification at the smallest packaging level, pharmaceutical companies can significantly reduce the risk of counterfeit medicines entering the market.

The Growing Risks of Counterfeit and Repacked Medicines

Pharmaceutical products move through complex supply chains before reaching patients. These supply chains often involve multiple intermediaries such as distributors, wholesalers, and retailers.

This complexity creates opportunities for unauthorized activities, including counterfeit drug circulation and repackaging of genuine medicines.

Some common risks include:

  • Counterfeit medicines replicating genuine packaging using security hologram stickers
  • Unauthorized repackaging of original medicines
  • Reuse of genuine packaging for fake products
  • Diversion of products into unintended markets
  • Difficulty verifying authenticity at pharmacy level

These activities not only affect pharmaceutical companies but also create serious risks for patient safety.

Consequences can include:

  • Reduced trust in pharmaceutical brands
  • Regulatory compliance issues
  • Distribution channel conflicts
  • Potential health risks for patients

Without reliable authentication systems, detecting these issues early becomes extremely difficult.

What Is Unit-Level Authentication in Pharmaceutical Packaging

Unit-level authentication means assigning a unique, traceable identity to every individual medicine package.

Instead of identifying products only by batch numbers or carton-level codes, each unit receives its own authentication marker.

This is typically implemented using technologies such as:

Each identifier is connected to secure manufacturing and distribution data.

When the code is scanned, the system can instantly verify:

  • Whether the product is genuine
  • The manufacturing origin
  • Batch and production information
  • Whether the code has been duplicated

This enables reliable product verification throughout the supply chain.

How Unit-Level Authentication Prevents Fake Repackaging

One of the most common challenges in pharmaceutical markets is fake repackaging.

In this scenario, counterfeiters reuse genuine packaging materials or create look-alike packaging to insert counterfeit medicines.

Without authentication, these fake products may appear legitimate.

Unit-level authentication prevents this by ensuring that each product unit has a unique identity supported by technologies like QR code holograms.

If a counterfeiter attempts to copy or reuse a code, the authentication system can detect:

  • Duplicate code scans
  • Invalid product records
  • Suspicious verification locations

This allows manufacturers and regulators to quickly identify counterfeit activity and take corrective action. By making every package individually verifiable, unit-level authentication significantly reduces the risk of fake repackaging.

Preventing Product Diversion with Unit-Level Verification

Product diversion occurs when genuine medicines are redirected from their intended distribution markets into unauthorized regions.

This can disrupt pricing structures, violate distribution agreements, and create regulatory complications.

Unit-level authentication helps detect diversion by linking each product unit to specific manufacturing and distribution data through systems like Track & Trace technology.

When the product is scanned, the system can verify:

  • The intended market for the product
  • Whether it appears in an unexpected location
  • Whether the product has already been verified elsewhere

If the product is detected outside its authorized distribution channel, the system can immediately flag the activity. This visibility allows pharmaceutical companies to investigate unauthorized distribution and maintain better control over global supply chains.

Strengthening Pharmaceutical Compliance and Traceability

Many regulatory frameworks now require pharmaceutical manufacturers to implement serialization and traceability systems. Authorities expect companies to demonstrate the ability to verify product authenticity and track medicines across the supply chain.

Unit-level authentication supports these regulatory goals by enabling:

  • Individual product serialization
  • End-to-end supply chain traceability
  • Authentication verification at distribution points
  • Faster investigation of suspicious products

These capabilities help regulators confirm product legitimacy during inspections and market surveillance.For pharmaceutical companies operating in global markets, unit-level authentication also strengthens compliance with evolving regulatory standards using solutions such as Track & Trace systems.

Improving Patient Trust Through Product Verification

Patients rely on medicines to protect their health, which makes trust essential in the pharmaceutical industry. However, patients often cannot visually distinguish between genuine and counterfeit medicines if packaging looks similar.

Unit-level authentication enables pharmacies and even patients to verify medicines quickly using smartphone-based authentication tools. By scanning a secure QR code or authentication marker such as QR code authentication labels, users can confirm whether the product is genuine.

This level of transparency helps:

  • Improve patient confidence in medicines
  • Reduce circulation of counterfeit drugs
  • Strengthen trust in pharmaceutical brands
  • Support safer healthcare outcomes

How We Support Unit-Level Authentication in Pharmaceutical Packaging

At Lasersec Technologies, we provide advanced anti-counterfeit packaging solutions designed to help pharmaceutical manufacturers implement reliable unit-level authentication systems.

Our solutions integrate secure packaging technologies with digital authentication platforms using:

By embedding these technologies directly into pharmaceutical packaging, we help manufacturers create secure authentication systems that protect medicines across the entire supply chain. To explore more, visit our Pharma Solutions.

Why Unit-Level Authentication Is Essential for Modern Pharmaceutical Packaging

Pharmaceutical supply chains are becoming increasingly complex, and the risks associated with counterfeit medicines continue to grow. Unit-level authentication provides a powerful solution by enabling every medicine package to be individually verified.

This approach helps pharmaceutical companies detect counterfeit activity, prevent product diversion, and maintain greater visibility across their supply chains. Most importantly, it helps ensure that genuine medicines reach pharmacies and patients safely. In today’s pharmaceutical industry, unit-level authentication is no longer optional.  It is a critical foundation for protecting product integrity, regulatory compliance, and patient trust.